Vehicle-mounted material handling conveyors are specialized automated transport systems designed to move goods and materials within industrial or manufacturing settings. These systems are typically integrated onto vehicles or mobile platforms, enabling seamless material transfer from one location to another. Understanding the core components and design principles of such conveyors is crucial for industries aiming to optimize their material flow processes and enhance operational efficiency.
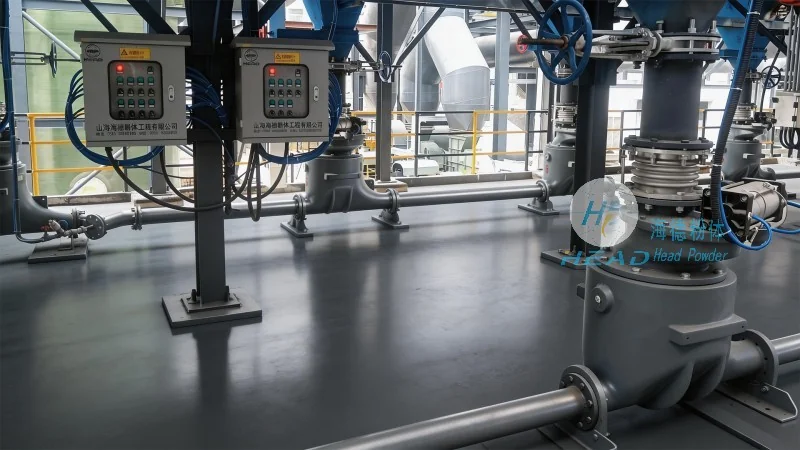
The functionality of a vehicle-mounted conveyor system relies on several critical components that work in concert to ensure smooth operation. The primary elements include a conveyor belt or roller system, which serves as the transport medium, and a drive mechanism—often an electric motor or hydraulic system—that propels the material along the path. Additionally, these systems incorporate sensors and control units to monitor and adjust the movement of items, ensuring accuracy and safety. The structural frame of the conveyor, typically constructed from robust materials like steel or aluminum, supports the entire system and is engineered to withstand the rigors of industrial use. Many vehicle-mounted conveyors also feature adjustable features, such as height or angle adjustments, to accommodate different loading and unloading scenarios, enhancing their versatility.
The design of vehicle-mounted material handling conveyors is guided by principles that prioritize efficiency, reliability, and adaptability. Engineers focus on creating systems that can handle a wide range of materials, from lightweight parts to heavier components, while maintaining consistent speed and direction. The conveyor's layout is carefully planned to minimize the distance between pickup and drop-off points, reducing overall transit time and improving throughput. Furthermore, the integration of automation technologies, such as programmable logic controllers (PLCs) and real-time monitoring systems, enhances operational control and allows for dynamic adjustments based on changing production demands. Safety features, including emergency stop buttons, collision detection sensors, and protective guards, are integral to the design, ensuring that operators and the surrounding environment remain protected during operation.
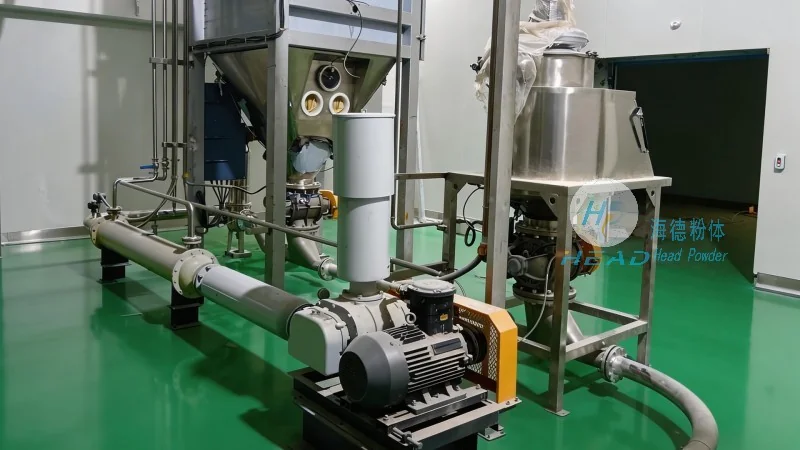
Vehicle-mounted material handling conveyors find widespread application across various industries, including automotive manufacturing, logistics, and warehousing. In automotive plants, these systems are commonly used to transport car parts and components between assembly lines, streamlining the production process and reducing manual labor. In logistics and distribution centers, they facilitate the movement of packages and goods between storage areas and loading docks, improving order fulfillment rates and reducing delivery times. The flexibility of vehicle-mounted conveyors also makes them suitable for use in construction sites, where they can transport building materials to different work zones as needed. By adapting to diverse operational requirements, these systems contribute to increased productivity and operational efficiency across multiple sectors.
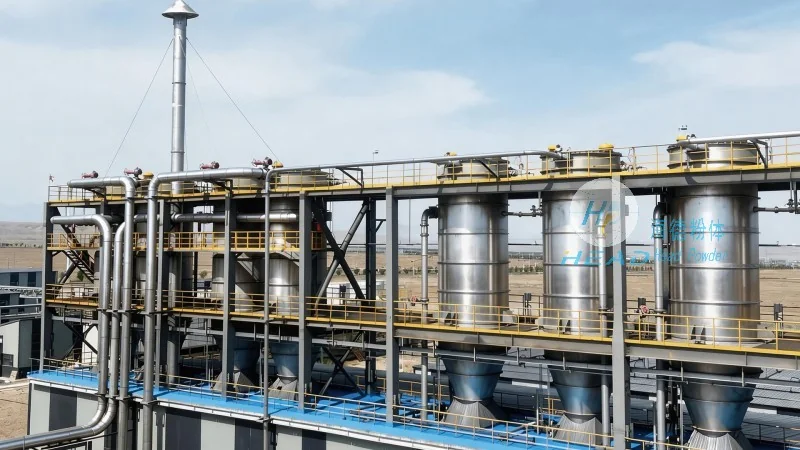
Implementing vehicle-mounted material handling conveyors offers several advantages that can significantly impact a business's bottom line. One of the key benefits is the reduction in labor costs, as automated systems can handle tasks that were previously performed manually, freeing up human resources for more complex or value-added activities. Additionally, these conveyors enhance operational speed and accuracy, minimizing errors and delays in material transport. The ability to integrate with existing production lines and systems further streamlines workflows, leading to improved overall efficiency. Furthermore, the durability and reliability of well-designed vehicle-mounted conveyors result in lower maintenance costs and longer service life, providing a strong return on investment for businesses.
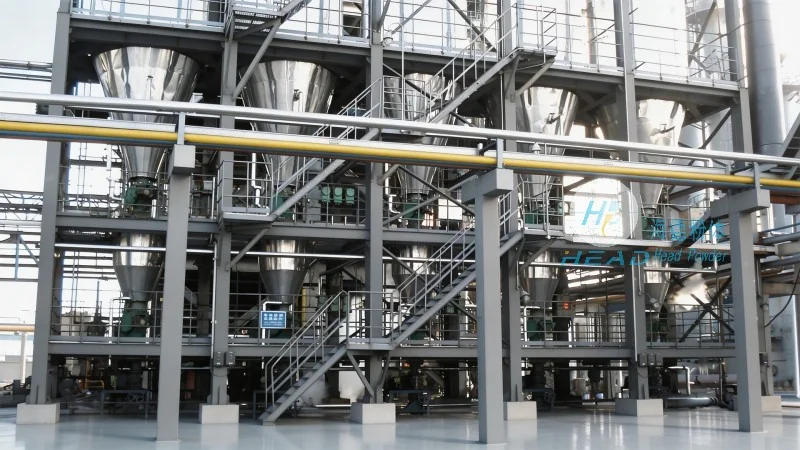
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in the design and production of vehicle-mounted material handling conveyors. The company's commitment to quality and innovation ensures that their products are tailored to meet the specific needs of each client. With a focus on customization, HeadPowder engineers work closely with customers to develop conveyor systems that integrate seamlessly with existing infrastructure and operational processes. This approach ensures that the new system complements rather than disrupts current workflows, minimizing downtime during implementation. The company's expertise in material handling technology allows them to offer solutions that address unique challenges, such as handling fragile items or transporting heavy loads in confined spaces. By providing comprehensive support from design to installation, HeadPowder helps businesses achieve their material handling goals effectively and efficiently.
Vehicle-mounted material handling conveyors represent a vital component of modern industrial automation, offering businesses a reliable and efficient solution for material transport. As industries continue to evolve and demand higher productivity, the importance of such systems will only grow. The design principles and technological advancements in these conveyors will continue to improve, enabling even greater adaptability and performance. For businesses looking to enhance their material flow processes, investing in a well-designed vehicle-mounted conveyor system is a strategic decision that can lead to long-term operational benefits. With companies like Shandong HeadPowder Engineering Co., Ltd. leading the way in innovation, the future of material handling technology looks promising, with continued advancements that will further optimize industrial operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top