For power plants and industrial facilities dealing with fly ash, the efficient handling and storage of this material are critical to operational efficiency and environmental compliance. A key component in this process is the fly ash silo material handling system, which ensures the safe and reliable transport of fly ash from collection points to storage or processing areas. This article explores the fundamentals of such systems, focusing on their design principles and the engineering solutions provided by Shandong HeadPowder Engineering Co., Ltd.
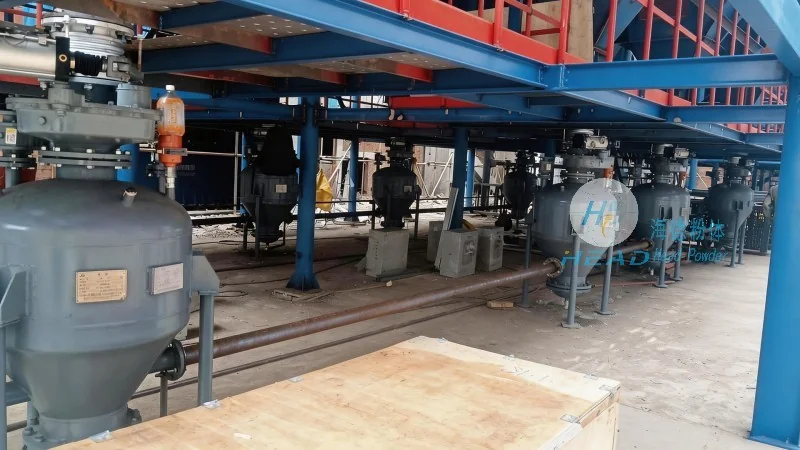
Fly ash, a byproduct of coal combustion in thermal power plants, is a fine, powdery material that requires specialized handling due to its characteristics like high moisture content, dustiness, and potential for agglomeration. Traditional methods of handling fly ash, such as manual shoveling or simple conveyor systems, are often inefficient and pose health and safety risks. The fly ash silo material handling system addresses these challenges by integrating advanced engineering to manage the material flow, minimize dust emissions, and ensure consistent performance. At the core of this system is the fly ash silo, which serves as a storage vessel, and the associated equipment that facilitates the movement of ash from the silo to downstream processes or disposal sites.
As a leading provider of engineering solutions for material handling and storage, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing systems tailored to the unique needs of industrial applications. With a strong commitment to quality and innovation, the company has established itself as a trusted partner in the power and environmental sectors. HeadPowder’s expertise lies in understanding the complexities of fly ash handling, from the physical properties of the material to the operational requirements of power plants. The company’s team of engineers and technicians work closely with clients to develop customized solutions that enhance efficiency, reduce costs, and ensure compliance with environmental regulations. HeadPowder’s facilities are located in Shandong, China, where the company leverages local resources and expertise to deliver high-quality products and services.
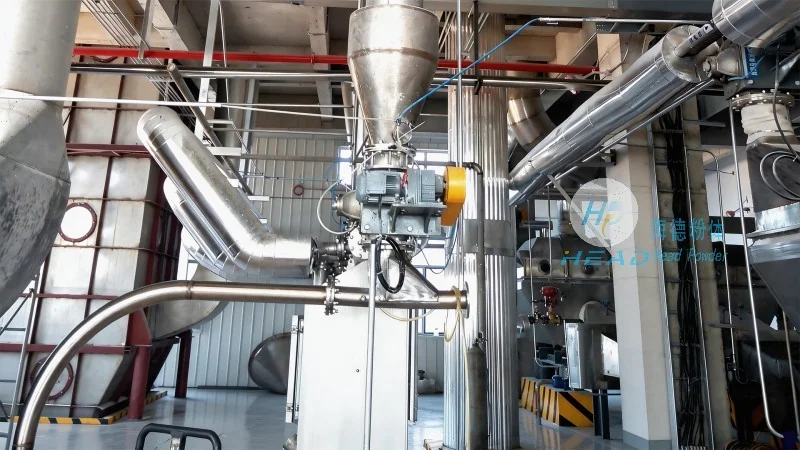
The design of a fly ash silo material handling system is a complex process that involves balancing several key factors to achieve optimal performance. The primary design principles include material flow optimization, dust control, structural integrity, and operational reliability. Material flow optimization is crucial to prevent blockages and ensure consistent ash movement from the silo to the discharge point. This is achieved through the use of specialized conveyor systems, such as screw conveyors or pneumatic transport lines, which are designed to handle the specific characteristics of fly ash. Dust control is another critical aspect, as fly ash is a fine powder that can easily become airborne, posing health risks and environmental concerns. The system incorporates dust suppression measures, including sealed conveyor systems, air filtration units, and moisture control mechanisms, to minimize dust emissions and maintain a safe working environment. Structural integrity is essential to withstand the weight of the stored material and the forces generated during material movement. The silo and supporting structures are designed to meet or exceed industry standards for load-bearing capacity and durability. Operational reliability is ensured through the integration of sensors, monitoring systems, and automated controls that allow for real-time tracking of material levels, flow rates, and system performance. These controls help prevent downtime and ensure that the system operates efficiently around the clock.
A typical fly ash silo material handling system consists of several interconnected components, each playing a vital role in the overall operation. The main components include the fly ash silo, inlet and outlet conveyors, dust collection systems, and control panels. The fly ash silo is a large, cylindrical or rectangular vessel designed to store large quantities of fly ash. It is typically made of steel or concrete, with a smooth interior surface to prevent ash buildup and facilitate easy discharge. The inlet conveyor receives ash from the boiler or collection hopper and transports it to the top of the silo. This conveyor may be a screw conveyor or a belt conveyor, depending on the system design. The outlet conveyor, located at the bottom of the silo, removes ash from the storage vessel and directs it to the next stage of processing or disposal. The dust collection system is integrated into the conveyor lines to capture and filter airborne particles, preventing dust from escaping into the environment. This system typically includes cyclones, baghouses, or electrostatic precipitators, depending on the required efficiency and regulatory standards. The control panel houses the system’s sensors, controls, and monitoring equipment, allowing operators to track and manage the system’s performance. This panel may include indicators for material levels, flow rates, and alarm systems for any abnormalities, such as blockages or excessive dust emissions.
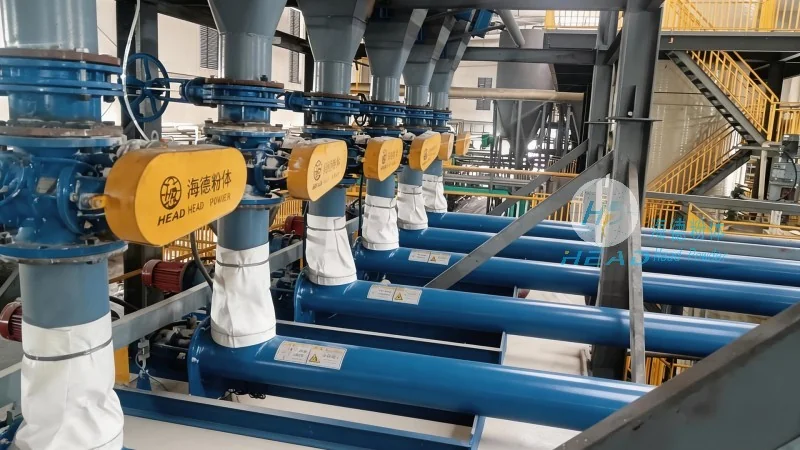
Implementing a comprehensive fly ash silo material handling system offers numerous advantages for industrial facilities. One of the primary benefits is improved operational efficiency, as the system automates the handling process, reducing the need for manual intervention and minimizing downtime. This leads to increased production capacity and reduced labor costs. The system also enhances safety by minimizing exposure to fly ash dust, which can cause respiratory issues and other health problems. By controlling dust emissions, the system helps facilities comply with environmental regulations and maintain a clean working environment. Additionally, the system’s design allows for scalability, enabling facilities to expand their capacity as their needs grow. The integration of monitoring and control systems provides real-time data on system performance, allowing for proactive maintenance and troubleshooting, which further reduces operational costs and extends the lifespan of the equipment. Overall, a well-designed fly ash silo material handling system is a critical investment for facilities seeking to optimize their fly ash management processes and achieve long-term operational success.
In conclusion, the fly ash silo material handling system is a vital component in the efficient and safe management of fly ash from power plants and industrial facilities. Its design principles, which focus on material flow optimization, dust control, structural integrity, and operational reliability, ensure that the system meets the demanding requirements of modern industrial applications. Shandong HeadPowder Engineering Co., Ltd. plays a key role in providing these advanced systems, leveraging its expertise and commitment to quality to deliver solutions that enhance efficiency, safety, and compliance. By investing in a well-designed material handling system, facilities can improve their operational performance, reduce costs, and contribute to a more sustainable environment. The future of fly ash management lies in such integrated systems, and companies like HeadPowder are at the forefront of developing the technology and expertise needed to meet these challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top