A positive pressure pneumatic powder conveying system is a specialized industrial equipment designed to transport bulk powders or granular materials over long distances with high efficiency and minimal product degradation. This technology utilizes compressed air or other gases to create a positive pressure environment, ensuring the material is conveyed from the source to the destination without the need for mechanical components that might cause contamination or damage to the product. The system is widely used in various industries, including pharmaceuticals, food processing, chemicals, and minerals, where maintaining product integrity and controlling dust are critical.
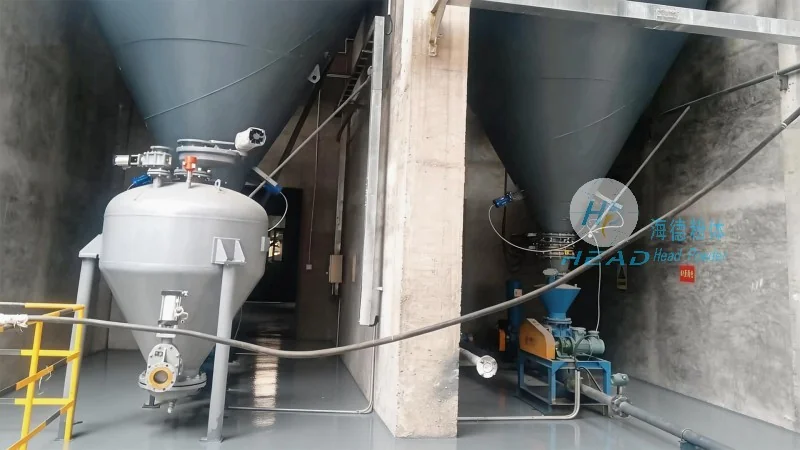
The core components of a positive pressure system include the air compressor, air treatment units, conveying lines, and material feeders. The air compressor generates the necessary pressure to move the material through the system. Air treatment units, such as filters and dryers, ensure the air is clean and dry, preventing moisture or contaminants from affecting the powder quality. Conveying lines, typically made of stainless steel or other corrosion-resistant materials, are designed to withstand the pressure and maintain product purity. Material feeders, such as rotary valves or star feeders, control the flow rate of the powder into the system, ensuring consistent and reliable operation.
The design of a positive pressure system is based on the principle of maintaining a higher pressure in the conveying line compared to the ambient environment. This pressure differential forces the powder to move through the system. The material is typically fed into the conveying line at a controlled rate, and the compressed air then propels the powder particles forward. The system operates continuously, with the air and powder mixture traveling through the lines until it reaches the discharge point. At the destination, the air is separated from the powder, often using cyclone separators or bag filters, allowing the powder to be collected while the air is recycled back to the compressor.
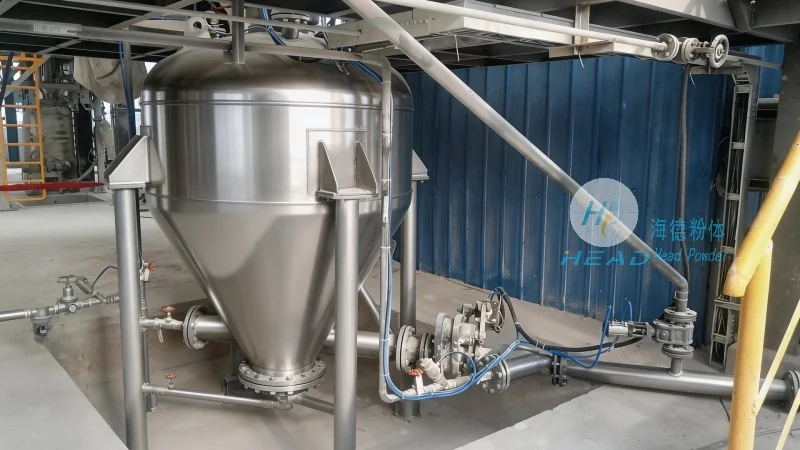
One of the primary advantages of positive pressure systems is their ability to handle a wide range of powder properties, including fine powders, sticky materials, and those prone to caking. The positive pressure environment prevents the material from settling or clogging the lines, ensuring smooth and continuous operation. Additionally, these systems are highly effective in controlling dust, as the entire system is sealed and the air is filtered before being released. This makes them ideal for applications where dust control is mandatory, such as in pharmaceutical and food industries. Another benefit is the ability to convey materials over long distances with minimal pressure drop, making them suitable for large-scale production facilities.
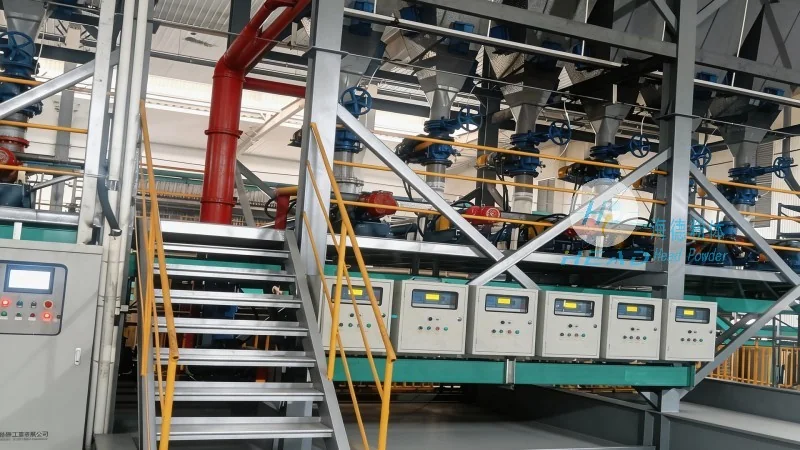
Positive pressure pneumatic powder conveying systems are used in numerous industries where bulk material handling is essential. In the pharmaceutical industry, they are used to transport active pharmaceutical ingredients (APIs) and excipients with strict purity requirements. In food processing, they handle ingredients like flour, sugar, and spices, ensuring they remain free from contamination. The chemical industry utilizes these systems for transporting raw materials and finished products, such as powders used in coatings or pigments. In the minerals and mining sector, they are used to transport ores and other bulk materials from processing plants to storage or shipping facilities. The versatility of positive pressure systems makes them a preferred choice for industries that demand high standards of product quality and operational efficiency.
Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China, specializes in designing and manufacturing customized positive pressure powder conveying systems tailored to meet the specific needs of clients. The company’s engineers work closely with customers to understand their material characteristics, conveying requirements, and operational constraints, ensuring the final system is optimized for performance and reliability. Customization options include different line materials, pressure ratings, and control systems, allowing the system to integrate seamlessly with existing production lines. The company also provides comprehensive support, including installation, commissioning, and maintenance services, ensuring the system operates at peak efficiency throughout its lifecycle.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top