For industrial applications that require the handling of fine powders, especially those used in pharmaceutical, food, or chemical industries where purity and contamination control are critical, a specialized system is often employed. This system, commonly known as a purified powder material conveying system, is designed to transport dry powders with minimal risk of cross-contamination and to maintain the integrity of the material being moved. The design principles behind such systems are rooted in ensuring efficiency, safety, and compliance with industry standards. These systems are essential for processes where even trace amounts of contamination can compromise product quality or safety, making the design and operation of the system a critical aspect of industrial operations.
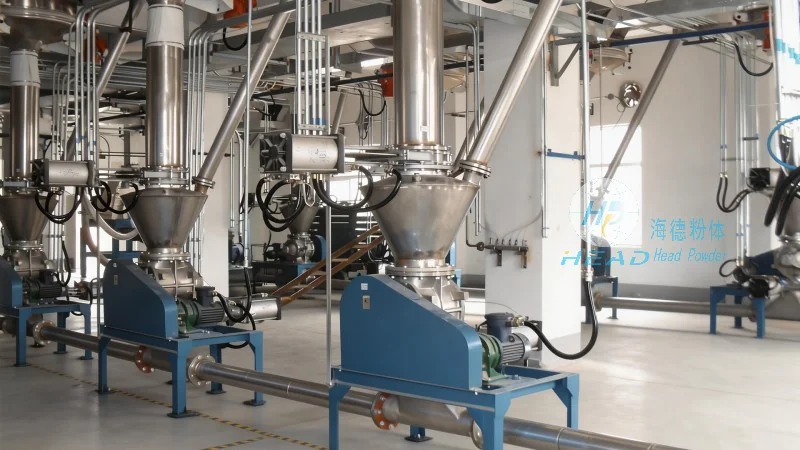
The core components of a purified powder material conveying system typically include a hopper for material storage, a feeding mechanism to control the flow of powder, a conveying pipeline (often made of stainless steel or other inert materials to prevent contamination), and a dust collection or filtration system. The hopper is usually equipped with a lid to prevent airborne contamination and may include a level indicator to monitor the material volume. The feeding mechanism, such as a rotary valve or a screw feeder, regulates the flow rate to match the conveying system's capacity. The pipeline is designed with smooth, non-porous surfaces to avoid powder buildup and to facilitate easy cleaning. Additionally, the system may incorporate a vacuum or pressure system to move the powder through the pipeline, depending on the specific application requirements. The hopper's design also includes a discharge valve that can be controlled remotely to ensure safe and efficient material release. The feeding mechanism is often equipped with a material sensor to detect any blockages or changes in flow, triggering an alarm or automatic shutdown to prevent system damage. The pipeline may feature a series of bends and elbows with minimal pressure loss, ensuring that the powder moves smoothly and without excessive energy consumption.
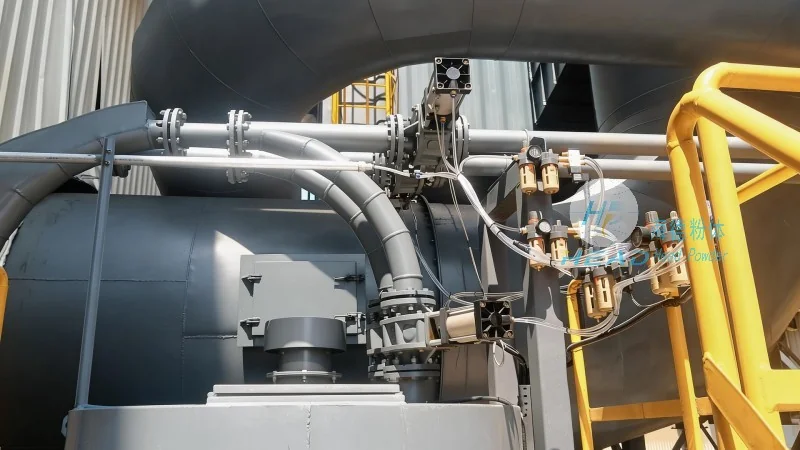
A primary design principle of a purified powder conveying system is the prevention of cross-contamination. This is achieved through several measures: the use of sealed components to avoid exposure to the environment, the incorporation of positive pressure or vacuum systems to maintain a controlled environment, and the implementation of filtration at the inlet and outlet points. The materials used in the construction of the system, such as stainless steel or PTFE-coated components, are chosen for their inertness and resistance to chemical attack. The system is also designed to minimize dead zones where powder can accumulate and become a source of contamination. Regular cleaning protocols are integrated into the design to ensure that any residual material can be easily removed, maintaining the system's sanitary condition. The filtration system, often including HEPA filters, removes airborne particles and ensures that the environment within the system remains clean. The sealed design prevents external contaminants from entering the system and internal contaminants from escaping, creating a closed-loop environment that is critical for maintaining product purity.
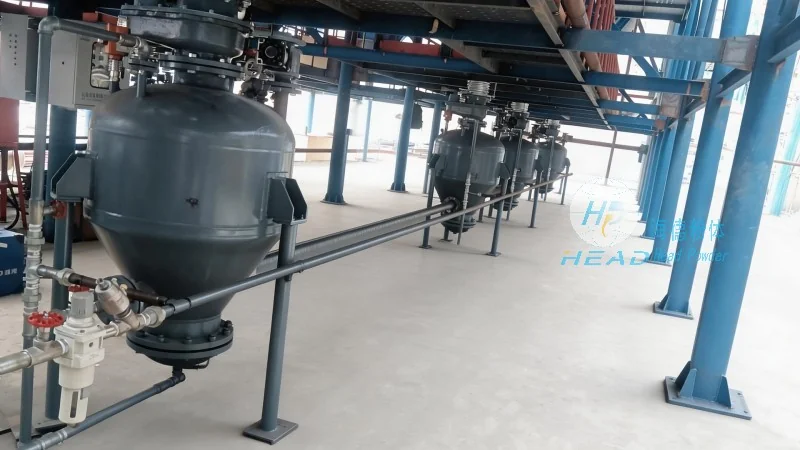
Efficiency in material transport is another critical design principle. The system is engineered to handle varying powder characteristics, such as particle size, density, and moisture content, without clogging or loss of material. The feeding mechanism is calibrated to provide a consistent flow rate, which is essential for maintaining the system's performance and preventing pressure drops that could lead to system failure. The pipeline design, including the use of appropriate bends and elbows, minimizes resistance to flow, ensuring that the powder moves smoothly and without excessive energy consumption. The control system, often integrated with sensors, monitors the flow rate and pressure, allowing for real-time adjustments to maintain optimal operation. This ensures that the system operates efficiently while meeting the required throughput and maintaining the quality of the conveyed material. Energy-efficient motors and variable speed drives are commonly used to reduce power consumption and lower operational costs. The system's design also considers the need for maintenance, with easy access to components for inspection and repair, minimizing downtime and ensuring long-term reliability.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top