Wheat handling and transportation is a critical process in the agricultural and food processing industries. Efficient and reliable methods are essential to ensure the quality and integrity of the grain from the field to the storage or processing facilities. Pneumatic conveying technology has emerged as a key solution for moving wheat and other bulk materials with precision and minimal loss. This article explores the role of pneumatic conveying systems in wheat transportation, highlighting their benefits, applications, and the expertise of Shandong HeadPowder Engineering Co., Ltd. in providing tailored solutions for this industry.
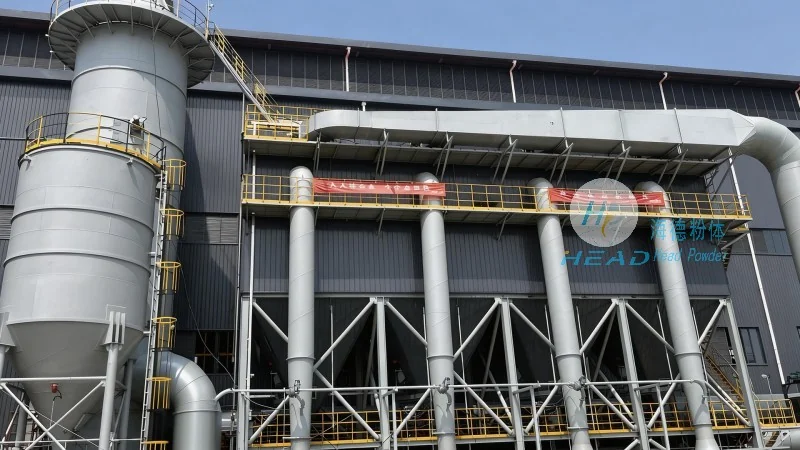
Pneumatic conveying uses air to transport bulk materials like wheat through a pipeline system. This method offers several advantages over traditional mechanical conveying, such as reduced product damage, lower maintenance costs, and the ability to handle a wide range of particle sizes and moisture contents. The system typically consists of a hopper, a blower or compressor, a pipeline network, and a discharge point. As air is forced through the pipeline, it lifts and moves the wheat particles, ensuring a smooth and continuous flow. This technology is particularly effective for long-distance or complex routing requirements, making it ideal for large-scale wheat handling operations.
Implementing pneumatic conveying systems in wheat transportation brings numerous benefits that enhance operational efficiency and product quality. One of the primary advantages is the reduction in product breakage and dust generation. Unlike mechanical conveyors that may cause abrasion or impact, pneumatic systems use air to gently move the grain, preserving its integrity and reducing the risk of contamination. Additionally, these systems are highly flexible, allowing for easy integration with existing infrastructure and the ability to reconfigure routes as needed. This adaptability is crucial for facilities that need to handle varying volumes or adjust their workflow based on seasonal demands. Another significant benefit is the energy efficiency of pneumatic conveying, especially when using high-efficiency blowers and optimized pipeline designs. By minimizing energy consumption, companies can reduce operational costs while maintaining optimal performance.
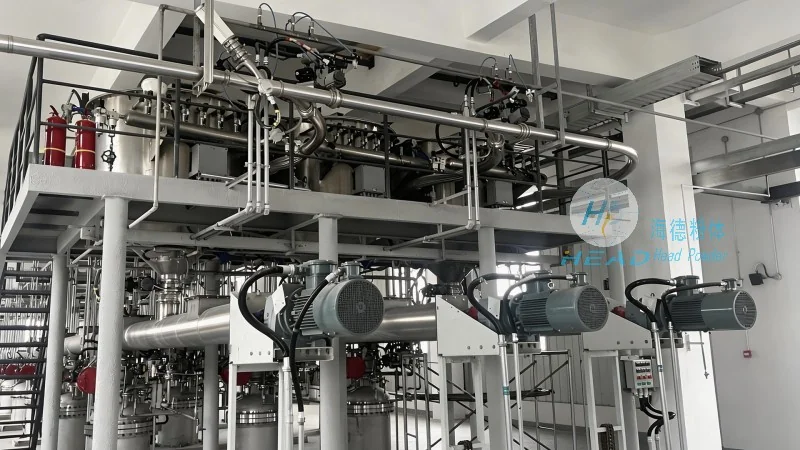
Pneumatic conveying systems are widely used in various stages of wheat handling and processing. From the initial collection and storage to the final milling or packaging, these systems play a vital role in ensuring a seamless flow of materials. In storage facilities, pneumatic conveyors can efficiently transfer wheat from silos or bins to processing lines, reducing the need for manual handling and improving safety. During processing, such as cleaning or sorting, pneumatic systems can transport wheat through screening or grading equipment, allowing for precise separation of impurities. The flexibility of these systems also makes them suitable for transporting wheat to different locations within a facility, such as from a cleaning station to a milling machine or from a storage silo to a loading dock. This versatility enables manufacturers to streamline their operations and improve overall productivity.
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveying systems tailored to the specific needs of wheat transportation and processing. With years of experience in the industry, the company understands the unique challenges faced by wheat handlers, such as varying grain characteristics, space constraints, and operational requirements. By leveraging advanced engineering and material science, HeadPowder provides customized solutions that maximize efficiency and reliability. The company’s team of experts works closely with clients to assess their current processes, identify areas for improvement, and develop a comprehensive system design. Whether it's a new installation or an upgrade to an existing facility, HeadPowder ensures that the pneumatic conveying system meets the highest standards of performance and durability. The company’s commitment to quality is evident in its use of premium materials, rigorous testing protocols, and comprehensive after-sales support. This approach has earned HeadPowder a reputation as a trusted partner in the agricultural and food processing sectors, with a focus on delivering solutions that enhance productivity and protect product quality.
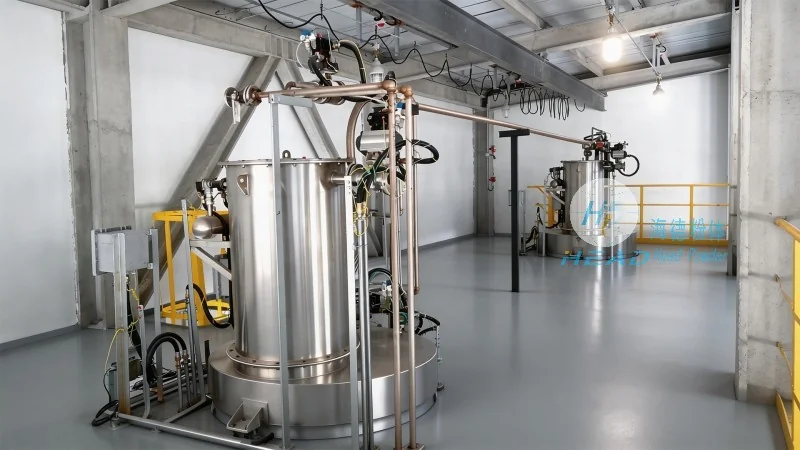
Proper installation and regular maintenance are crucial for the long-term performance and reliability of pneumatic conveying systems used in wheat transportation. When installing a new system, it is essential to consider factors such as the layout of the facility, the distance and elevation changes, and the type of wheat being handled. A well-designed system will minimize pressure losses and ensure consistent air flow, which is critical for maintaining the efficiency of the conveying process. Regular maintenance, including cleaning of the pipeline, checking blower performance, and inspecting for leaks or blockages, is necessary to prevent system downtime and ensure optimal operation. Shandong HeadPowder Engineering Co., Ltd. offers comprehensive maintenance services to help clients keep their systems in top condition. The company’s technicians are trained to handle various types of pneumatic conveying equipment and can provide timely repairs and upgrades as needed. By following the manufacturer's guidelines and scheduling regular maintenance, wheat handlers can extend the lifespan of their systems and avoid costly breakdowns.
Pneumatic conveying systems are an indispensable technology in modern wheat transportation, offering a reliable and efficient method for handling bulk materials. The benefits of reduced product damage, flexibility, and energy efficiency make these systems a preferred choice for many agricultural and food processing companies. With the expertise of Shandong HeadPowder Engineering Co., Ltd., clients can access tailored solutions that meet their specific requirements, ensuring optimal performance and product quality. As the demand for efficient wheat handling continues to grow, pneumatic conveying technology will remain a key component in the industry's success. By investing in high-quality pneumatic conveying systems and proper maintenance, wheat handlers can enhance their operational efficiency, reduce costs, and maintain the integrity of their grain, ultimately contributing to the overall sustainability of the agricultural sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top