For industries involved in the processing and distribution of mung beans, efficient and reliable material handling is crucial to maintaining product quality and operational efficiency. Among the various technologies available, pneumatic conveying stands out as a sophisticated solution tailored to the unique characteristics of mung beans. This article explores the pivotal role of pneumatic conveying systems in the transportation of mung beans, highlighting the technical advantages, operational benefits, and practical applications that make it an indispensable choice for modern agricultural and food processing enterprises.
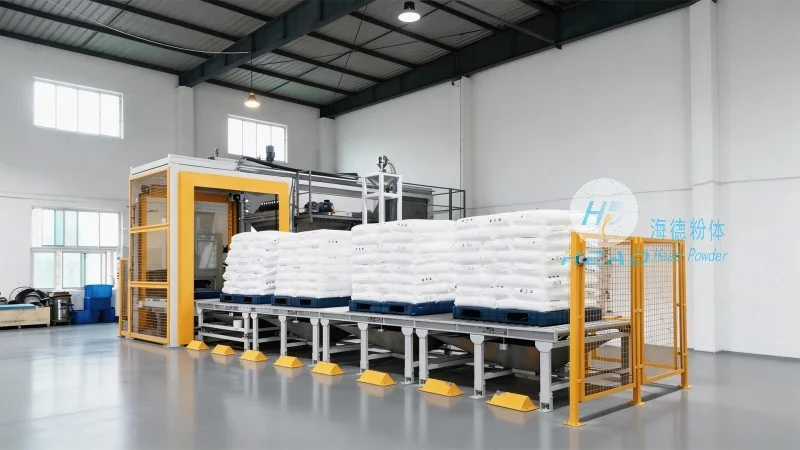
Pneumatic conveying is a method of transporting bulk materials, such as mung beans, through a pipeline using a stream of air. Unlike traditional mechanical systems like belt conveyors or screw conveyors, pneumatic conveying offers a closed system that minimizes exposure to external contaminants and environmental factors. The core components of a typical pneumatic conveying system include a hopper for material storage, a conveyor line (often equipped with a rotary valve or feeder to control flow), a blower or air compressor to generate the air stream, and a receiver or discharge point where the material is collected.
When applied to mung beans, pneumatic conveying systems deliver several critical advantages that enhance both the quality and efficiency of the handling process. First, the closed pipeline design ensures that the mung beans remain protected from dust, moisture, and microbial contamination, which is essential for maintaining their nutritional value and shelf life. This is particularly important for mung beans, as they are sensitive to humidity and can easily spoil if exposed to adverse conditions.
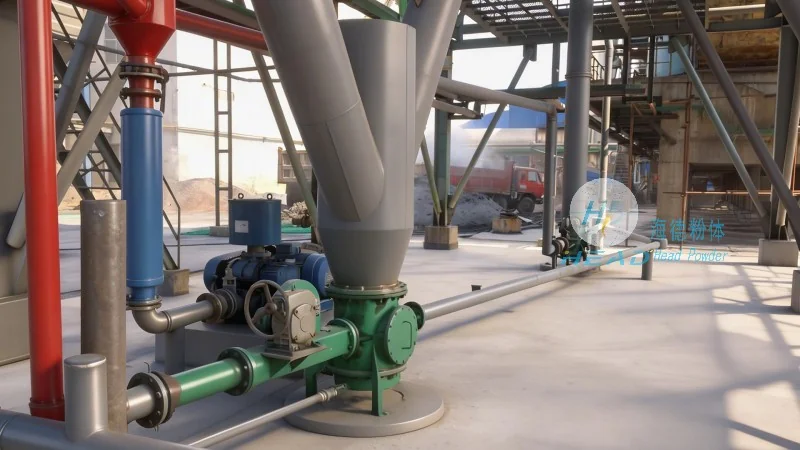
Second, pneumatic conveying offers high throughput rates with minimal operational downtime. The system can handle large volumes of mung beans at once, reducing the time required for material transfer between processing stages. This efficiency is further enhanced by the ability to integrate multiple conveying lines, allowing for flexible routing and distribution of the beans to different storage or processing facilities.
Third, the technology minimizes product degradation and loss. Unlike mechanical conveyors that may cause abrasion or breakage to the beans, pneumatic systems use air pressure to gently move the material, preserving the physical integrity of the mung beans. This is vital for maintaining their market value, especially when dealing with high-quality or specialty varieties.
The effectiveness of pneumatic conveying in mung bean transportation depends on several operational factors that must be carefully considered. One of the primary considerations is the particle size and moisture content of the mung beans. Smaller, more uniform particles are generally easier to convey, while high moisture content can lead to clogging or increased air consumption. To address these challenges, companies like Shandong HeadPowder Engineering Co., Ltd. offer customized solutions tailored to specific material characteristics.
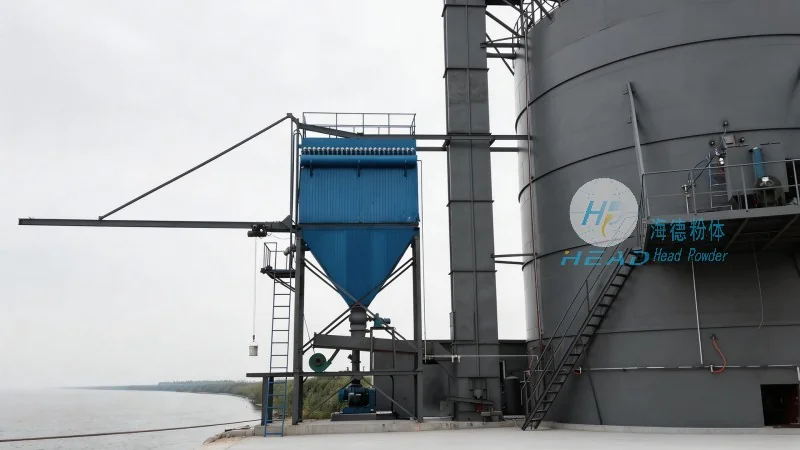
Shandong HeadPowder Engineering Co., Ltd., a leading provider of pneumatic conveying systems, specializes in designing and manufacturing equipment that meets the unique demands of mung bean processing. With headquarters in Shandong, China, the company leverages decades of industry experience to develop systems that optimize performance, energy efficiency, and durability. Their solutions often include advanced control systems that monitor air pressure, flow rates, and material levels in real-time, ensuring consistent and reliable operation.
Pneumatic conveying is not just a standalone transport solution but an integral part of the overall mung bean processing workflow. It can be seamlessly integrated with other equipment such as cleaning machines, grading systems, and packaging lines. For example, after mung beans are cleaned and sorted, the pneumatic system can efficiently transport them to the packaging stage, reducing the need for manual handling and minimizing the risk of cross-contamination.
This integration enhances overall operational efficiency by creating a streamlined, automated process. The closed system also facilitates compliance with food safety regulations, as it prevents the introduction of foreign materials and maintains a controlled environment throughout the handling process.
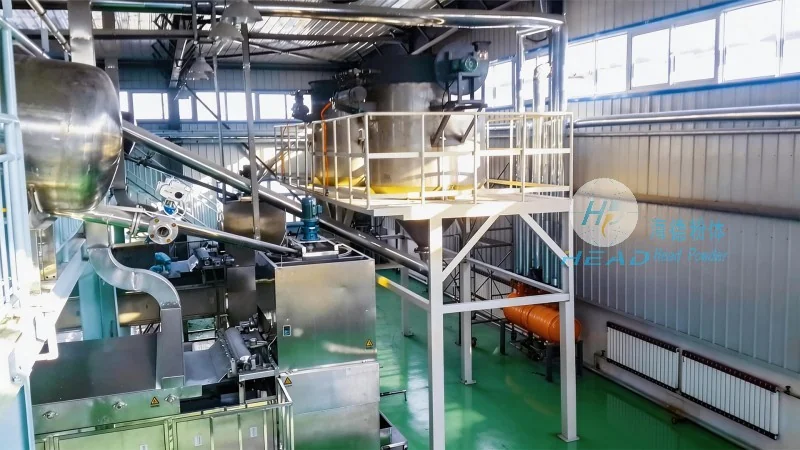
In conclusion, pneumatic conveying plays a pivotal role in the efficient and safe transportation of mung beans. By leveraging the principles of air-based material movement, these systems offer superior protection of product quality, high operational efficiency, and minimal degradation. For businesses in the mung bean industry, investing in a well-designed pneumatic conveying system is a strategic decision that can lead to improved productivity, reduced costs, and enhanced product value.
Companies like Shandong HeadPowder Engineering Co., Ltd. continue to advance the technology with innovative designs and customized solutions, ensuring that the industry can meet the growing demands for high-quality mung beans while maintaining operational excellence. As the backbone of modern mung bean handling, pneumatic conveying systems remain a cornerstone of efficient material management in the agricultural and food processing sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top