Camellia seed, also known as tea oil seed, is a key raw material in the production of edible oil and other value-added products. Efficient and reliable transportation of these seeds from storage to processing facilities is crucial for maintaining production efficiency and product quality. Pneumatic conveying systems offer a solution to this challenge by utilizing air flow to move bulk powders and granular materials like camellia seeds with high efficiency and minimal loss. Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer of pneumatic conveying equipment based in Shandong, China, specializes in providing customized solutions for such applications.
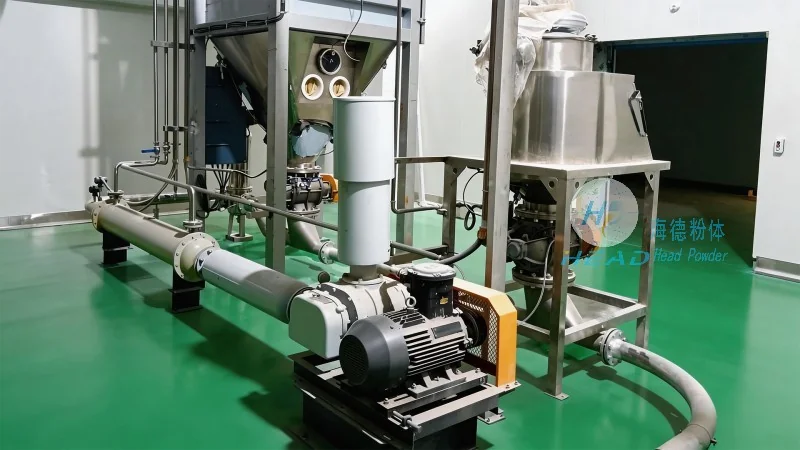
Pneumatic conveying is a technology that uses compressed air or other gas to transport solid materials through a pipeline. This method is particularly suitable for handling fine powders and seeds due to its ability to minimize material degradation, prevent contamination, and maintain a clean and hygienic environment. Unlike mechanical conveying systems, which rely on belts, buckets, or screws, pneumatic systems use air pressure to move materials, reducing the risk of product breakage and contamination.
A typical pneumatic conveying system for camellia seeds consists of several key components. These include a hopper or feeder to store and meter the seeds, a blower or compressor to generate the air flow, a pipeline network to transport the seeds, and a receiver or silo to collect the material at the destination. The system may also include accessories such as filters, cyclones, and valves to control the flow and ensure proper operation.
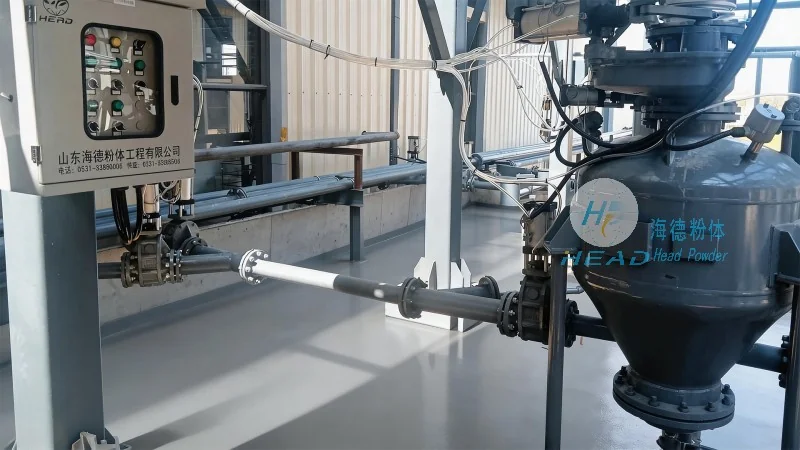
The process begins with the camellia seeds being fed into the hopper. The feeder then meters the material into the pipeline at a controlled rate. Simultaneously, the blower generates a high-pressure air stream that moves through the pipeline. As the air flows, it entrains the seeds, creating a mixture of air and solids. This mixture travels through the pipeline to the receiving silo, where the air is separated from the seeds using a cyclone or filter. The purified air is then discharged, while the seeds are collected in the silo for further processing.
Implementing a pneumatic conveying system for camellia seeds offers several advantages. First, it provides a clean and hygienic method of transport, which is essential for food processing applications. The enclosed system prevents contamination from dust, moisture, or other external factors, ensuring the quality of the seeds remains intact. Second, pneumatic conveying reduces material degradation by minimizing impact and friction during transport. This is particularly important for delicate seeds that can be easily damaged by mechanical handling. Third, the system offers high efficiency and flexibility, allowing for the transport of materials over long distances and varying elevations without the need for multiple transfer points.
In camellia seed processing facilities, pneumatic conveying is commonly used to move seeds from storage silos to oil extraction machines or other processing equipment. The system can handle large volumes of seeds with minimal labor, reducing operational costs and increasing production throughput. For example, a facility processing 100 tons of camellia seeds per day can use a pneumatic conveying system to transport the seeds from the storage area to the extraction line efficiently and without interruption.
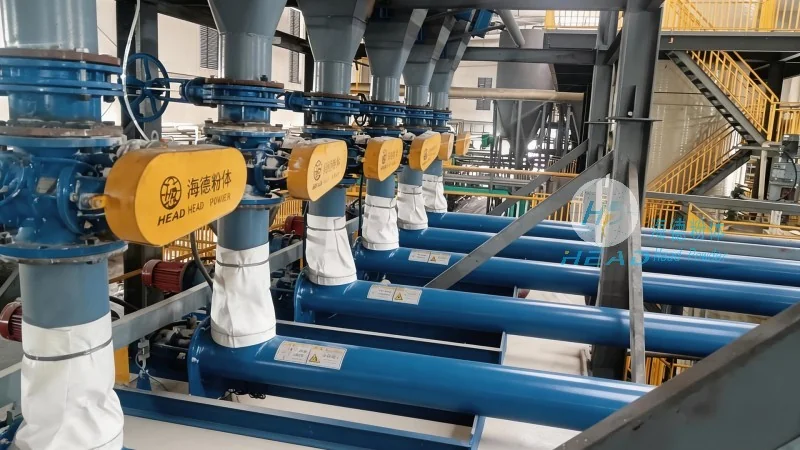
When designing a pneumatic conveying system for camellia seeds, several factors must be considered to ensure optimal performance. The system's capacity and pressure requirements must be matched to the processing needs of the facility. The pipeline diameter and length must be appropriately sized to prevent excessive pressure drop and maintain the air flow velocity necessary for effective material transport. Additionally, the material of construction for the hopper, feeder, and pipeline must be selected to resist corrosion and wear from the seeds and the air flow. Proper maintenance, including regular cleaning of filters and cyclones, is also essential to maintain system efficiency and prevent downtime.
Pneumatic conveying is a highly effective method for efficiently transporting camellia seeds in food processing applications. By utilizing air flow to move bulk powders, this technology offers advantages such as cleanliness, minimal material degradation, and high efficiency. For businesses in the camellia seed industry, investing in a well-designed pneumatic conveying system can improve production efficiency, maintain product quality, and reduce operational costs. With proper design and maintenance, pneumatic conveying systems provide a reliable and long-lasting solution for the transportation of camellia seeds from storage to processing facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top