Chocolate pneumatic conveying systems are essential equipment in the confectionery industry, designed to efficiently transport chocolate powders and other related materials. These systems utilize air pressure to move products, offering a hygienic and efficient solution for chocolate processing. The following article provides a comprehensive overview of these systems, including their working principles, key components, and practical applications.
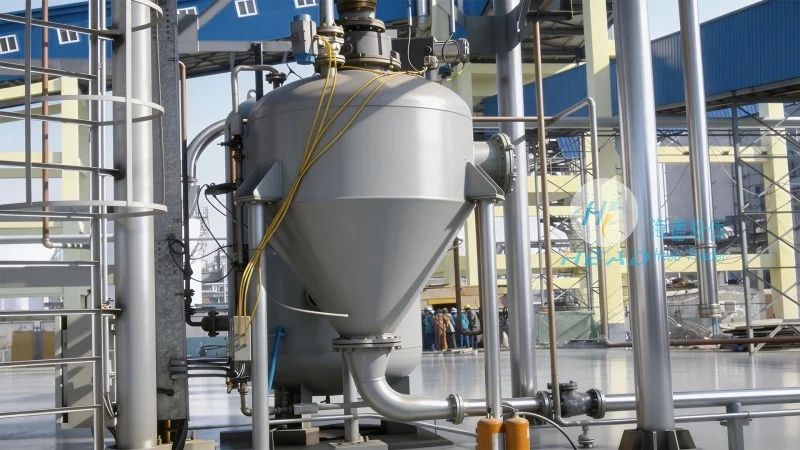
Chocolate pneumatic conveying systems are specialized equipment used to transport chocolate powders and related materials within a production facility. Unlike traditional mechanical conveyors, these systems employ air pressure to move materials, reducing the risk of contamination and ensuring a clean, efficient process. The technology is widely adopted in chocolate manufacturing due to its ability to handle delicate materials like cocoa powder and chocolate chips without causing degradation or damage.
The core components of a chocolate pneumatic conveying system include the hopper, air compressor, conveyor line, and collection vessel. The hopper serves as the storage container for the chocolate material, allowing for controlled feeding into the system. The air compressor generates the necessary air pressure to move the material through the conveyor line. The conveyor line, typically made of stainless steel or other food-grade materials, transports the chocolate particles using air flow. Finally, the collection vessel receives the material at the end of the conveyor line, ensuring proper storage and handling.
The operation of a chocolate pneumatic conveying system involves several steps. First, the chocolate material is fed into the hopper from a storage silo or batch container. The air compressor then activates, creating a pressure differential that draws the material into the conveyor line. As air flows through the line, it lifts and transports the chocolate particles to the collection vessel. The system can operate in either positive or negative pressure modes, depending on the specific requirements of the process. Positive pressure systems push the material through the line, while negative pressure systems create a vacuum to pull the material in.
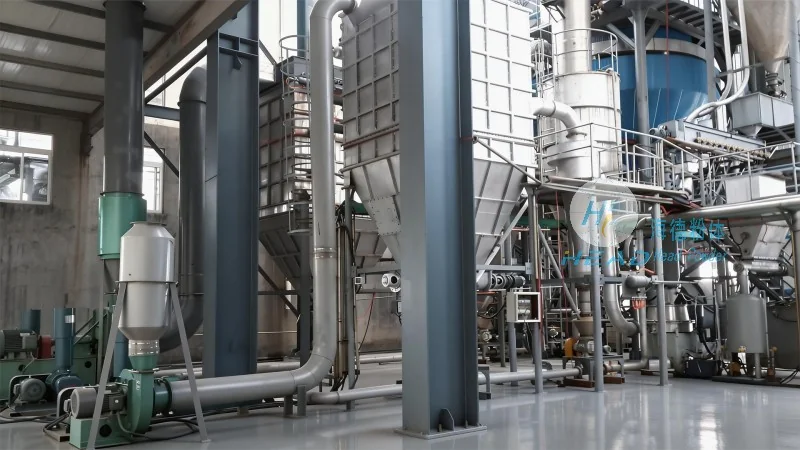
There are several advantages to implementing chocolate pneumatic conveying systems in chocolate production. One of the primary benefits is the hygienic nature of the system, as it minimizes direct contact between the material and equipment, reducing the risk of contamination from bacteria or other contaminants. Additionally, these systems are highly efficient, capable of moving large volumes of material quickly and with minimal energy consumption. They also offer flexibility in terms of layout, as the conveyor lines can be easily reconfigured to accommodate changes in production processes or facility design. Furthermore, the systems are gentle on the material, preserving the quality and texture of chocolate powders and other delicate ingredients.
Chocolate pneumatic conveying systems are used in various stages of chocolate manufacturing. They are commonly employed for transporting cocoa powder from storage to processing equipment, moving chocolate chips or other additives into mixing tanks, and conveying finished chocolate products to packaging lines. The systems are also used in quality control processes, such as sampling and testing, where precise material handling is required. In addition, these systems can be integrated with other production equipment, such as mixers and extruders, to create a seamless production line.
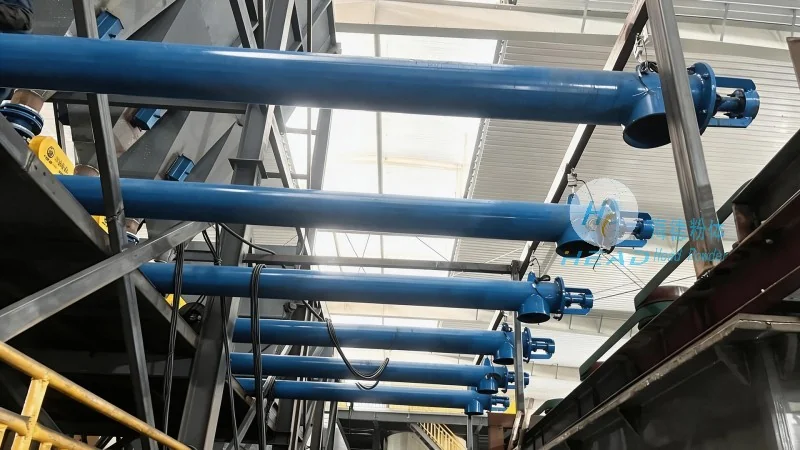
Proper maintenance is crucial for ensuring the longevity and efficiency of chocolate pneumatic conveying systems. Regular cleaning of the hopper, conveyor line, and collection vessel is necessary to prevent the buildup of chocolate residue, which can affect the system's performance and hygiene. The air compressor should be checked regularly for proper functioning, and filters should be replaced as needed to maintain air quality. Additionally, the system's pressure and flow rates should be monitored to ensure optimal operation. Proper training of operators is also essential to prevent accidents and ensure the system is used correctly.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of pneumatic conveying systems and related equipment. The company specializes in designing and producing high-quality chocolate pneumatic conveying systems tailored to the specific needs of the confectionery industry. With years of experience in the field, HeadPowder has developed a reputation for providing reliable, efficient, and hygienic equipment that meets the highest industry standards. The company's products are widely used in chocolate manufacturing facilities around the world, contributing to improved production efficiency and product quality.
Chocolate pneumatic conveying systems are an indispensable part of modern chocolate production, offering a hygienic, efficient, and flexible solution for material handling. By understanding the key components, working principles, and advantages of these systems, manufacturers can optimize their production processes and improve overall efficiency. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., the confectionery industry can continue to advance in terms of technology and quality, ensuring the production of high-quality chocolate products for consumers worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top