Aluminum sulfate, a widely used chemical in water treatment and industrial processes, requires efficient and reliable transportation methods to ensure consistent performance and operational safety. Among the various options available, pneumatic conveying stands out as a sophisticated solution that addresses many of the challenges associated with handling this material. This article explores the different aluminum sulfate transportation methods, with a particular focus on the advantages and characteristics of pneumatic conveying systems.
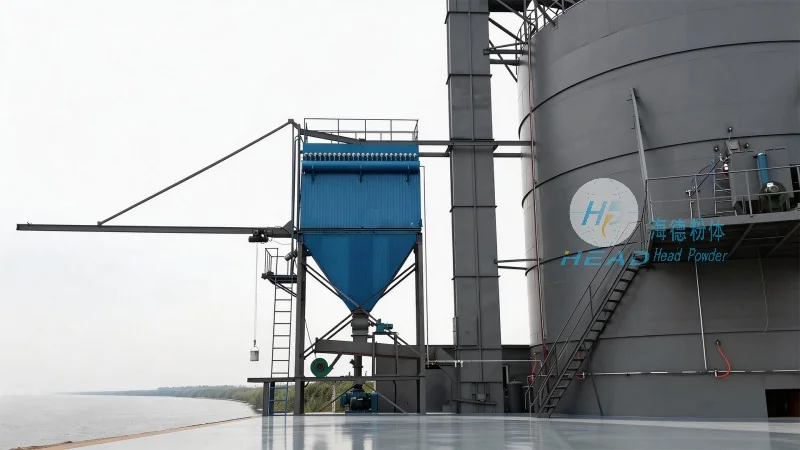
Aluminum sulfate, also known as alum, is a white crystalline solid used in a range of applications, including water purification, paper manufacturing, and dyeing processes. Due to its hygroscopic nature and potential for dust generation, transporting this material demands specialized equipment that can maintain product integrity while ensuring worker safety. Traditional methods like belt conveyors or bucket elevators may struggle with the fine powder characteristics of aluminum sulfate, leading to issues such as material degradation, dust exposure, and inefficient handling. Therefore, selecting the right transportation system is crucial for optimizing production efficiency and minimizing operational risks.
Several transportation methods are employed for aluminum sulfate, each with its own set of advantages and limitations. The most common approaches include bulk handling via trucks or railcars, manual handling for small quantities, and mechanical conveyors like screw conveyors or belt conveyors. However, these methods often fall short in terms of dust control, material flow consistency, and energy efficiency. For instance, belt conveyors may cause material degradation due to friction and may not effectively handle the fine particles of aluminum sulfate, leading to clogging or uneven distribution. Similarly, manual handling is impractical for large-scale operations and poses significant health risks due to dust inhalation.
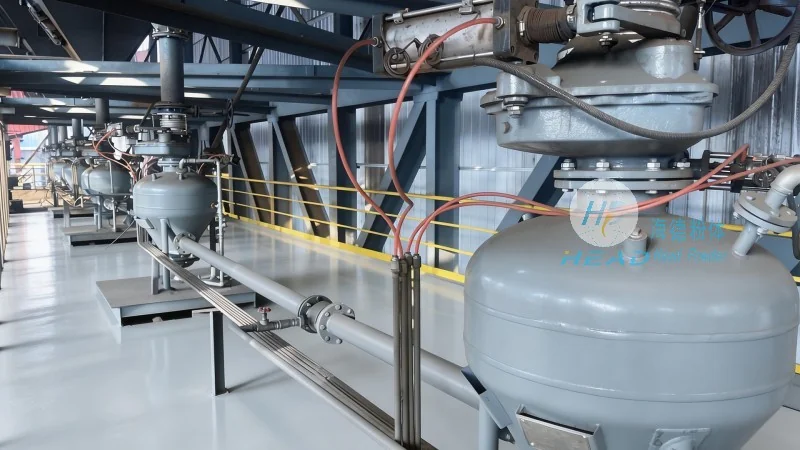
Pneumatic conveying systems utilize air or gas to transport solid materials like aluminum sulfate through a pipeline network. This method offers several key advantages that make it ideal for aluminum sulfate transportation. First, it provides excellent dust control, as the material is contained within a sealed system, reducing exposure risks for workers and minimizing environmental contamination. Second, pneumatic conveying ensures consistent material flow, preventing clogging and maintaining uniform product distribution throughout the process. Third, it offers energy efficiency compared to traditional mechanical conveyors, as the system can be optimized to use minimal air pressure while maintaining effective material transport. Additionally, pneumatic conveying systems are versatile and can be integrated with other processing equipment, allowing for seamless material transfer from storage to processing units.
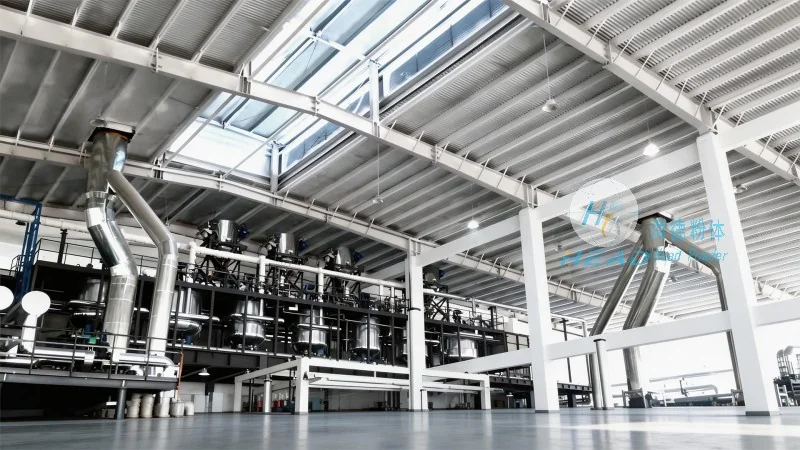
When compared to other transportation methods, pneumatic conveying offers distinct benefits for aluminum sulfate handling. The enclosed system design significantly reduces dust generation and exposure, which is critical for maintaining workplace safety and complying with environmental regulations. This is particularly important in industries where aluminum sulfate is used in large quantities, as dust can pose health risks and lead to operational disruptions. Furthermore, the ability to control air pressure and flow rates allows for precise material handling, ensuring that the material is transported at the optimal speed without causing degradation or loss. This precision is essential for maintaining the quality of aluminum sulfate, which is often sensitive to moisture and temperature changes during transport.
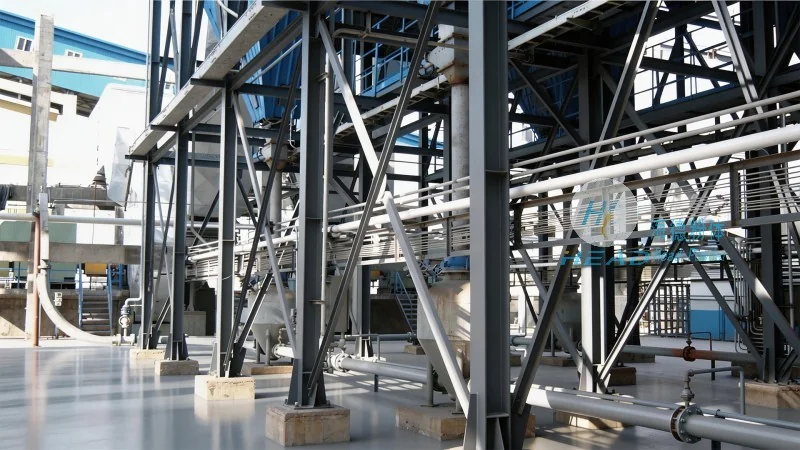
Modern pneumatic conveying systems for aluminum sulfate are equipped with advanced features that enhance their performance and reliability. These systems typically include components such as rotary airlocks, dust collectors, and pressure vessels, all designed to handle the specific characteristics of aluminum sulfate. The rotary airlock prevents material backflow and ensures a continuous flow of material through the system. The dust collector, often integrated with a filtration system, captures any fine particles that may escape, maintaining a clean and safe working environment. The pressure vessels, or hoppers, provide storage capacity and allow for controlled release of material into the conveying line, ensuring smooth operation. Additionally, many systems are equipped with monitoring and control systems that allow operators to adjust parameters in real-time, optimizing performance and reducing downtime.
For industries relying on aluminum sulfate, selecting an appropriate transportation method is essential for maintaining operational efficiency and safety. While traditional methods like belt conveyors and manual handling have their uses, pneumatic conveying emerges as the superior choice for large-scale applications. Its ability to control dust, ensure consistent flow, and integrate seamlessly with processing equipment makes it a cost-effective and reliable solution. By investing in a pneumatic conveying system, companies can enhance their production processes, reduce operational risks, and maintain the quality of their aluminum sulfate products. As a leading provider of specialized material handling solutions, Shandong HeadPowder Engineering Co., Ltd. offers advanced pneumatic conveying systems tailored to the unique needs of aluminum sulfate transportation, ensuring that clients achieve optimal performance and safety in their operations.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top