HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and implementation of advanced powder conveying systems tailored for the cement and fly ash industries. This article provides an overview of the cement fly ash powder conveying system, detailing its structural components and operational principles to help stakeholders understand its functionality and benefits.
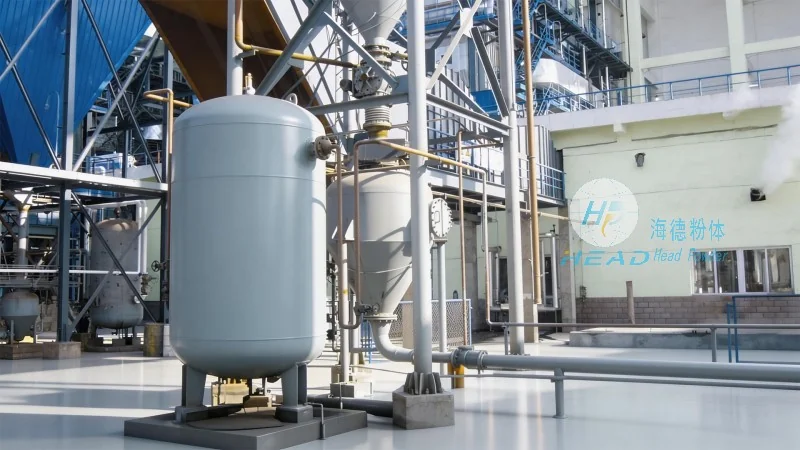
HeadPowder Engineering Co., Ltd. is a professional enterprise dedicated to providing high-quality engineering solutions for powder handling and material transportation. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted partner in the cement and related sectors. Headquartered in Shandong, China, HeadPowder leverages its extensive experience and technical expertise to develop efficient and reliable conveying systems that meet the demanding requirements of modern industrial applications.
The cement fly ash powder conveying system is a specialized equipment designed to transport bulk powders such as cement and fly ash from storage silos or production lines to processing units or storage facilities. This system is crucial for optimizing material flow, reducing operational costs, and enhancing overall production efficiency in cement manufacturing plants. The system integrates various components that work in tandem to ensure smooth and continuous powder handling, minimizing downtime and maximizing productivity.
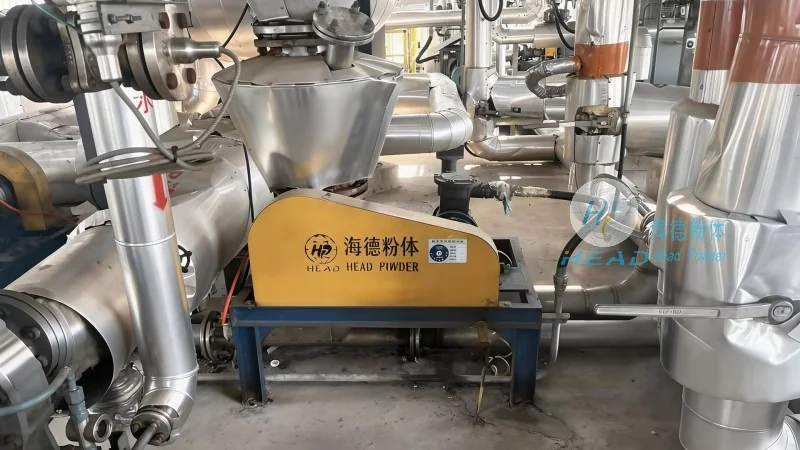
The cement fly ash powder conveying system consists of several critical components, each playing a vital role in the overall operation. These components include the hopper, feeder, conveyor pipeline, and control system. The hopper serves as the initial storage and feeding unit, where bulk powders are collected and prepared for transport. The feeder, typically a rotary or vibratory type, regulates the flow of material into the conveyor pipeline, ensuring a consistent and controlled discharge rate. The conveyor pipeline, often made of flexible or rigid materials depending on the application, transports the powder from the feeder to the destination point. The control system, equipped with sensors and automation technology, monitors the entire process, adjusting parameters as needed to maintain optimal performance and prevent issues like blockages or overloading.
The operational principle of the cement fly ash powder conveying system is based on the use of pressure or vacuum to move the powder through the pipeline. In a typical setup, the system operates under positive pressure, where a blower or fan generates the necessary airflow to push the powder forward. The feeder controls the amount of material entering the pipeline, while the control system ensures that the airflow and material flow are balanced to prevent clogging and maintain efficiency. The pipeline design, including bends and elbows, is carefully engineered to minimize pressure losses and ensure smooth material movement. The system also incorporates safety features such as pressure relief valves and emergency shut-off mechanisms to protect against potential hazards and ensure safe operation.
The cement fly ash powder conveying system offers numerous benefits that contribute to improved operational performance and cost savings. By automating the material handling process, the system reduces the need for manual labor, minimizing human error and enhancing safety. The consistent and controlled flow of powder ensures that production processes are not interrupted, leading to higher throughput and reduced downtime. Additionally, the system helps in maintaining the quality of the powder by preventing contamination and degradation during transport. The modular design of the system allows for easy integration with existing infrastructure and scalability to accommodate future expansion needs. Overall, the cement fly ash powder conveying system is a reliable and efficient solution for bulk powder transportation in the cement industry.
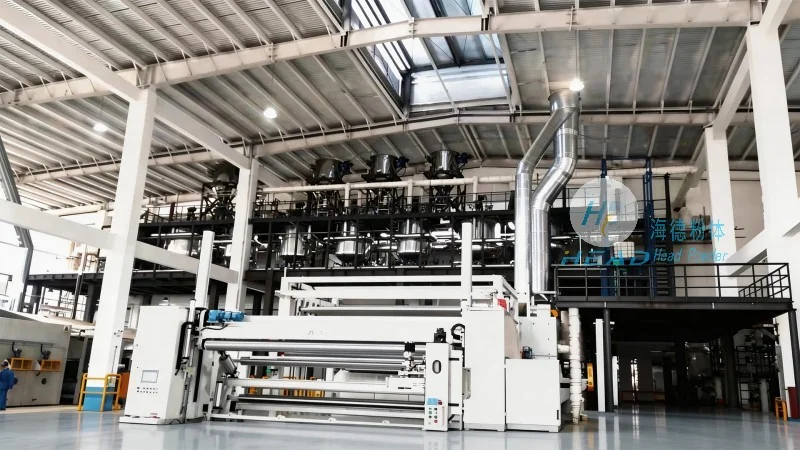
The cement fly ash powder conveying system is widely used in cement manufacturing plants, power stations, and other industrial facilities that handle large quantities of powders. Its ability to handle abrasive and dusty materials makes it suitable for applications where traditional conveying methods may not be effective. The system is particularly beneficial in environments where dust control and environmental compliance are critical, as it minimizes the release of particulate matter into the air. By improving the efficiency of material handling, the system contributes to the overall sustainability and profitability of industrial operations. HeadPowder's expertise in designing and implementing such systems ensures that clients receive tailored solutions that meet their specific operational requirements and industry standards.
In conclusion, the cement fly ash powder conveying system is a sophisticated and essential component in modern cement and related industries. With its robust structural design and efficient operational principles, the system enhances productivity, reduces costs, and ensures safe and reliable material handling. HeadPowder Engineering Co., Ltd., based in Shandong, China, is a leading provider of such systems, leveraging its technical expertise and industry experience to deliver high-quality solutions that meet the evolving needs of the market. The system's ability to handle bulk powders like cement and fly ash effectively makes it an indispensable asset for industrial operations, contributing to the growth and success of companies in the sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top