Welcome to Shandong HeadPowder Engineering Co., Ltd., a leading provider of specialized equipment for the coffee industry. Our company, commonly known as HeadPowder, is dedicated to delivering innovative solutions for coffee powder handling and transportation. Based in Shandong, China, we have established ourselves as a trusted partner for businesses seeking efficient and reliable coffee powder conveying systems.
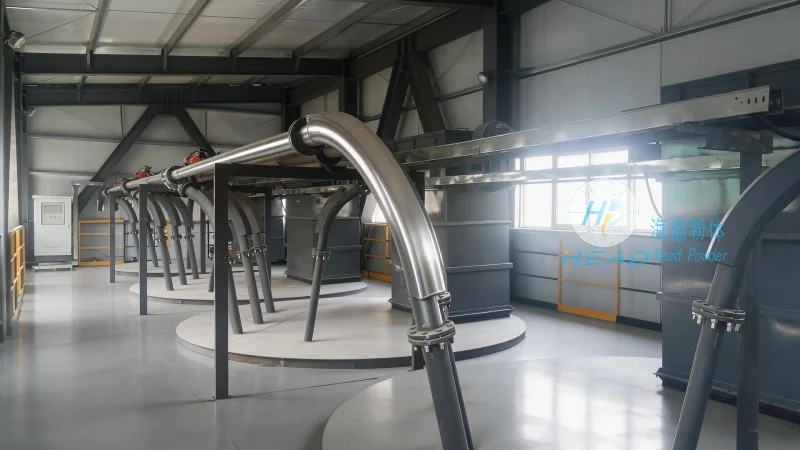
HeadPowder Engineering Co., Ltd. specializes in the design, manufacturing, and supply of coffee powder conveying equipment. Our mission is to enhance operational efficiency in coffee processing facilities by providing high-quality, durable, and user-friendly systems. With a strong commitment to technological advancement and customer satisfaction, we serve a diverse range of clients in the coffee sector, from small-scale roasters to large-scale production plants.
Coffee powder conveying systems are essential for the smooth operation of coffee processing and distribution. These systems are designed to transport coffee powder from storage silos or processing units to packaging lines or other destinations within a facility. The core components of a typical coffee powder conveying system include feeders, conveyors, and control mechanisms, all working in tandem to ensure consistent and safe material handling.
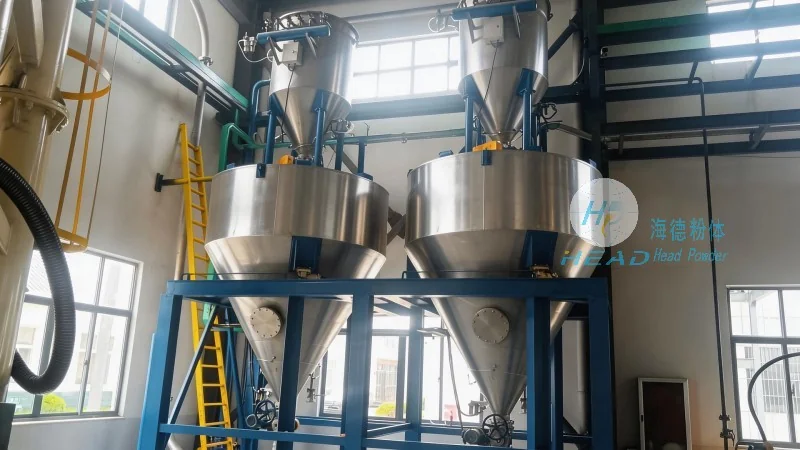
The structure of a coffee powder conveying system typically involves a hopper or silo where coffee powder is stored. A feeder, often a rotary or vibratory type, regulates the flow of powder into the conveyor. The conveyor itself may be a pneumatic system, using air pressure to move the powder through a pipeline, or a mechanical system, such as a screw or belt conveyor, which physically transports the material. Control valves and sensors are integrated to monitor and adjust the flow rate, ensuring optimal performance and preventing blockages or overloading.
The principle behind coffee powder conveying lies in the efficient transfer of bulk materials while maintaining product integrity. For coffee powder, which is a fine, abrasive substance, the conveying system must be designed to minimize particle degradation and prevent clogging. Pneumatic conveying systems are particularly effective for this purpose, as they use air to create a low-pressure environment that allows the powder to flow smoothly through the pipeline. Mechanical conveyors, on the other hand, rely on physical force to move the material, which may be more suitable for larger particles or when air quality is a concern.
In both systems, the key is to maintain a consistent flow rate and pressure. This is achieved through the use of variable speed drives, pressure regulators, and flow meters. These components work together to ensure that the coffee powder is conveyed at the correct speed and volume, reducing the risk of product loss or contamination. Additionally, the system may include cleaning mechanisms to prevent the buildup of coffee residue, which is crucial for maintaining hygiene standards in food processing environments.
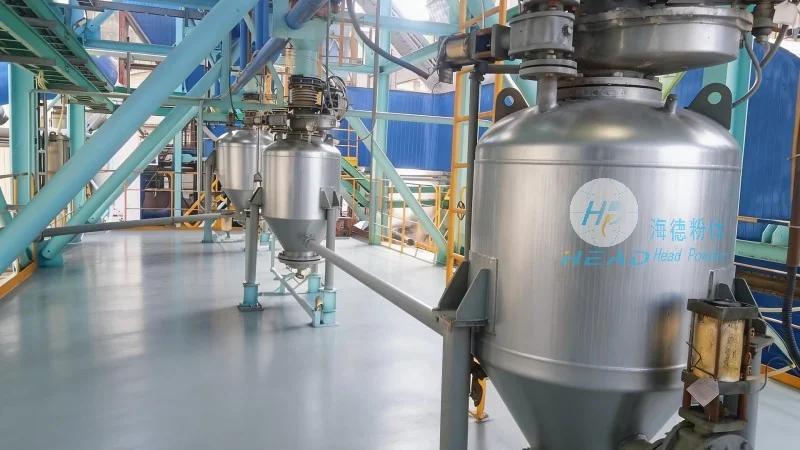
Implementing a coffee powder conveying system offers numerous benefits for coffee processing businesses. Firstly, it enhances operational efficiency by automating the material handling process, reducing the need for manual labor and minimizing the risk of human error. This leads to increased productivity and lower labor costs. Secondly, the systems improve product quality by preventing contamination and maintaining the integrity of the coffee powder. This is particularly important for specialty coffees, where even small changes in particle size or moisture content can affect the final product's flavor and aroma.
Another significant benefit is the reduction of operational costs. By optimizing the flow of coffee powder, businesses can minimize energy consumption and reduce the need for frequent maintenance or cleaning. The durability of our conveying systems, built with high-quality materials and robust construction, ensures long-term reliability and minimal downtime. This translates to lower maintenance expenses and higher return on investment over the system's lifespan.
HeadPowder Engineering Co., Ltd. understands that each coffee processing facility has unique requirements. Therefore, we offer customized coffee powder conveying solutions tailored to specific production needs. Whether a client requires a small-scale system for a boutique roaster or a large-scale system for a commercial coffee producer, our team of engineers works closely with clients to design and implement the most suitable solution. Our expertise in material handling and coffee processing allows us to address the specific challenges faced by each business, ensuring that the final system meets all operational and regulatory standards.
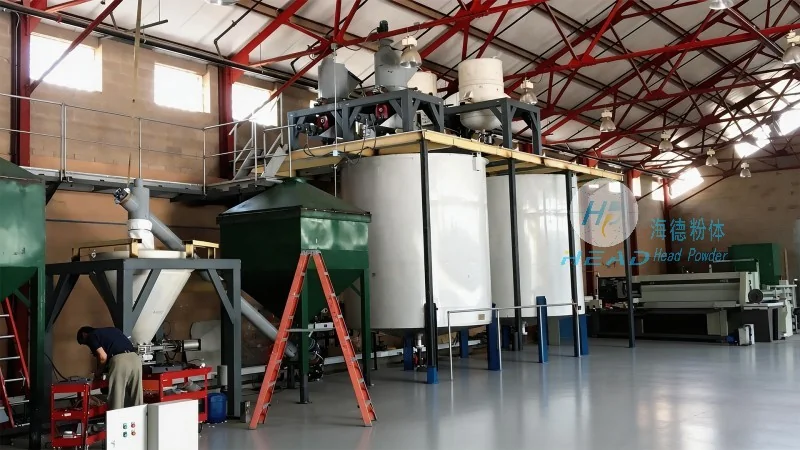
The applications of coffee powder conveying systems are diverse and widespread. They are used in coffee roasting facilities to transport roasted coffee beans to grinding and packaging areas. In coffee processing plants, these systems are crucial for moving ground coffee from storage to blending and packaging lines. Additionally, they are employed in coffee distribution centers to move large quantities of coffee powder to various markets. Our systems are designed to handle different types of coffee powders, including whole bean, ground coffee, and instant coffee, ensuring versatility and adaptability to various production processes.
At Shandong HeadPowder Engineering Co., Ltd., we are committed to providing top-tier coffee powder conveying systems that meet the highest standards of efficiency, reliability, and quality. Our company, HeadPowder, is dedicated to supporting the coffee industry with innovative solutions that enhance productivity and product quality. With our headquarters in Shandong, China, we serve clients globally, delivering customized equipment that meets their specific needs. By choosing HeadPowder, businesses can ensure that their coffee powder handling processes are optimized for performance and longevity, contributing to their overall success in the competitive coffee market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top