Efficient and reliable powder handling is a critical requirement across various industrial sectors, including pharmaceuticals, chemicals, food processing, and manufacturing. The intelligent centralized powder handling system, developed by Shandong HeadPowder Engineering Co., Ltd., represents a cutting-edge solution designed to enhance operational efficiency, safety, and control in powder processing applications.
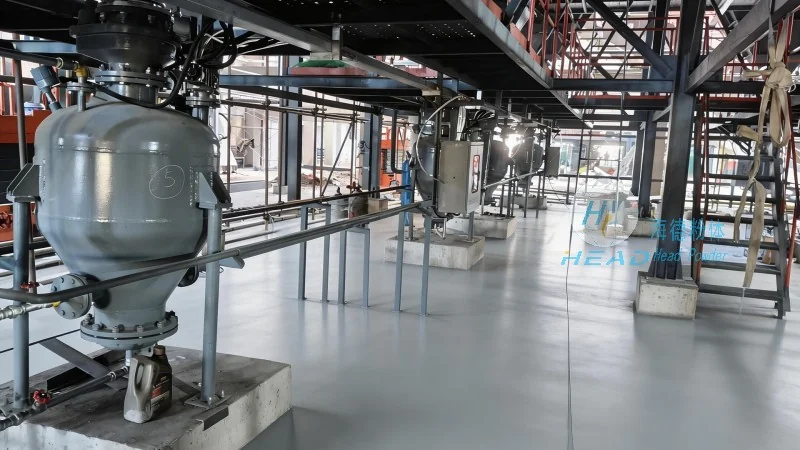
The intelligent centralized powder handling system is engineered to centralize the management and transport of powders from storage to processing points. This system integrates advanced automation technologies, such as sensors, control systems, and data analytics, to ensure precise and safe powder handling. By consolidating multiple powder handling operations into a single, centralized unit, the system minimizes the risk of cross-contamination, reduces material waste, and optimizes workflow. The design is tailored to meet the diverse needs of industries that handle sensitive or hazardous powders, providing a robust and adaptable solution for modern manufacturing environments.
The intelligent centralized powder handling system consists of several core components that work in harmony to achieve efficient powder transport. The primary components include bulk material storage silos, pneumatic conveying lines, control panels, and monitoring systems. The system operates on the principle of pneumatic conveying, where powders are transported through a network of pipes using compressed air or other gases. This method allows for the safe and efficient movement of powders over long distances without the need for mechanical contact, reducing wear and tear on equipment and minimizing the risk of contamination.
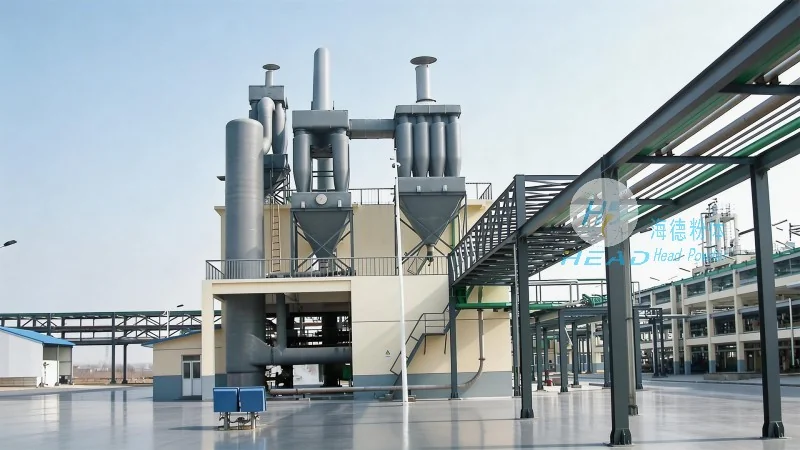
At the heart of the system is the control panel, which integrates sensors and automation software to monitor and regulate the flow of powders. Real-time data from sensors is processed to adjust the conveying speed, pressure, and other parameters, ensuring optimal performance. The system also includes safety features, such as pressure relief valves and emergency shut-off mechanisms, to prevent accidents and protect personnel and equipment. The modular design of the system allows for easy expansion and customization, enabling it to adapt to changing production requirements over time.
Implementing the intelligent centralized powder handling system offers numerous benefits for industrial operations. Firstly, it enhances operational efficiency by streamlining the powder handling process, reducing downtime, and improving throughput. The centralized control allows for better coordination of multiple processing steps, leading to increased productivity. Secondly, the system improves safety by minimizing human exposure to powders and reducing the risk of dust explosions through advanced safety features and enclosed systems. Thirdly, it enhances product quality by ensuring consistent powder flow and reducing contamination, which is crucial for industries like pharmaceuticals and food processing where product purity is paramount.
Additionally, the system promotes sustainability by reducing material waste and energy consumption. The efficient conveying technology minimizes the need for manual handling, which not only saves labor costs but also reduces the environmental impact of powder processing. The data-driven approach of the system enables continuous improvement, as performance metrics can be analyzed to identify areas for optimization and further enhance operational efficiency.
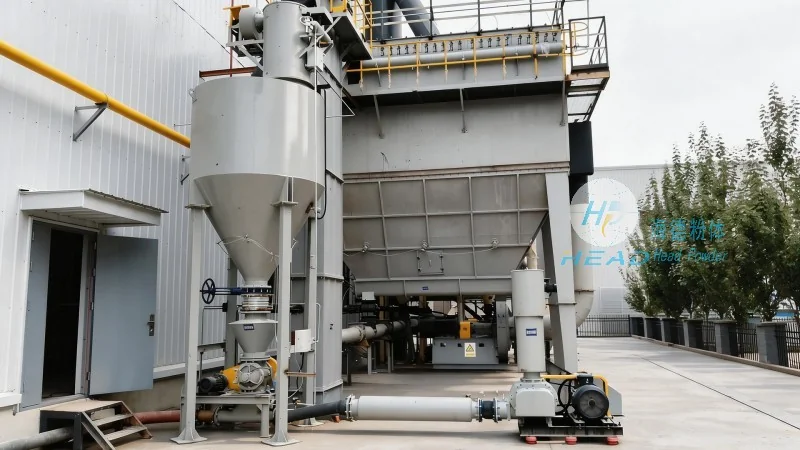
The intelligent centralized powder handling system is widely applicable across various industries. In the pharmaceutical industry, it ensures the safe and sterile handling of active pharmaceutical ingredients (APIs) and excipients, maintaining compliance with stringent regulatory standards. In the chemical industry, it facilitates the transport of hazardous chemicals while protecting workers and the environment. In the food and beverage industry, it ensures the hygienic handling of ingredients, preserving product quality and safety. The system's adaptability makes it suitable for both small-scale and large-scale production facilities, providing a scalable solution for growing businesses.
By integrating advanced automation and control technologies, the intelligent centralized powder handling system from Shandong HeadPowder Engineering Co., Ltd. sets a new standard for powder handling efficiency and reliability. The system's modular design, safety features, and data-driven approach make it an ideal choice for industries seeking to enhance their operational performance while maintaining high standards of safety and quality. As industries continue to evolve and demand more efficient processing solutions, this intelligent system offers a robust and future-proof solution for powder handling needs.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top