Industrial salt, a critical raw material across sectors like chemical manufacturing, food processing, and de-icing, demands efficient bulk transport solutions. Industrial salt pneumatic conveying systems have become a preferred choice due to their adaptability, cost-effectiveness, and minimal manual intervention. This article explores the structural components and operational principles of such systems, with insights from Shandong HeadPowder Engineering Co., Ltd., a leading provider based in China.
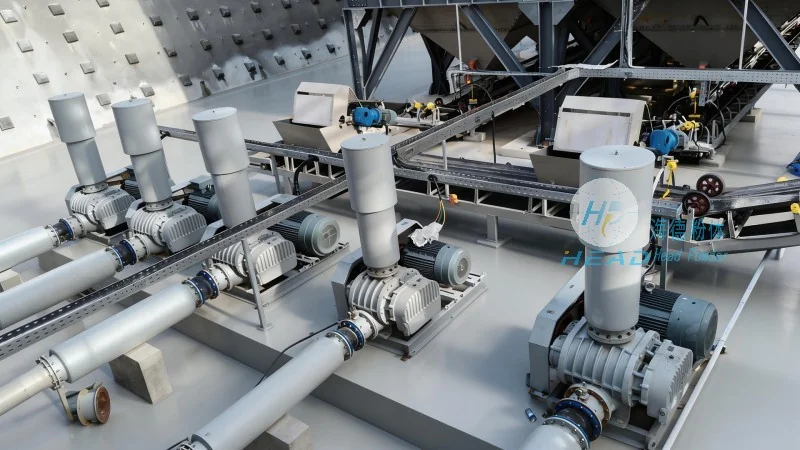
An industrial salt pneumatic conveying system comprises core elements that ensure seamless material transport. These include a hopper for storage, a feeder to regulate flow, a conveying line (ducts or pipes), a dust collector for air purification, and a receiver for discharged material. Each component is vital for efficiency and safety. The hopper holds substantial industrial salt, feeding the system steadily. The feeder—often a rotary valve or screw type—controls discharge rate, preventing over/underflow. The conveying line uses air as the medium: positive pressure systems employ a blower to push material, while negative pressure systems use a vacuum to draw it. The dust collector captures airborne particles, ensuring environmental compliance and workplace safety. The receiver collects the conveyed salt, completing the cycle.
The operational principle centers on air as the conveying medium. In positive pressure systems, a blower generates high-pressure air to propel salt particles from the hopper. The feeder maintains an optimal air-to-material ratio for consistent flow. Air velocity must keep particles suspended to avoid blockages. Negative pressure systems use a vacuum pump to draw material, with duct design critical for efficiency and energy use. The dust collector captures entrained particles, ensuring clean exhaust. The receiver collects salt for downstream use, such as chemical processing or de-icing.
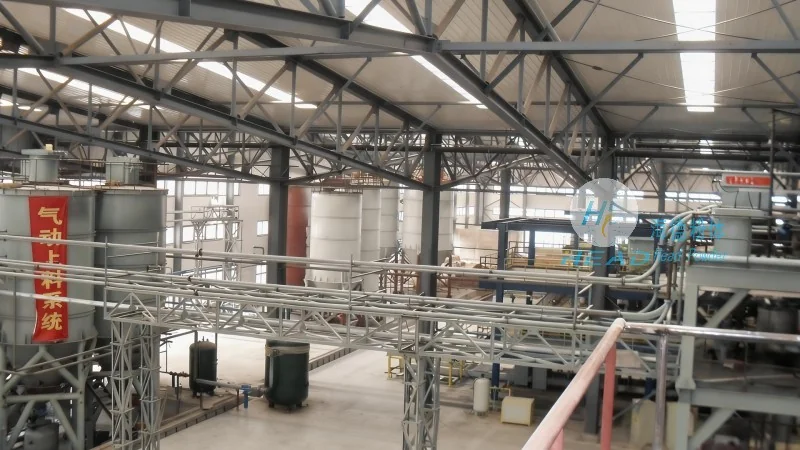
Compared to traditional methods like belt conveyors, these systems offer distinct benefits. They enable long-distance transport without multiple transfer points, reducing spillage and contamination risks. Enclosed design minimizes dust exposure, enhancing safety and regulatory compliance. Flexibility allows route changes without major infrastructure adjustments, valuable for evolving production processes. Fewer moving parts mean lower maintenance needs, and optimized designs improve energy efficiency, leading to long-term cost savings. Overall, they provide a reliable, efficient solution for industrial salt handling.
The systems' versatility suits diverse applications. In chemicals, they transport raw salt to processing units for products like sodium hydroxide. In food processing, they deliver hygienic salt for preservation. For de-icing, they efficiently supply salt to roads and highways, critical for winter safety. In mining, they handle salt as a flux or reagent, ensuring consistent process performance. These applications rely on the systems' ability to handle bulk quantities reliably.
Shandong HeadPowder Engineering Co., Ltd. specializes in customizing systems tailored to client needs. Based in China, the company leverages expertise to integrate seamlessly with existing processes. Customization includes material selection for hoppers/ducts (e.g., stainless steel for corrosion resistance) to match salt properties. Control systems integrate with client automation for real-time monitoring. The company considers conveying capacity, distance, and environmental regulations during design. Their understanding of industrial salt challenges ensures reliable, long-lasting solutions, with maintenance and support to maximize system lifespan.
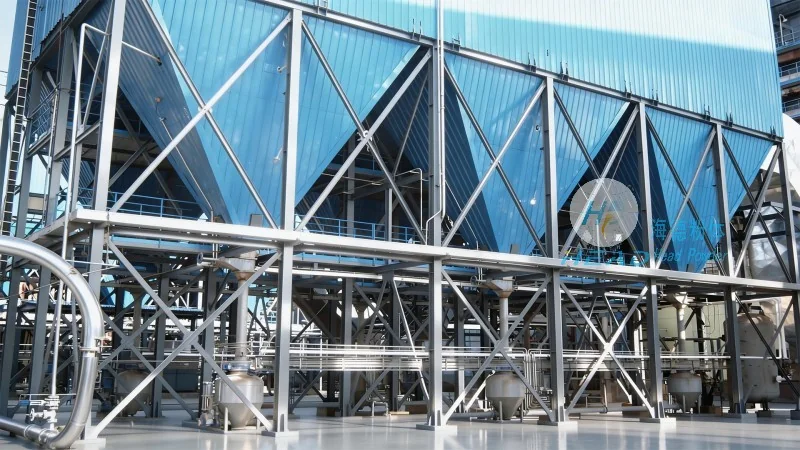
Regular maintenance is key to system longevity. Inspections of hopper, feeder, and ducts detect wear or damage. Dust collectors require periodic cleaning to avoid clogs. Blowers/vacuum pumps need lubrication and filter replacement. Feeder mechanisms are adjusted for optimal flow. Shandong HeadPowder provides maintenance services, leveraging expertise in troubleshooting and spare parts suitable for abrasive industrial salt. This support ensures consistent performance and extended system life.
Industrial salt pneumatic conveying systems represent a sophisticated, efficient solution for bulk material transport. Their structural components and air-based operation ensure reliability and safety. Advantages like flexibility, low maintenance, and environmental compliance make them ideal for industrial salt handling. Shandong HeadPowder Engineering Co., Ltd. contributes to this efficiency by providing customized, reliable systems tailored to client needs, supporting operational success worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top