Desulfurization sodium bicarbonate, also known as sodium bicarbonate used in flue gas desulfurization processes, is a critical chemical in modern industrial applications. The efficient handling and transportation of this material are essential for maintaining the performance and reliability of desulfurization systems. Pneumatic conveying technology offers a highly effective solution for moving desulfurization sodium bicarbonate, providing advantages such as dust-free operation, reduced material degradation, and improved safety compared to traditional methods like belt conveyors or bucket elevators.
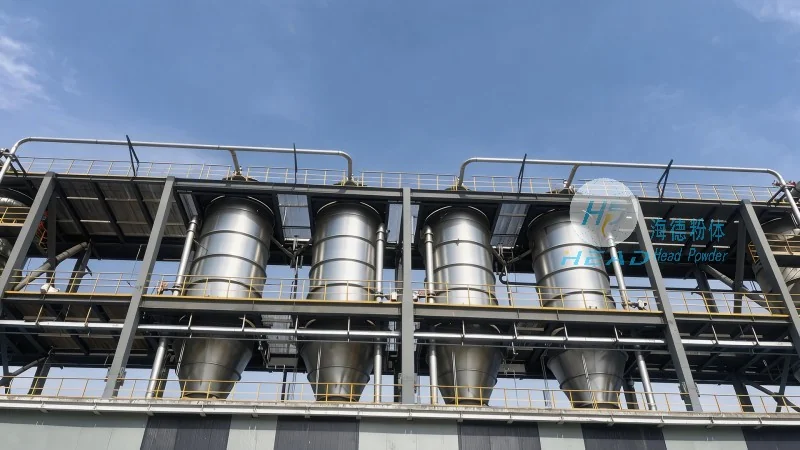
Pneumatic conveying systems for desulfurization sodium bicarbonate typically consist of several key components that work in concert to transport the material from a source to a destination. The primary components include a material hopper or feeder, a conveying pipeline, a pneumatic transport device (such as a positive displacement blower or rotary airlock), and a discharge unit. Each component plays a vital role in ensuring the smooth and efficient operation of the system.
The material hopper or feeder is designed to store and feed the desulfurization sodium bicarbonate into the conveying system. It is usually equipped with a level indicator and a discharge valve to control the flow rate of the material. The conveying pipeline is made of durable materials, such as stainless steel or high-density polyethylene, to withstand the abrasive nature of the sodium bicarbonate and the pressure from the air flow. The pipeline system may include bends, elbows, and expansion joints to accommodate changes in direction and elevation. The pneumatic transport device, often a positive displacement blower, generates the necessary air pressure to move the material through the pipeline. This device is typically equipped with a filter to remove any particulate matter from the air, ensuring clean operation. The discharge unit, which may be a rotary airlock or a pressure vessel, regulates the release of the material at the destination, preventing backflow and maintaining consistent flow rates.
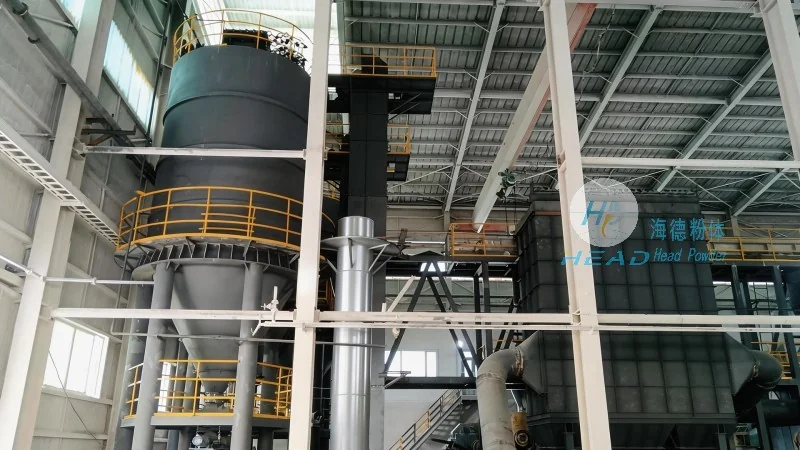
The core principle of pneumatic conveying for desulfurization sodium bicarbonate is the use of compressed air to create a flow that transports the material particles through the pipeline. There are two main types of pneumatic conveying systems: dilute-phase and dense-phase. Dilute-phase systems operate at lower air velocities and are suitable for short distances or low material loads, while dense-phase systems use higher air velocities and are ideal for longer distances or higher material loads. In both systems, the compressed air is introduced into the pipeline at a specific point, creating a pressure differential that draws the material particles into the air stream. The material is then carried through the pipeline by the air flow and discharged at the receiving end.
Implementing pneumatic conveying systems for desulfurization sodium bicarbonate offers several significant advantages over traditional material handling methods. First, it provides a dust-free environment, which enhances workplace safety and reduces the risk of respiratory issues for personnel. Second, the system minimizes material degradation, as the material is not subjected to mechanical stress or impact during transportation. Third, pneumatic conveying systems are highly flexible, allowing for changes in the layout or direction of the pipeline without major modifications. Fourth, they offer improved energy efficiency compared to other methods, as the compressed air can be recycled and reused within the system. Finally, the system is easy to maintain and operate, with minimal downtime required for routine maintenance.
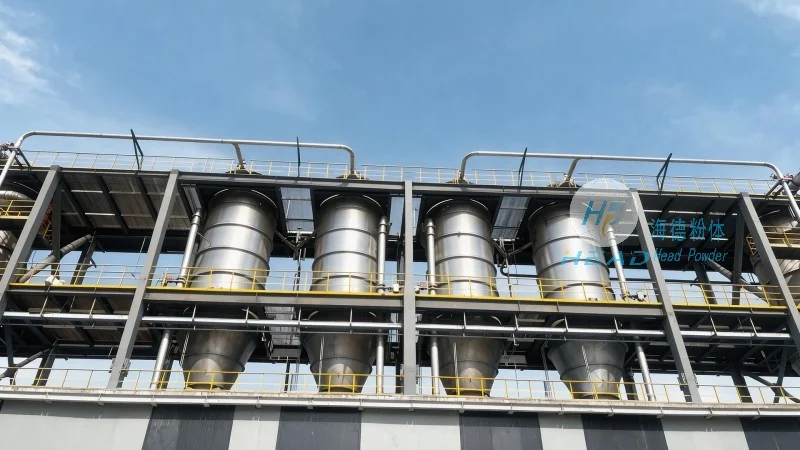
Pneumatic conveying systems for desulfurization sodium bicarbonate are widely used in various industries, including power generation, chemical manufacturing, and industrial waste treatment. In power plants, these systems are used to transport sodium bicarbonate from storage silos to the desulfurization reactors, ensuring a continuous and reliable supply of the chemical. In chemical manufacturing facilities, the systems are employed to move the material between processing units, such as reactors, filters, and storage tanks. In industrial waste treatment plants, pneumatic conveying is used to transport sodium bicarbonate for use in scrubbing processes, helping to reduce emissions and meet environmental regulations.
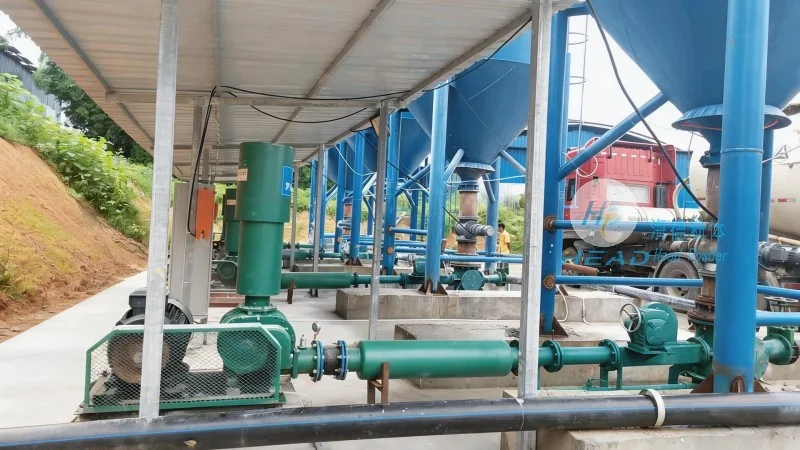
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing customized pneumatic conveying systems tailored to the specific needs of clients. The company's expertise lies in integrating these systems with existing infrastructure, ensuring seamless operation and minimal disruption to current processes. By working closely with clients, HeadPowder engineers can develop solutions that optimize material flow, reduce operational costs, and enhance overall system performance. The company's commitment to quality and innovation has made it a trusted partner for businesses seeking reliable and efficient material handling solutions.
In conclusion, pneumatic conveying systems for desulfurization sodium bicarbonate are a critical component of modern industrial operations. By understanding the structure and principle of these systems, businesses can make informed decisions about their material handling strategies, leading to improved efficiency, reduced costs, and enhanced safety. As the demand for sustainable and efficient industrial processes continues to grow, the importance of reliable pneumatic conveying systems will only increase. With its expertise and commitment to quality, Shandong HeadPowder Engineering Co., Ltd. remains at the forefront of providing advanced material handling solutions for the desulfurization industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top