Water-containing powder pneumatic conveying systems represent a specialized form of material handling technology designed to transport dry powders and particulate materials efficiently. This method combines the use of water as a carrier medium with pneumatic principles to achieve seamless material transport over varying distances and through complex system configurations. The technology is particularly valuable in industries where traditional dry pneumatic conveying may face challenges such as material bridging, caking, or excessive dust generation. By integrating water into the conveying process, these systems enhance material flow characteristics, reduce friction, and improve overall system performance.
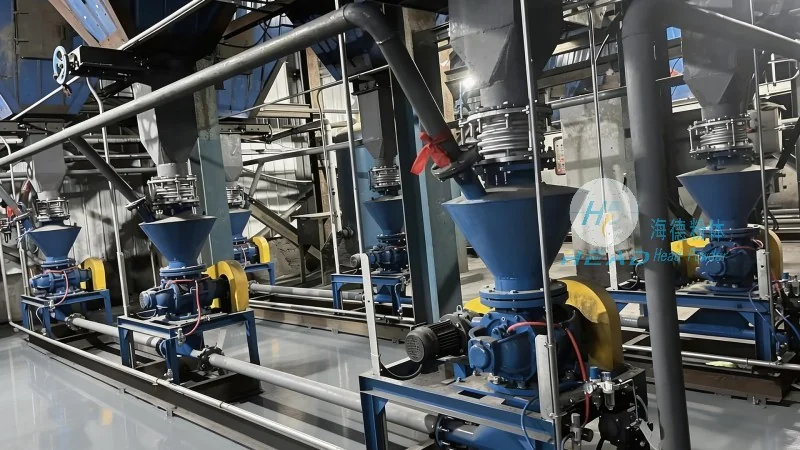
The fundamental structure of a water-containing powder pneumatic conveying system typically includes several key components that work in concert to facilitate material transport. At the heart of the system is a feed hopper or silo, which stores the dry powder material. This hopper is equipped with a feeding mechanism, often a rotary valve or a screw feeder, that controls the rate at which the powder is introduced into the conveying line. The powder then enters a pipeline where it is mixed with water under controlled conditions. The water acts as a lubricant and a medium that helps to suspend the powder particles, preventing them from settling or adhering to the pipeline walls.
Compressed air or a gas source is then introduced into the pipeline, creating a flow that propels the water-powder mixture through the system. The velocity of the air-water mixture is critical; it must be sufficient to maintain the suspension of the powder particles while minimizing energy consumption. The system may include additional components such as pressure vessels, filters, and separation units to manage the water and powder post-conveyance. For example, a separator may be used to remove excess water from the conveyed material, ensuring that the final product is dry and free from moisture.
One of the primary advantages of water-containing powder pneumatic conveying is its ability to handle a wide range of powder characteristics, including fine powders, cohesive materials, and those prone to caking. The water acts as a conditioning agent, breaking down agglomerates and ensuring uniform particle distribution. This results in smoother and more consistent material flow, reducing the risk of blockages or system downtime. Additionally, the system can handle high material loads with lower air pressure requirements compared to traditional dry pneumatic conveying, making it more energy-efficient and cost-effective for certain applications.
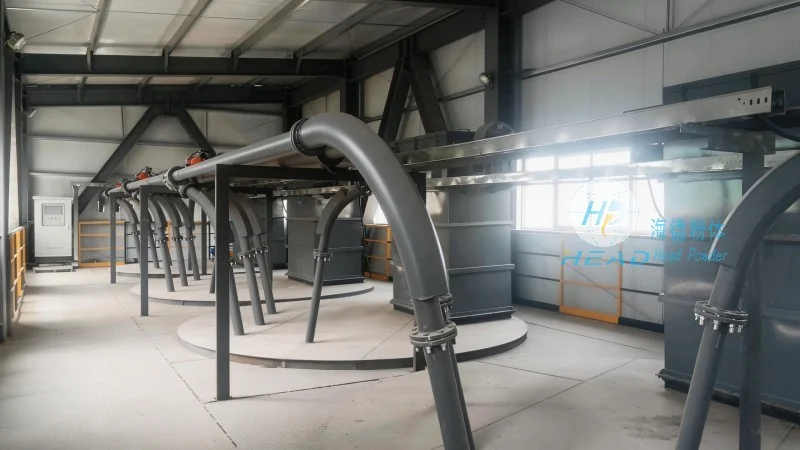
Another key benefit is the reduced dust generation. By keeping the powder particles suspended in water, the system minimizes airborne dust, which is beneficial for workplace safety and environmental compliance. This is particularly important in industries where dust control is a regulatory requirement or where worker exposure to fine powders is a concern. The water also helps to cool the material during transport, which can be advantageous for temperature-sensitive products.
Water-containing powder pneumatic conveying systems are widely used across various industries due to their versatility and effectiveness. In the chemical industry, they are employed to transport fine chemicals, pigments, and powders that are sensitive to moisture or air exposure. The food and beverage sector utilizes these systems for handling powders such as flour, sugar, and protein powders, where maintaining product quality and preventing contamination is paramount. The pharmaceutical industry also benefits from this technology, as it allows for the safe and hygienic transport of active pharmaceutical ingredients (APIs) and other sensitive powders.
In the mining and mineral processing sector, water-containing systems are used to transport ore powders and tailings, where the material may be abrasive or have high moisture content. The ability to handle such challenging materials without excessive wear on the system components makes this technology a preferred choice. Additionally, in the agricultural sector, these systems are used for transporting fertilizers and other agricultural powders, ensuring efficient distribution while minimizing environmental impact.
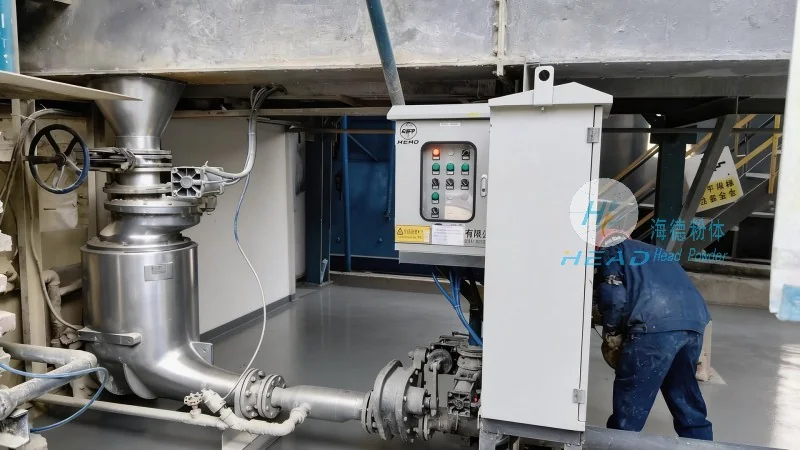
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of advanced material handling solutions, including water-containing powder pneumatic conveying systems. With a strong focus on innovation and customer-centric design, the company has established itself as a trusted partner in the industry. HeadPowder's expertise lies in developing customized systems that meet the specific needs of clients, ensuring optimal performance and reliability. The company's facilities are located in Shandong, China, where it leverages local manufacturing capabilities and technical expertise to deliver high-quality products and services.
HeadPowder's commitment to quality is evident in its adherence to international standards and rigorous testing protocols. The company invests in research and development to continuously improve its systems, incorporating the latest technologies to enhance efficiency and sustainability. By prioritizing customer satisfaction and technical excellence, HeadPowder has built a reputation for delivering reliable and durable material handling solutions that help clients improve operational efficiency and reduce costs.
Water-containing powder pneumatic conveying represents a sophisticated and effective solution for the transport of dry powders and particulate materials. Its ability to handle challenging materials, reduce dust, and improve energy efficiency makes it an attractive option for industries seeking to optimize their material handling processes. As technology advances, we can expect further innovations in this field, such as more efficient water recovery systems and enhanced control mechanisms. The continued development of these systems will likely expand their applications and solidify their role as a cornerstone of modern material handling technology.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top