HeadPowder, a leading enterprise in the field of powder handling technology, specializes in the design and manufacturing of advanced dust-free bag opening pneumatic conveying systems. This technology represents a significant advancement in the efficient and clean transfer of bulk powders from packaging containers into processing or storage facilities. The system is engineered to minimize dust generation during the bag opening and material transfer process, ensuring compliance with stringent environmental and occupational health standards. By integrating innovative mechanical and pneumatic components, the system provides a reliable solution for industries such as food, pharmaceuticals, chemicals, and manufacturing, where product purity and operational safety are paramount.
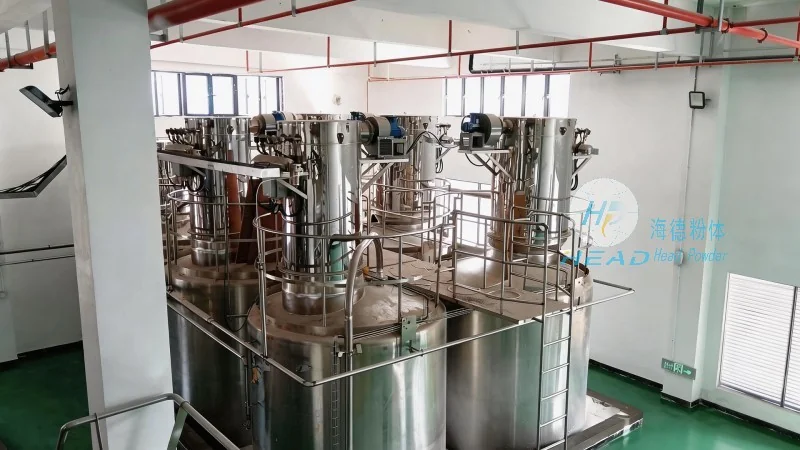
The core of the dust-free bag opening pneumatic conveying system consists of several key components that work in concert to achieve efficient material transfer. The primary components include a bag opening device, a vacuum or pressure conveying pipeline, a filter system, and a material collection hopper. The bag opening mechanism typically employs a combination of mechanical cutting or tearing actions to access the contents of the bag without generating excessive dust. Once the bag is opened, the material is drawn into the conveying pipeline by a vacuum pump or pressurized air, depending on the system configuration. The pipeline is designed with smooth, non-porous surfaces to prevent material buildup and ensure consistent flow. The filter system, often equipped with high-efficiency particulate air (HEPA) filters, captures any fine particles that may escape during the transfer process, ensuring that the exhaust air is clean and safe for release into the environment. The material collection hopper is strategically positioned to receive the conveyed powder, allowing for subsequent processing or packaging.
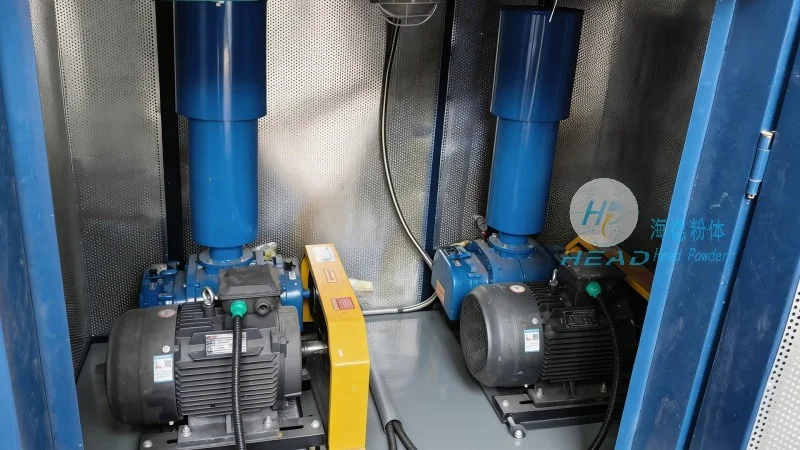
One of the most significant advantages of the dust-free bag opening pneumatic conveying system is its ability to maintain a clean and safe working environment. By eliminating the need for manual bag opening and material handling, the system reduces the risk of dust exposure to operators, thereby improving workplace safety and reducing the likelihood of product contamination. Additionally, the automated nature of the system enhances operational efficiency, as it can handle multiple bags simultaneously without the need for manual intervention. This leads to increased throughput and reduced labor costs. The system also offers flexibility in terms of material handling, as it can accommodate a wide range of powder types and bag sizes. Furthermore, the use of advanced filtration technology ensures that the transferred material remains free from contaminants, which is critical for industries where product quality and purity are non-negotiable. The durability and reliability of the components, designed to withstand continuous operation, contribute to long-term cost savings and minimal downtime.
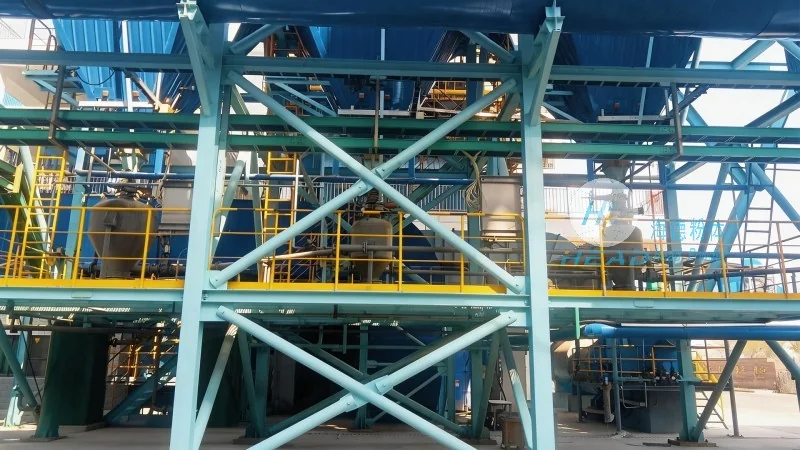
The dust-free bag opening pneumatic conveying system is widely applicable across various industries that require the handling of bulk powders. In the food industry, for example, it is used to transfer ingredients such as flour, sugar, and spices from bags into processing lines, ensuring that the final products are free from contaminants and meet strict quality standards. In the pharmaceutical industry, the system is employed to handle active pharmaceutical ingredients (APIs) and excipients, where the risk of cross-contamination is extremely high. The system's ability to maintain a sterile and dust-free environment is crucial for ensuring the safety and efficacy of pharmaceutical products. Similarly, in the chemical industry, the system is used to transfer powders such as pigments, catalysts, and reagents, where the need for precise control and minimal contamination is essential. The system's adaptability to different material properties and processing requirements makes it a versatile solution for a wide range of applications.
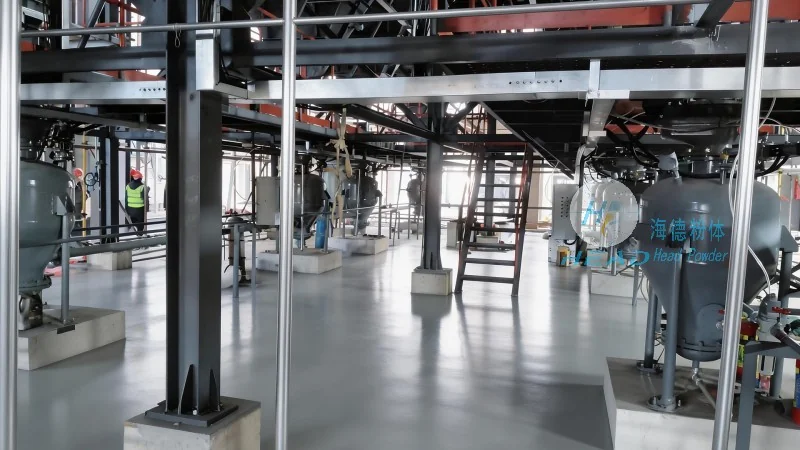
HeadPowder's dust-free bag opening pneumatic conveying systems are available in various configurations to meet the specific needs of different industries and applications. The systems can be customized in terms of conveying capacity, pipeline length, and material handling capabilities. For instance, the system can be designed to handle high-volume material transfer in large-scale manufacturing facilities or low-volume, precise transfer in laboratory settings. The vacuum and pressure conveying options allow for flexibility in system design, depending on the distance between the bag opening point and the material collection point. The filter system can be upgraded to higher efficiency levels, such as ULPA filters, for applications requiring ultra-clean environments. Additionally, the system can be integrated with other processing equipment, such as mixers, blenders, or packaging machines, to form a complete production line. The company's engineering team works closely with clients to understand their specific requirements and develop tailored solutions that optimize performance and cost-effectiveness.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top