Pharmaceutical bulk material pneumatic conveying equipment is a specialized system designed for the efficient and hygienic transportation of powders and granules within pharmaceutical manufacturing facilities. Developed by Shandong HeadPowder Engineering Co., Ltd., a leading provider in the industry, this equipment ensures compliance with stringent regulatory standards while delivering reliable performance in various production scenarios.
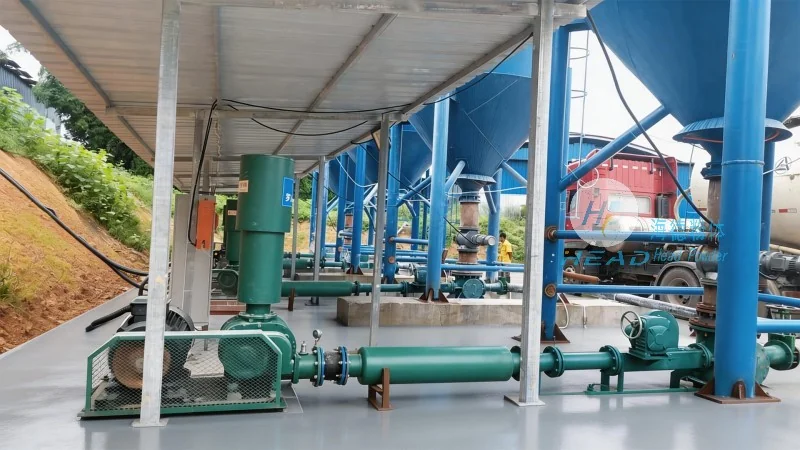
At the core of pharmaceutical pneumatic conveying systems is the ability to move bulk materials like active pharmaceutical ingredients (APIs), excipients, and other raw materials with precision and minimal contamination. The system typically comprises a series of components including a hopper, feeder, air compressor, conveying line, and collection vessel. Each component plays a critical role in maintaining the integrity of the material and ensuring operational efficiency.
The hopper serves as the storage container for the bulk material, providing a controlled environment to prevent moisture and contamination. The feeder, often a rotary valve or screw feeder, regulates the flow of material into the conveying line, ensuring a consistent and controlled discharge rate. The air compressor generates the necessary pressure to create airflow, which propels the material through the system. The conveying line, usually made of stainless steel or other sanitary materials, transports the material while maintaining product purity. Finally, the collection vessel receives the material at the destination, completing the transportation process.
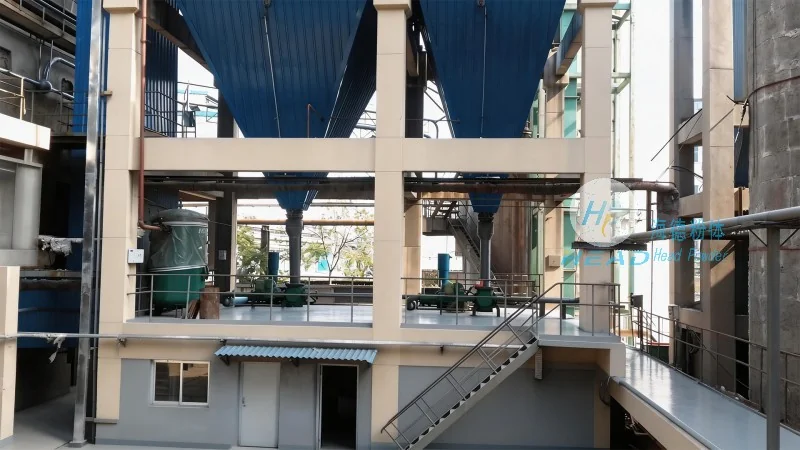
The operation process begins with the material being loaded into the hopper. The feeder then controls the discharge rate, feeding the material into the conveying line. Simultaneously, the air compressor produces compressed air, which is introduced into the system. The air flow creates a pressure differential that lifts and transports the material through the conveying line to the collection vessel. This process is typically continuous, allowing for seamless material transfer between different stages of the pharmaceutical production line.
The working principle of pharmaceutical pneumatic conveying is based on the use of air as the conveying medium. There are two primary types of pneumatic conveying systems: pressure and vacuum. In a pressure system, the air compressor supplies compressed air to the conveying line, creating positive pressure that forces the material to move. In a vacuum system, a vacuum pump creates a negative pressure at the collection end, drawing the material through the line. Both systems rely on the principle of fluidization, where the material is suspended in the air stream and transported as a slurry. This method minimizes product degradation, reduces contamination risks, and ensures consistent material handling.
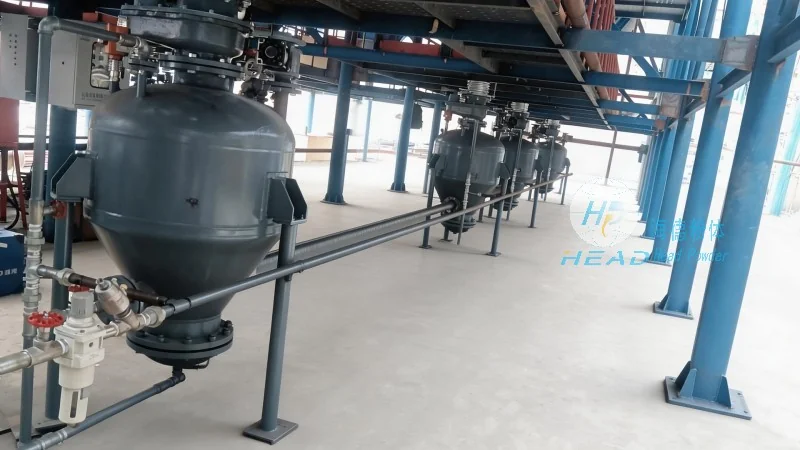
Pharmaceutical pneumatic conveying equipment offers several advantages over traditional methods such as bucket elevators or belt conveyors. These include improved hygiene and contamination control, as the system is enclosed and made of sanitary materials. It also provides flexibility in material handling, allowing for vertical, horizontal, or inclined transport. The system is compact and requires less floor space compared to other bulk material handling solutions. Additionally, it offers high efficiency in material transfer, reducing downtime and increasing overall production throughput.
Pharmaceutical pneumatic conveying equipment is widely used in various stages of pharmaceutical manufacturing, including raw material handling, intermediate processing, and final product packaging. It is particularly suitable for transporting sensitive materials like APIs and excipients, where product purity and consistency are paramount. The system can be integrated with other production equipment, such as mixers, blenders, and granulators, to form a seamless production line. This integration enhances operational efficiency and ensures that materials are handled in a controlled environment, meeting regulatory requirements for pharmaceutical manufacturing.
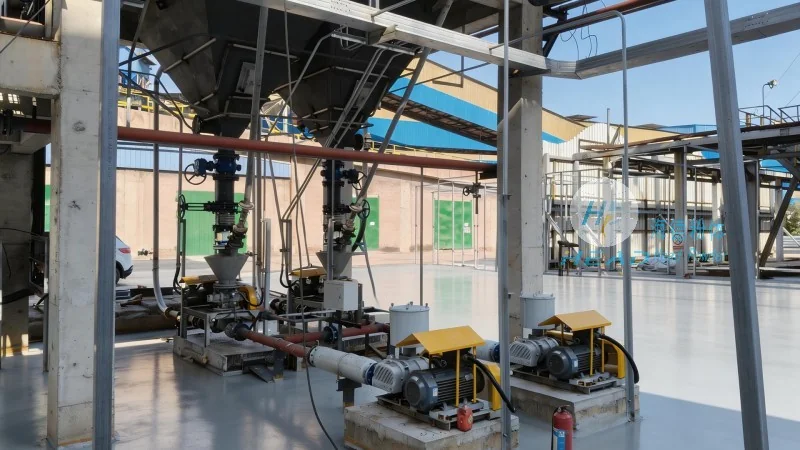
Proper maintenance of pharmaceutical pneumatic conveying equipment is crucial to ensure optimal performance and longevity. Regular cleaning and sanitization of the system components are essential to prevent contamination and maintain product quality. The air compressor and filters should be checked and replaced as needed to ensure consistent air quality. The conveying line and hopper should be inspected for wear and tear, and any blockages should be cleared promptly. Additionally, the system should be operated within the recommended pressure and flow ranges to avoid damage to components and ensure efficient material transfer.
Pharmaceutical bulk material pneumatic conveying equipment, developed by Shandong HeadPowder Engineering Co., Ltd., represents a sophisticated solution for the efficient and hygienic handling of bulk materials in pharmaceutical manufacturing. By understanding the operation process and working principles of this equipment, manufacturers can optimize their production processes, ensure product quality, and comply with regulatory standards. The system's advantages in hygiene, flexibility, and efficiency make it an essential component in modern pharmaceutical production lines.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top