HeadPowder, a leading engineering firm based in Shandong, China, specializes in the design, manufacturing, and installation of advanced pneumatic conveying systems tailored for the efficient handling of potash fertilizer materials. This article delves into the operational process and underlying working principles of such equipment, providing a comprehensive understanding of how these systems ensure reliable and efficient material transport in industrial settings.
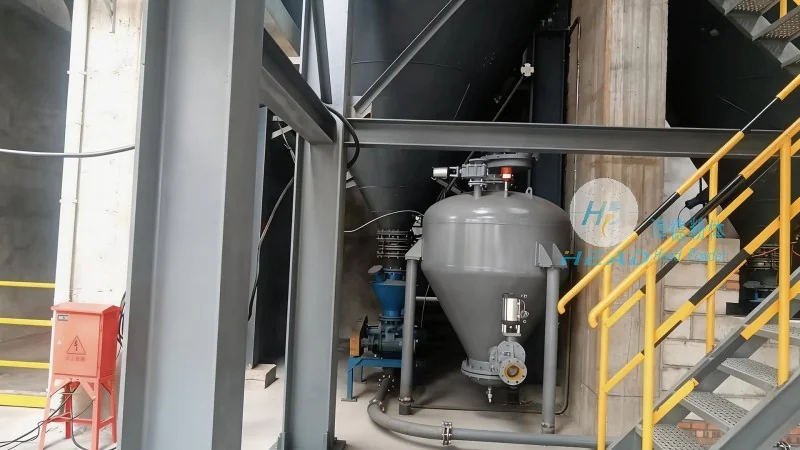
Potash fertilizer, a critical component in modern agriculture, often requires specialized handling due to its granular or powdery nature and varying moisture content. Traditional methods like belt conveyors or bucket elevators may face challenges such as material degradation, dust generation, and operational inefficiencies. Pneumatic conveying systems offer a solution by utilizing air or gas to transport bulk materials, providing a flexible, dust-free, and energy-efficient alternative. These systems are particularly advantageous for potash fertilizer, which demands precise control over particle flow and minimal contamination.
The core components of a pneumatic conveying system for potash fertilizer include the material hopper, feeder, air compressor, conveying pipeline, and discharge unit. Each component plays a vital role in the overall operation. The material hopper stores the potash fertilizer, ensuring a consistent feed to the feeder. The feeder, typically a rotary valve or screw feeder, regulates the flow of material into the conveying line, maintaining a steady supply without blockages. The air compressor generates the necessary pressure or vacuum to move the material through the pipeline. The conveying pipeline, made of durable materials like stainless steel or PVC, transports the material and air mixture. Finally, the discharge unit, such as a rotary valve or cyclone separator, collects the potash fertilizer at the destination, separating it from the air.
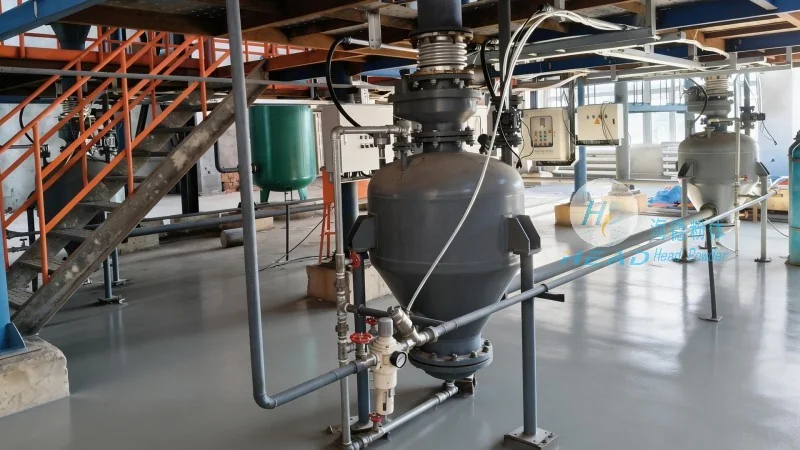
The operation of a pneumatic conveying system for potash fertilizer involves several sequential steps, each critical to the system's efficiency and reliability. The process begins with the loading of potash fertilizer into the material hopper. The feeder then starts, controlling the flow rate of the material into the conveying line. Simultaneously, the air compressor activates, generating the required air pressure or vacuum. The air and material mixture is then propelled through the pipeline, with the air velocity sufficient to carry the potash particles. As the mixture travels, it may encounter expansion or contraction sections in the pipeline, which help maintain consistent flow and prevent material settling. At the discharge end, the cyclone separator or rotary valve separates the potash fertilizer from the air, collecting the material in a storage bin or directly to the next processing stage. The air, now clean, is either recirculated or vented to the atmosphere, depending on the system design.
The working principle of pneumatic conveying equipment relies on the fundamental physics of fluid dynamics and particle motion. In a pressure system, the air compressor increases the pressure of the air, which is then introduced into the conveying pipeline. As the high-pressure air flows through the line, it entrains the potash fertilizer particles, creating a dense air-material mixture. The velocity of the air is maintained above the minimum transport velocity, ensuring that the particles remain suspended and are transported to the discharge point. In a vacuum system, the air compressor creates a vacuum, drawing the potash fertilizer and air mixture from the source to the destination. The key to efficient operation is balancing the air flow rate with the material feed rate, preventing either under- or over-transportation. The system's design, including pipeline diameter, length, and bends, is optimized to minimize pressure drop and energy consumption while ensuring reliable material transport.
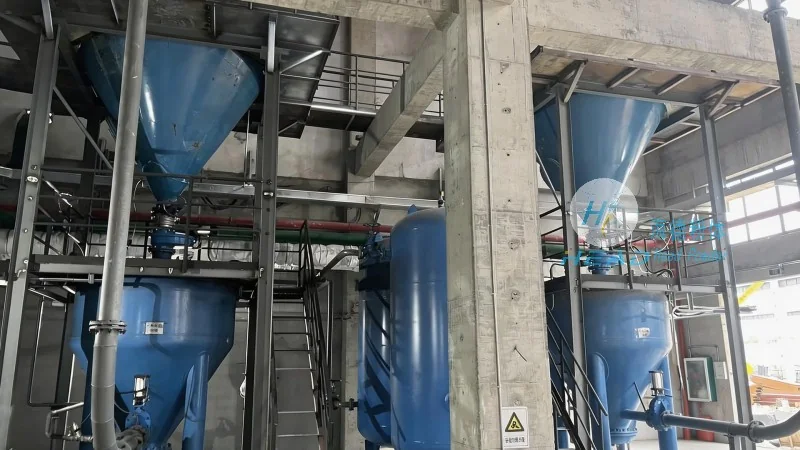
Pneumatic conveying systems offer several advantages when handling potash fertilizer. Firstly, they provide a dust-free environment, reducing health hazards and contamination risks associated with traditional methods. Secondly, the system is flexible, allowing for changes in material flow rates and destinations without major modifications. Thirdly, it minimizes material degradation by avoiding mechanical impact or excessive vibration. Additionally, the system can handle a wide range of potash fertilizer types, from granules to powders, with minimal adjustments. The energy efficiency of pneumatic conveying, particularly in pressure systems, makes it a cost-effective solution for large-scale operations. Finally, the enclosed system design enhances safety and environmental compliance, aligning with modern industrial standards.
Pneumatic conveying equipment for potash fertilizer is widely used in various industrial applications, including fertilizer production plants, storage facilities, and distribution centers. In fertilizer production, these systems efficiently transport raw potash materials from storage to processing units, ensuring a continuous supply for manufacturing. In storage facilities, they facilitate the transfer of potash fertilizer between silos or storage tanks, maintaining inventory levels and preventing material buildup. In distribution centers, the equipment enables the transport of finished potash fertilizer products to shipping containers or trucks, streamlining the logistics process. The reliability and efficiency of these systems contribute to increased productivity, reduced downtime, and improved overall operational performance in the fertilizer industry.
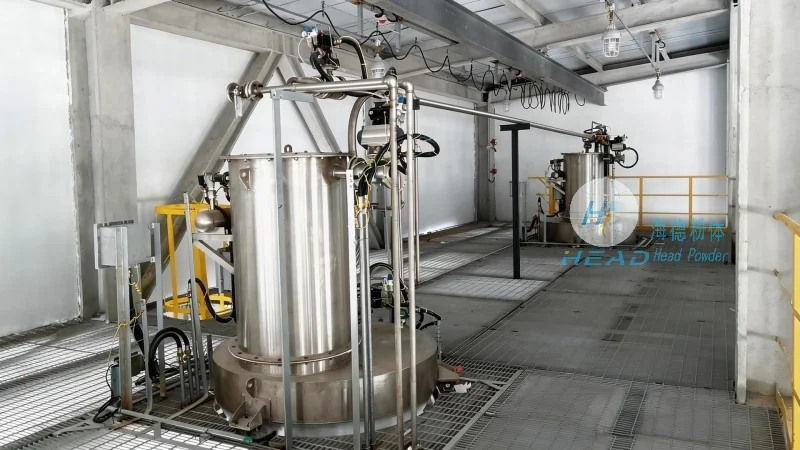
Proper maintenance is crucial to ensure the long-term performance and reliability of pneumatic conveying equipment for potash fertilizer. Regular inspections of the material hopper, feeder, and pipeline for blockages or wear are essential. The air compressor and its filters should be checked and maintained to prevent air leaks and ensure consistent pressure. The cyclone separator or discharge unit should be cleaned regularly to prevent material buildup and maintain efficient separation. Additionally, monitoring the air flow rate and pressure in the system helps identify any operational issues early, allowing for timely adjustments. Proper training of operators on the system's operation and maintenance is also vital to prevent accidents and ensure optimal performance. By adhering to these maintenance practices, HeadPowder ensures that its pneumatic conveying systems deliver consistent and reliable performance for potash fertilizer handling.
HeadPowder's pneumatic conveying equipment for potash fertilizer represents a sophisticated solution to the challenges of handling bulk materials in the agricultural industry. Through its detailed operational process and robust working principles, the system ensures efficient, dust-free, and reliable transport of potash fertilizer. With its advanced design and maintenance practices, this equipment contributes to improved productivity and operational efficiency in fertilizer production and distribution. As a leading engineering company based in Shandong, China, HeadPowder continues to innovate and provide tailored solutions that meet the evolving needs of the potash fertilizer industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top