Carbonaceous granular material pneumatic conveying systems are essential in industrial applications for the efficient transport of bulk materials. These systems utilize air or gas as the conveying medium to move particles from one location to another, offering advantages such as reduced labor costs, minimized material contamination, and improved process safety compared to traditional mechanical conveying methods.
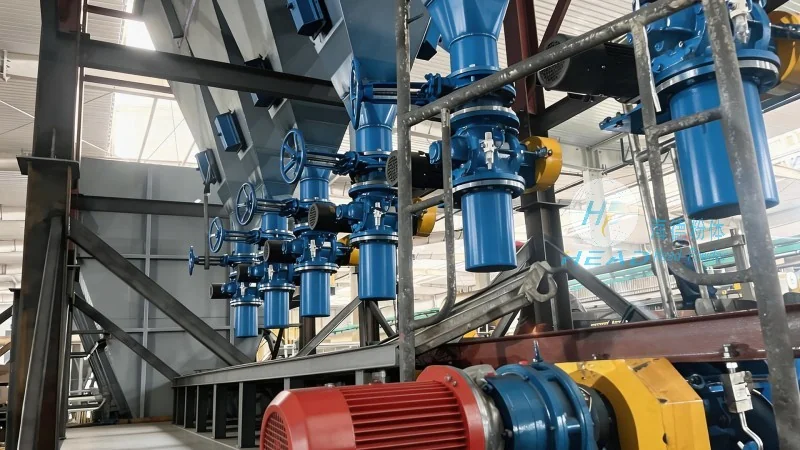
At the heart of a carbonaceous granular material pneumatic conveying system lies a series of interconnected components designed to facilitate the movement of particles. The primary components typically include a material hopper or feeder, a blower or compressor to generate the conveying air, a pipeline network for transporting the material, and a receiver or discharge hopper where the material is deposited. Additionally, systems may incorporate accessories like filters, cyclones, and pressure regulators to ensure optimal performance and maintain air quality.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading provider of pneumatic conveying solutions specializing in the design, manufacturing, and installation of systems tailored to the unique needs of carbonaceous granular materials. With a strong presence in China, particularly in Shandong, the company leverages decades of industry experience to deliver reliable and efficient conveying systems that meet the demands of various industrial sectors.
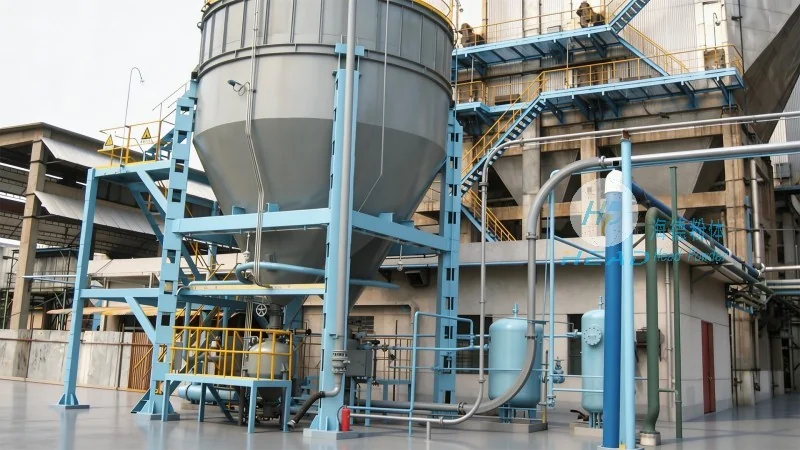
The operation of a carbonaceous granular material pneumatic conveying system begins with the loading of material into the hopper. The feeder then controls the flow rate of the granular material into the pipeline. Simultaneously, the blower or compressor generates a flow of air, which is introduced into the pipeline at a specific pressure and velocity. As the air moves through the pipeline, it entrains the carbonaceous particles, forming a dense phase or dilute phase conveying stream depending on the system design. The material is then transported to the receiver, where the air is separated from the particles, often through a cyclone or filter system. The separated air is then discharged, while the material is collected in the receiver for further processing or storage.
The working principle of a carbonaceous granular material pneumatic conveying system is based on the fundamental physics of fluid dynamics and particle motion. The system operates by creating a pressure differential between the hopper and the receiver. The blower or compressor supplies the necessary pressure to overcome the resistance of the pipeline and the weight of the material. The air velocity is critical; it must be sufficient to lift and transport the particles without causing excessive wear on the system components. The conveying process can be categorized into two main types: dense phase conveying, which uses lower air velocities and higher material concentrations, and dilute phase conveying, which employs higher air velocities and lower material concentrations. Both methods are effective for carbonaceous granular materials, with the choice depending on factors such as material properties, system length, and required flow rates.
Implementing a pneumatic conveying system for carbonaceous granular materials offers several key advantages. Firstly, it eliminates the need for mechanical components like belts, chains, or buckets, reducing maintenance requirements and extending the system's lifespan. Secondly, the system provides a hygienic and clean environment, preventing contamination of the material during transport, which is particularly important for food or pharmaceutical applications. Thirdly, pneumatic conveying systems can handle a wide range of material sizes and shapes, including fine powders and irregularly shaped particles. Additionally, these systems offer flexibility in layout, allowing for horizontal, vertical, or inclined transport paths as needed. Finally, the energy efficiency of modern pneumatic conveying systems, combined with advanced control technologies, ensures optimal performance while minimizing operational costs.
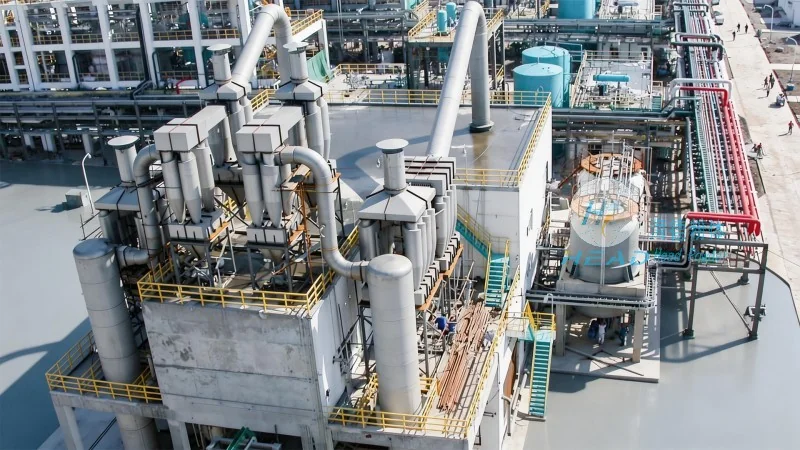
Carbonaceous granular material pneumatic conveying systems are widely used across various industrial sectors. In the carbon industry, these systems are crucial for transporting raw materials such as coal, coke, and graphite. In the chemical industry, they facilitate the transport of carbon-based powders and additives. The food and beverage industry also benefits from these systems for handling ingredients like cocoa powder or coffee granules. Furthermore, in the pharmaceutical sector, pneumatic conveying ensures the safe and sterile transport of active pharmaceutical ingredients (APIs) and other powders. The versatility and reliability of these systems make them indispensable in modern industrial operations.
Carbonaceous granular material pneumatic conveying systems represent a sophisticated and efficient solution for the transport of bulk materials. By understanding the operational process and working principles, industries can leverage these systems to enhance productivity, improve material handling, and reduce operational costs. With the expertise of companies like Shandong HeadPowder Engineering Co., Ltd., businesses can implement tailored pneumatic conveying solutions that meet their specific requirements, ensuring reliable and sustainable material transport in various industrial applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top