Organic fertilizer granular materials are widely used in agricultural applications due to their effectiveness in soil conditioning and nutrient supply. The efficient handling and transportation of these materials are crucial for maintaining productivity in fertilizer production and distribution. Pneumatic conveying systems offer a reliable and flexible solution for moving organic fertilizer granules from production sites to storage or processing facilities. This article provides an overview of the operation process and working principles of such systems, highlighting key components and their functions. Shandong HeadPowder Engineering Co., Ltd. specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for organic fertilizer applications.
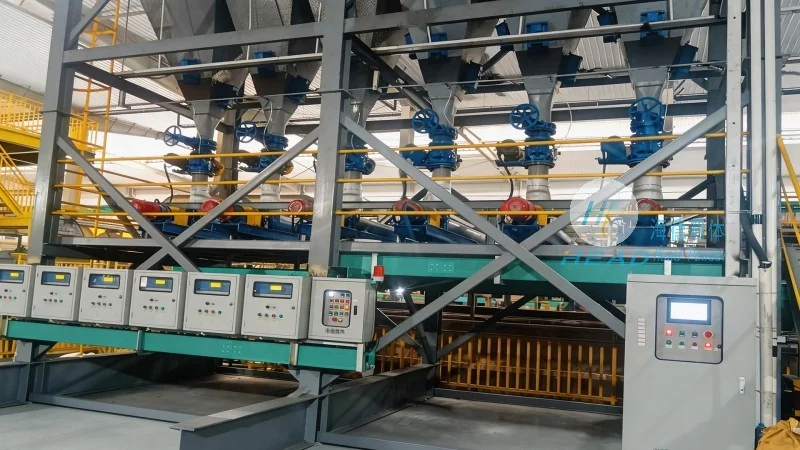
The pneumatic conveying system for organic fertilizer granular materials typically consists of several essential components. The primary elements include a material hopper, a conveyor line (either positive or negative pressure), a rotary airlock valve, a filter and dust collector, and a discharge outlet. Each component plays a critical role in ensuring the smooth and efficient transport of the fertilizer granules.
The material hopper is designed to store the organic fertilizer granules before they are fed into the conveying system. It is equipped with a feeder, such as a screw or rotary valve, which controls the flow rate of the material into the conveyor line. The feeder ensures a consistent supply of granules, preventing blockages and maintaining system efficiency. The conveyor line is the core of the system, responsible for transporting the granules through the air stream. It can operate under positive pressure (where air is forced through the material) or negative pressure (where air is drawn through the material). The choice of pressure type depends on factors like the material's characteristics, distance to be conveyed, and system design requirements.
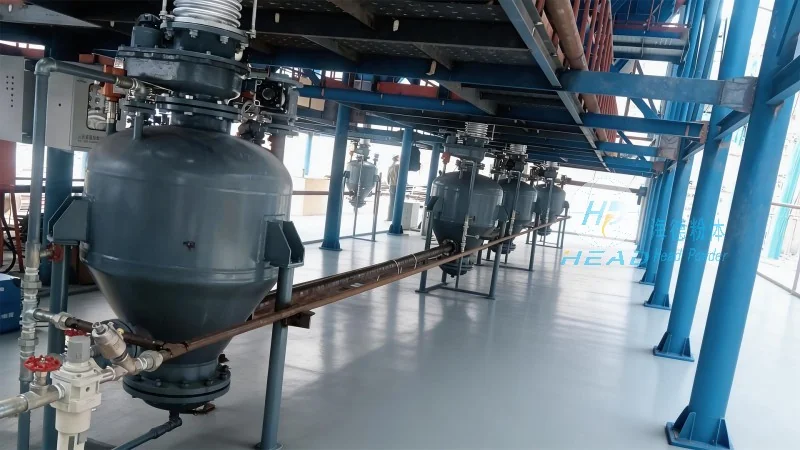
The rotary airlock valve is installed at the discharge end of the conveyor line. Its function is to regulate the flow of granules from the conveying line to the discharge outlet, preventing backflow and maintaining a steady flow rate. This component is crucial for controlling the output and ensuring that the material is discharged smoothly without clogging. The filter and dust collector are essential for maintaining air quality and system safety. As the air passes through the conveying line, it may carry fine particles or dust from the fertilizer granules. The filter captures these particles, preventing them from being released into the environment or causing equipment damage. The collected dust is typically stored in a separate container for disposal or reuse.
The operation process of a pneumatic conveying system for organic fertilizer granular materials involves several sequential steps. First, the organic fertilizer granules are loaded into the material hopper. The feeder then starts to rotate, feeding the granules into the conveyor line at a controlled rate. Simultaneously, the air compressor or fan generates the necessary air pressure or vacuum, depending on the system configuration. The air is introduced into the conveyor line, creating a flow that moves the granules along the line.
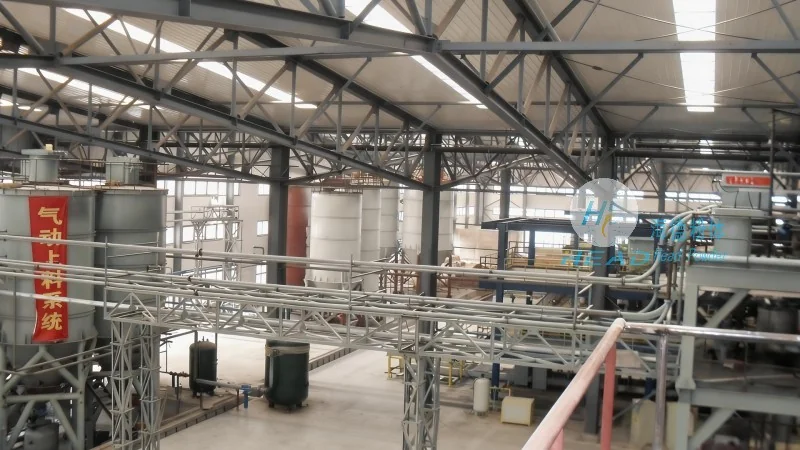
As the granules travel through the conveyor line, they are carried by the air stream. The design of the conveyor line, including the pipe diameter and length, affects the air velocity and pressure required to move the material efficiently. Proper air velocity is essential to prevent material deposition or blockages. The rotary airlock valve at the discharge end regulates the flow of granules out of the system, ensuring a consistent discharge rate. The filtered air is then released from the system, typically through a vent or exhaust system.
During operation, the system continuously monitors key parameters such as air pressure, flow rate, and material level. These parameters are adjusted as needed to maintain optimal performance. For example, if the material flow rate decreases, the feeder speed may be increased to restore the desired flow. Similarly, if the air pressure drops, the compressor output may be adjusted to maintain the required pressure. The filter and dust collector are also monitored to ensure they are functioning correctly and to prevent clogging.
The working principle of a pneumatic conveying system for organic fertilizer granular materials is based on the movement of material particles by an air stream. In positive pressure systems, the air is forced through the material, creating a high-pressure environment that propels the granules forward. The air velocity must be sufficient to overcome the gravitational force and friction between the granules and the conveyor line. In negative pressure systems, the air is drawn through the material, creating a low-pressure environment that pulls the granules along the line. Both systems rely on the principle of fluidization, where the air stream lifts the granules and transports them through the system.
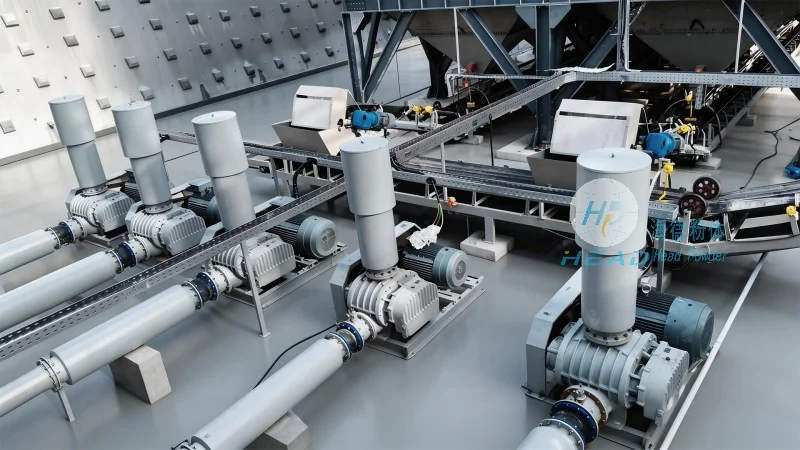
The efficiency of the pneumatic conveying system depends on several factors, including the particle size and density of the organic fertilizer granules, the air velocity, and the system design. Larger or denser granules may require higher air velocities or more powerful air compressors to ensure efficient transport. The conveyor line's length and diameter also impact the system's performance, as longer or narrower lines may increase pressure drop and require more energy. Proper system sizing and design are critical to achieving optimal performance and minimizing operational costs.
Pneumatic conveying systems offer several advantages for handling organic fertilizer granular materials. One of the primary benefits is the ability to transport materials over long distances without the need for intermediate storage or transfer points. This reduces the risk of material degradation and contamination, as the granules are not exposed to the environment during transport. Additionally, pneumatic conveying systems are flexible and can be easily integrated with existing production lines or storage facilities.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top