Phosphates powder pneumatic conveying equipment is a critical component in industrial material handling systems, designed to efficiently transport phosphates powders through a pressurized or vacuum system. This equipment plays a vital role in various industries, including chemical manufacturing, food processing, and mining, where the reliable and safe movement of powders is essential for operational efficiency and product quality.
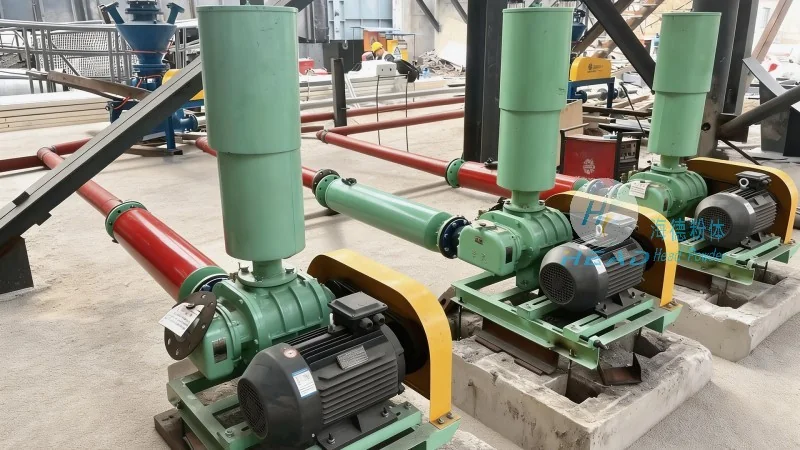
Phosphates powder pneumatic conveying systems utilize air or gas to move powders from one location to another. These systems are typically composed of several key components, including a hopper for material storage, a conveyor line, a control system, and a dust collection unit. The design of these systems is tailored to handle the specific properties of phosphates powders, such as particle size, moisture content, and flowability, ensuring optimal performance and minimal material degradation.
The core components of a phosphates powder pneumatic conveying system include the material hopper, which stores the phosphates powder and provides a controlled feed to the system. The hopper is equipped with a feeder mechanism, such as a rotary valve or a screw feeder, that regulates the flow of powder into the conveyor line. The conveyor line itself is a flexible or rigid tube that transports the powder using air pressure or suction. A blower or vacuum pump generates the necessary airflow, while a filter and dust collector ensure that the air is cleaned and returned to the system or released safely. Additionally, a control panel manages the operation of the system, allowing for adjustments to flow rate, pressure, and other parameters to maintain consistent performance.
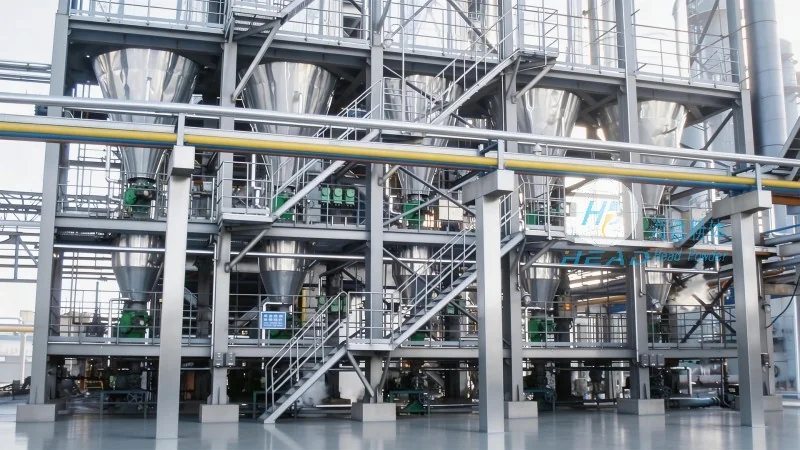
The operation of phosphates powder pneumatic conveying equipment involves a series of steps to ensure efficient and safe material transport. The process begins with the loading of phosphates powder into the hopper. The feeder then starts to discharge the powder into the conveyor line at a controlled rate. Simultaneously, the blower or vacuum pump generates the required airflow, which propels the powder particles through the system. As the powder travels through the conveyor line, it may encounter various components, such as bends or filters, which help maintain the flow and prevent blockages. The material is then discharged at the receiving end, where it is collected in a storage bin or directly into a processing unit. Throughout the operation, the control system monitors key parameters, such as pressure, flow rate, and temperature, to ensure that the system operates within safe and optimal conditions.
The working principle of phosphates powder pneumatic conveying equipment is based on the principles of fluid dynamics and particle transport. In a pressurized system, the blower increases the air pressure above the powder in the hopper, creating a pressure differential that forces the powder to flow into the conveyor line. The air and powder mixture travels through the system, with the air providing the necessary momentum to move the particles. In a vacuum system, the vacuum pump creates a negative pressure that draws the powder from the hopper into the conveyor line. The air velocity within the system is carefully controlled to ensure that the powder particles are entrained without causing excessive wear or degradation. The design of the system, including the size of the conveyor line and the air velocity, is optimized to balance the forces acting on the powder particles, such as gravity, drag, and lift, to achieve efficient transport.
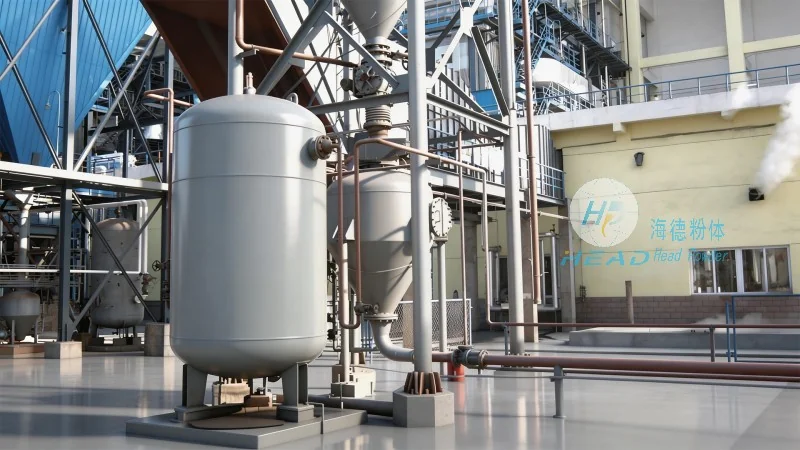
Phosphates powder pneumatic conveying equipment offers several advantages over traditional bulk material handling methods, such as belt conveyors or bucket elevators. These systems are highly flexible, allowing for the transport of powders over long distances and around obstacles. They also provide a closed system, which helps prevent dust emissions and contamination, ensuring product purity and compliance with environmental regulations. Additionally, pneumatic conveying systems are capable of handling a wide range of powder properties, including fine powders, cohesive powders, and powders with high moisture content. This makes them suitable for various applications, including the transport of phosphates powders in chemical plants, food processing facilities, and mining operations.
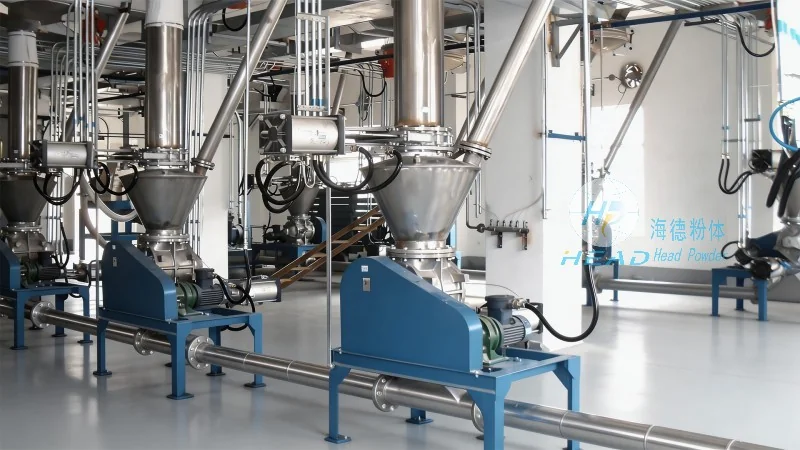
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading manufacturer and supplier of industrial material handling equipment, including phosphates powder pneumatic conveying systems. With headquarters located in Shandong, China, the company has established itself as a trusted partner in the industry, providing high-quality, reliable equipment tailored to the specific needs of its clients. Headpowder's commitment to innovation and customer satisfaction has enabled it to serve a diverse range of industries, from chemical manufacturing to food processing, and has earned the company a reputation for excellence in the field of material handling technology.
In conclusion, phosphates powder pneumatic conveying equipment is a sophisticated and essential tool for the efficient and safe transport of powders in various industrial applications. The operation process and working principle of these systems are designed to optimize performance, minimize material degradation, and ensure compliance with safety and environmental standards. As a leading provider of such equipment, Shandong HeadPowder Engineering Co., Ltd. continues to advance the technology and deliver solutions that meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top