Shandong HeadPowder Engineering Co., Ltd., a leading enterprise in material handling technology, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for corn kernels. This article provides a comprehensive overview of the operational process and working principles of such systems, emphasizing their efficiency, reliability, and the technical innovations that make them suitable for modern agricultural and industrial applications.
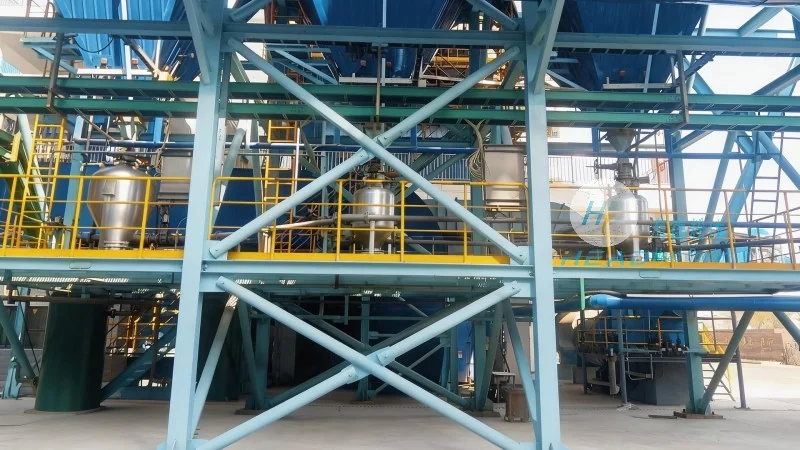
The corn kernels pneumatic conveying system comprises several critical components that collaborate to achieve effective material transport. These include the material hopper for storage, the air compressor or blower to generate the necessary air pressure, the pipeline network for conveying the material, and the control system to regulate the flow. Each component is engineered to work in harmony, ensuring smooth and consistent operation. The hopper is typically constructed from durable materials to withstand the weight and abrasion of corn kernels, while the air compressor is selected based on the required flow rate and pressure. The pipeline network may vary in diameter and length depending on the application, with bends and fittings strategically placed to maintain the air velocity and prevent material deposition.
The fundamental principle of the system is the use of air movement to suspend and transport solid particles. When the air compressor is activated, it creates a pressure differential between the inlet and outlet of the pipeline. Corn kernels are fed into the hopper and then drawn into the pipeline by the moving air. The air velocity is carefully controlled to ensure that the kernels are carried without causing excessive wear or degradation. This method of conveying is particularly effective for corn kernels due to their size (typically 3-10 mm) and density (around 0.7-0.8 g/cm³), which allow for efficient suspension in the air stream. The system operates under either positive or negative pressure, depending on the specific requirements of the application.
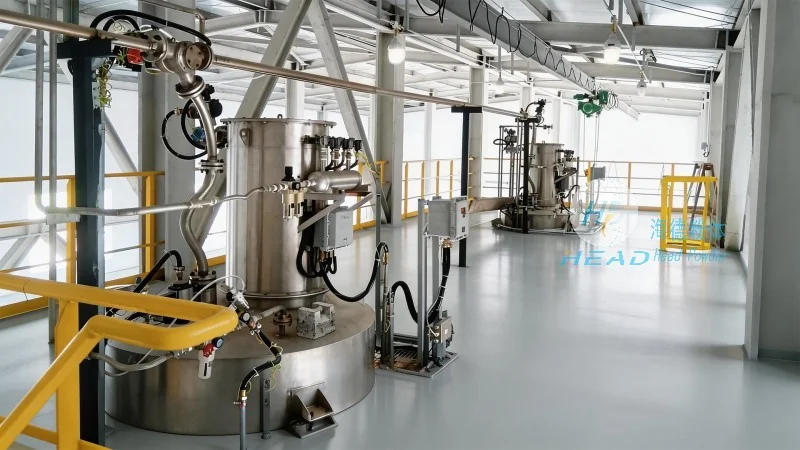
The operational process of the corn kernels pneumatic conveying system can be broken down into a series of sequential steps. First, the corn kernels are loaded into the storage hopper. The control system then activates the air compressor, which begins to generate the required air pressure. As the air flows through the pipeline, it creates a vacuum at the inlet, drawing the corn kernels into the system. The material travels through the pipeline network, which may include filters to remove dust or debris and bends to change the direction of the flow. At the destination, the corn kernels are discharged into a receiving container. The entire process is automated, with the control system continuously monitoring parameters such as air pressure, flow rate, and material level to ensure optimal performance. Any deviations from the set parameters are immediately detected and corrected, minimizing downtime and maintaining consistent output.
Compared to traditional methods like belt conveyors or manual handling, the corn kernels pneumatic conveying system offers several significant advantages. One of the key benefits is the ability to transport materials over long distances with minimal labor and space requirements. The system is also highly flexible, allowing for changes in the conveying route without major modifications. Additionally, it reduces the risk of material contamination and damage, which is crucial for maintaining the quality of corn kernels. The automated nature of the system enhances safety and consistency, making it ideal for large-scale operations. Furthermore, the system can handle a wide range of particle sizes and densities, making it versatile for various applications.
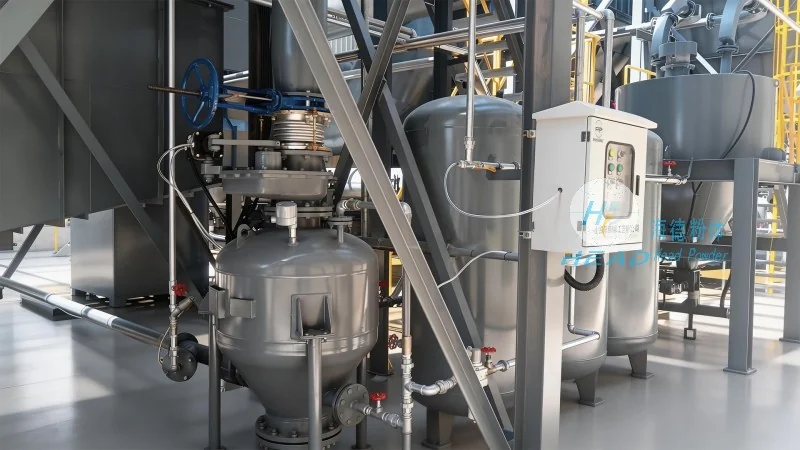
Shandong HeadPowder Engineering Co., Ltd.'s corn kernels pneumatic conveying systems are widely utilized across multiple industries, including food processing, animal feed manufacturing, and agricultural storage. In food processing plants, the system efficiently transports corn kernels from storage to processing lines, ensuring a continuous supply of raw materials for products like cornmeal, corn syrup, and animal feed. In animal feed production, the system helps in blending different ingredients, including corn, with precision and speed, improving the nutritional value and consistency of the final product. Agricultural storage facilities benefit from the system's ability to move large quantities of corn kernels between storage silos and processing units, enhancing overall operational efficiency and reducing manual handling efforts.
To ensure the long-term reliability and performance of the corn kernels pneumatic conveying system, regular maintenance is essential. The air compressor and blower should be checked for proper lubrication and air filter cleanliness to prevent dust accumulation and maintain optimal air flow. The pipeline network should be inspected for any signs of wear, corrosion, or blockages, which can affect the flow rate and increase energy consumption. The control system should be calibrated regularly to maintain accurate monitoring of operational parameters, such as air pressure, flow rate, and material level. Common issues such as reduced flow or increased air pressure may indicate blockages or worn components, which should be addressed promptly to avoid system downtime. Regular cleaning of the hopper and pipeline is also recommended to prevent material buildup and maintain the system's efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top