Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for the transportation and handling of diatomite powder. The diatomite powder material handling system equipment is designed to ensure efficient and reliable operation in industrial applications. This equipment plays a crucial role in the processing and distribution of diatomite, a natural sedimentary rock known for its high porosity and excellent filtering properties. The system integrates various components to facilitate the seamless movement of diatomite powder from storage to processing units, enhancing overall operational efficiency. With a focus on durability and performance, the equipment is engineered to withstand the abrasive nature of diatomite powder and operate in demanding industrial environments.
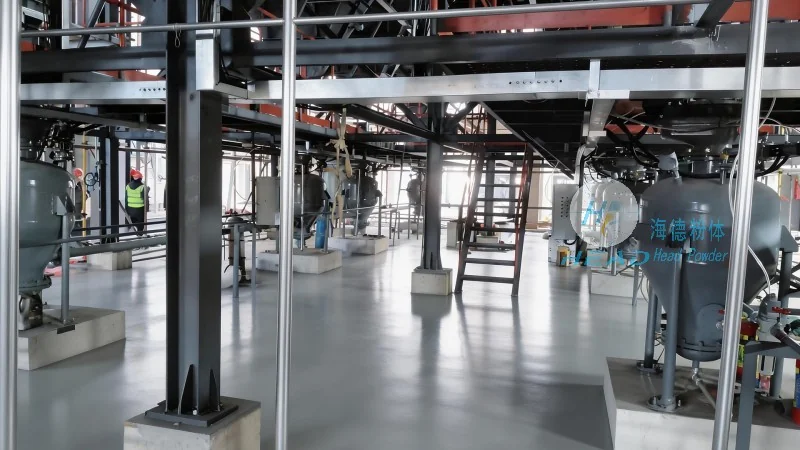
The diatomite powder material handling system typically consists of several core components that work in tandem to achieve optimal performance. These components include feeders, conveyors, storage silos, and control systems. Each component is engineered to handle the unique characteristics of diatomite powder, such as its fine particle size (ranging from 0.1 to 100 microns) and low bulk density (approximately 0.2 to 0.5 g/cm³). The feeders are responsible for regulating the flow of powder from the storage silo to the conveyor system, ensuring a consistent and controlled feed rate. The conveyors, often in the form of belt or screw conveyors, transport the diatomite powder through the system with minimal loss or degradation. The storage silos provide a large capacity for bulk storage, allowing for continuous operation even during maintenance or processing adjustments. The control systems integrate sensors and automation technology to monitor and adjust the flow rates, ensuring the system operates within safe and efficient parameters. Additionally, the system includes dust collection and filtration systems to maintain a clean working environment and comply with environmental regulations.
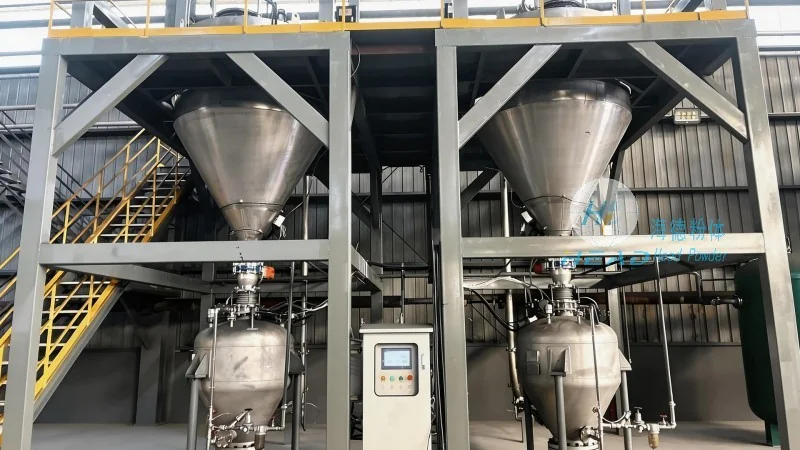
The operation process of the diatomite powder material handling system begins with the loading of diatomite into the storage silo. The powder is then discharged from the silo into the feeder, which regulates the flow based on the system's requirements. The feeder transfers the powder to the conveyor, which transports it to the processing or packaging units. Throughout this process, the system maintains a consistent flow rate, minimizing the risk of clogging or material buildup. The control system continuously monitors the pressure, flow rate, and temperature to ensure the diatomite powder remains in optimal condition. In case of any anomalies, such as blockages or overflows, the system automatically triggers alarms or safety mechanisms to prevent damage to the equipment or loss of material. The entire operation is designed to be automated, reducing the need for manual intervention and improving operational safety. The system also includes backup mechanisms, such as emergency stop buttons and redundant sensors, to enhance reliability and prevent downtime.
The working principle of the diatomite powder material handling system is based on the principles of material flow and mechanical transport. The system utilizes gravity and mechanical force to move the diatomite powder from one point to another. The storage silo stores the diatomite in bulk, and the feeder uses a rotating mechanism, such as a screw or paddle, to discharge the powder at a controlled rate. The conveyor system, such as a belt conveyor, uses friction between the belt and the powder to move it along the path. The control system uses level sensors in the silo and flow sensors in the feeder to adjust the feeder speed dynamically. This closed-loop control ensures that the system operates efficiently and prevents overfilling or underfilling. The equipment is also designed with sealing and gasketing to minimize dust leakage, and the conveyor belts are made of materials resistant to abrasion from the diatomite powder. The overall working principle is to create a seamless and continuous flow of diatomite powder, from storage to processing, with minimal energy consumption and maximum efficiency. The system's design minimizes the need for manual handling, reducing the risk of dust exposure and improving workplace safety.
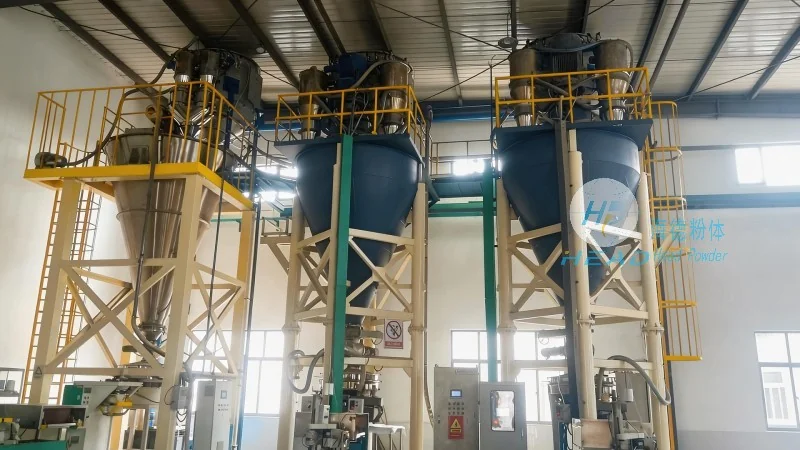
The diatomite powder material handling system equipment offers several benefits for industrial applications. The primary benefit is the improved efficiency in the transportation and handling of diatomite powder, which reduces labor costs and increases production throughput. The system's automated control features enhance operational safety by minimizing human error and preventing accidents. The dust control measures also contribute to a healthier working environment, reducing the risk of respiratory issues associated with fine powder handling. The equipment is widely used in industries such as filtration, cosmetics, and food processing, where diatomite is a key raw material. The system's ability to handle large volumes of diatomite powder makes it suitable for both small-scale and large-scale production facilities. Additionally, the modular design of the system allows for easy expansion or modification to meet changing production needs. The consistent quality of the powder delivered by the system ensures that downstream processes, such as filtration or packaging, operate smoothly and produce high-quality products. For example, in the filtration industry, the system ensures that diatomite powder is delivered to filter presses in a uniform manner, improving the quality of the final filter cake. In the cosmetics industry, the consistent flow of diatomite powder to mixing units ensures that the final products have a consistent texture and quality.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top