HeadPowder, a leading manufacturer in the field of material handling solutions, specializes in providing advanced equipment for efficient material transfer. The automatic tonne bag feeding material conveying equipment is a key product designed to streamline the process of handling bulk materials from tonne bags into processing lines. This equipment is crucial for industries such as food, chemicals, and pharmaceuticals where precise and reliable material feeding is essential for maintaining production efficiency and product quality.
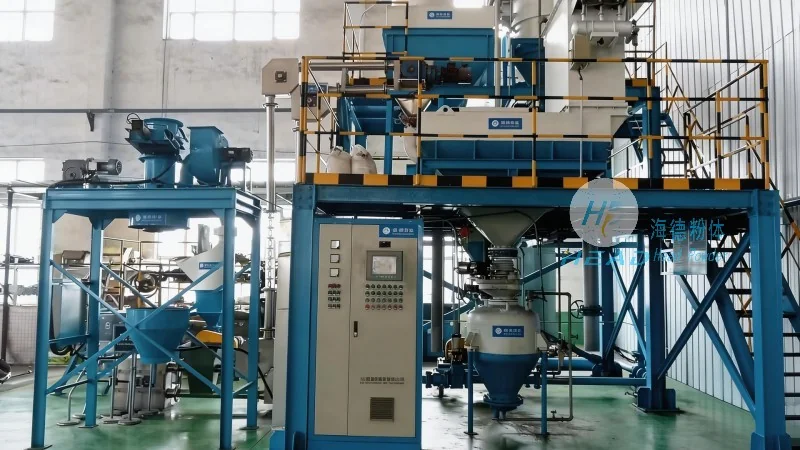
HeadPowder, the brand name used by Shandong HeadPowder Engineering Co., Ltd., is dedicated to delivering high-quality engineering solutions. The company is headquartered in Shandong, China, and has established itself as a trusted provider of material handling equipment. With a focus on innovation and customer satisfaction, HeadPowder ensures that its products meet the stringent requirements of various industrial applications.
The operation of the automatic tonne bag feeding material conveying equipment involves several key steps that ensure smooth and continuous material transfer. The process begins with the placement of a tonne bag on the equipment's loading platform. The system then uses a combination of mechanical and automated controls to open the bag and discharge its contents into a hopper or conveyor system. The equipment is equipped with sensors and control mechanisms that monitor the bag opening process, ensuring that the material is released evenly and without blockages. Once the bag is emptied, the system automatically closes the bag opening mechanism and prepares for the next bag, minimizing downtime and increasing overall throughput.
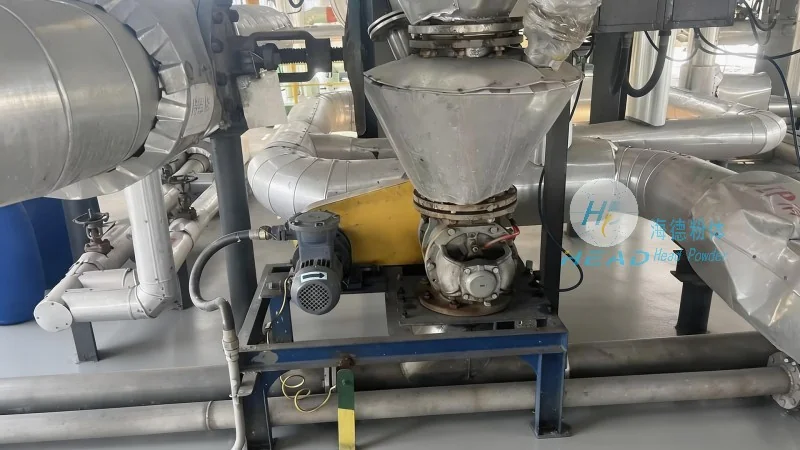
The working principle of the automatic tonne bag feeding material conveying equipment is based on a combination of mechanical action and automated control systems. The core components include a bag opening device, a discharge chute, a hopper, and a conveyor system. The bag opening device typically uses a hydraulic or pneumatic actuator to cut or tear the bag open, allowing the material to flow out. The discharge chute is designed to guide the material from the bag into the hopper, where it is then transferred to the conveyor system for further processing. The control system, which may include PLC (Programmable Logic Controller) technology, coordinates the operation of all components, ensuring that the process runs smoothly and efficiently. Sensors are used to detect the presence of a bag, the level of material in the hopper, and any blockages, providing feedback to the control system to adjust the operation as needed. This integrated approach ensures that the equipment operates reliably and with minimal human intervention.
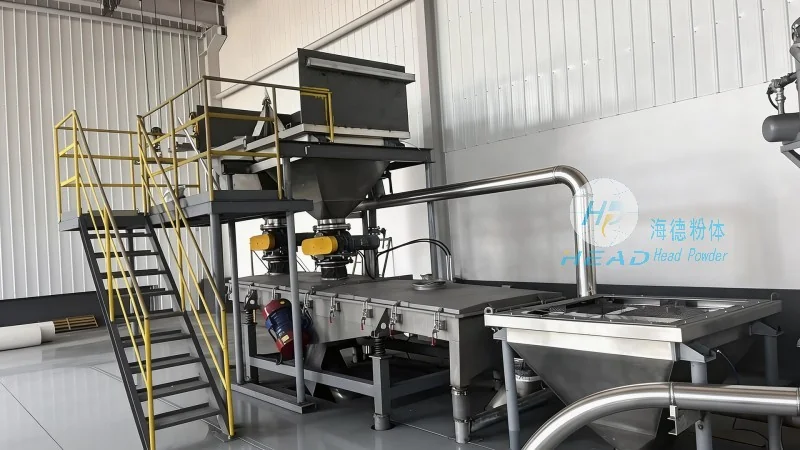
The automatic tonne bag feeding material conveying equipment offers several advantages that make it an ideal choice for industrial applications. These include high efficiency in material handling, reduced labor costs due to automated operation, and improved safety by minimizing human contact with bulk materials. The equipment is also designed for easy maintenance and cleaning, ensuring long-term reliability and low operational costs. Additionally, the system can be customized to meet specific production requirements, such as different bag sizes or material types, providing flexibility for various industrial needs.
The automatic tonne bag feeding material conveying equipment is widely used in various industries where bulk materials are handled from tonne bags. In the food industry, it is used for feeding ingredients like flour, sugar, and grains into processing lines. In the chemical industry, it handles raw materials such as powders and granules, ensuring safe and efficient transfer. The pharmaceutical industry also benefits from this equipment, as it provides a hygienic and controlled environment for handling active ingredients and other materials. Overall, the equipment enhances productivity and ensures consistent quality in material handling processes across different sectors.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top