Wheat flour bulk material conveying systems are critical components in the food processing industry, particularly for operations involving the efficient and safe transportation of wheat flour from storage silos or processing units to various destinations such as packaging lines or blending facilities. The operation process and working principle of these systems are designed to ensure high efficiency, minimal product degradation, and compliance with industry standards for hygiene and safety.
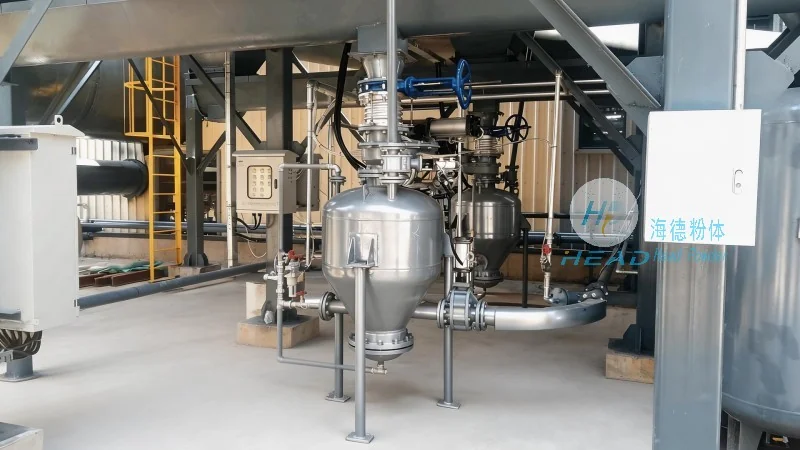
Wheat flour bulk material conveying systems typically consist of several key components, including hoppers, conveyors (like screw conveyors, pneumatic conveyors, or bucket elevators), control systems, and safety mechanisms. Each component plays a vital role in the overall operation, working in concert to move wheat flour through the system with precision and reliability. The system's design is tailored to handle the unique characteristics of wheat flour, such as its fine particle size, hygroscopic nature, and susceptibility to bridging or caking in storage silos.
The primary components of a wheat flour bulk material conveying system include the material hopper, which serves as the initial storage and feeding point for the wheat flour. The hopper is designed with a sloped bottom to facilitate the flow of material and prevent clogging. Adjacent to the hopper is the conveyor system, which can vary in type depending on the specific application. For example, screw conveyors are commonly used for horizontal or slight incline transport due to their ability to handle fine powders without significant segregation. Pneumatic conveyors, on the other hand, use air pressure to transport wheat flour in a closed system, offering advantages in terms of dust control and flexibility in routing.
Bucket elevators are another common component, especially for vertical transport, as they can efficiently lift wheat flour from lower to higher levels while maintaining product integrity. The control system, often integrated with sensors and variable frequency drives (VFDs), monitors the flow rate, pressure, and other parameters to ensure smooth operation and prevent overloading or underflow. Safety mechanisms, such as emergency stop buttons and overload protection, are also integral to the system to protect both personnel and equipment.
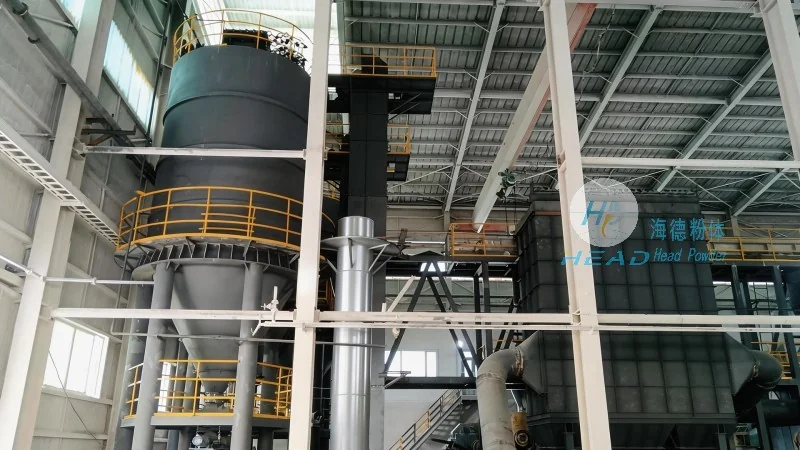
The operation process of a wheat flour bulk material conveying system begins with the loading of wheat flour into the hopper. The material is then fed into the conveyor system, which transports it to the next stage of the process. For horizontal transport, screw conveyors rotate, pushing the flour forward through a rotating helical screw. The speed of the screw can be adjusted to control the flow rate, ensuring consistent delivery to downstream equipment. Pneumatic conveyors, in contrast, use compressed air to create a pressure differential that draws the flour into the conveying line. The air and flour mixture is then transported to the discharge point, where the air is separated and the flour is collected.
During vertical transport, bucket elevators operate by lifting buckets attached to a chain or belt. As the buckets move upward, they scoop up wheat flour from the lower hopper and discharge it into the upper hopper or directly into the processing line. The speed of the elevator is controlled to maintain a steady flow, preventing material from falling back or causing blockages. In both horizontal and vertical systems, the control system continuously monitors the process, adjusting parameters as needed to maintain optimal performance.
The working principle of wheat flour bulk material conveying systems is based on the principles of fluidization and mechanical transport. In pneumatic systems, the air flow creates a fluidized state where the wheat flour particles are suspended and transported. This method is particularly effective for fine powders like wheat flour, as it minimizes particle segregation and reduces the risk of caking. Mechanical systems, such as screw and bucket elevators, rely on the physical movement of the conveying mechanism to push or lift the material. The design of these mechanisms is critical to prevent material degradation, as excessive friction or impact can cause the flour to become compacted or lose its quality.
Hygiene and safety are paramount in wheat flour processing, and the conveying system's design reflects this. Materials used in the construction of hoppers, conveyors, and control systems are typically made from stainless steel or other food-grade materials to prevent contamination. The system is also equipped with cleaning mechanisms, such as CIP (Clean-in-Place) systems, to ensure thorough sanitation between batches. Additionally, dust control measures, including sealed enclosures and filtration systems, are implemented to protect both the product and the environment from airborne flour particles.
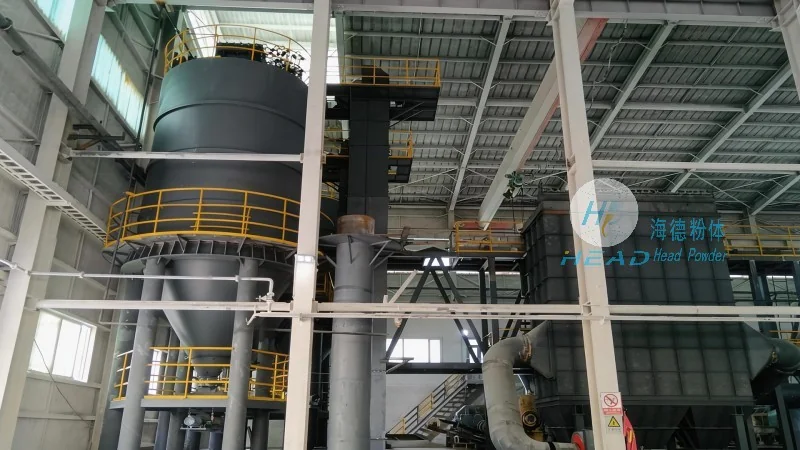
The efficiency of a wheat flour bulk material conveying system is influenced by several factors, including the design of the hopper, the type of conveyor, and the control system. Proper hopper design, with appropriate slope and anti-caking measures, minimizes the risk of material bridging and ensures a consistent feed rate. The choice of conveyor type depends on the specific application, with screw conveyors being ideal for horizontal transport and bucket elevators for vertical lifting. The control system's ability to adjust parameters in real-time enhances the system's adaptability to varying production demands.
Maintenance is a critical aspect of ensuring the long-term performance of the conveying system. Regular inspections of the hopper, conveyor, and control components are necessary to identify and address issues such as wear and tear, clogging, or sensor malfunctions. Lubrication of moving parts, cleaning of the conveying line, and calibration of the control system are all part of routine maintenance. By adhering to a regular maintenance schedule, the system's efficiency and reliability are maintained, reducing downtime and ensuring consistent product quality.
Wheat flour bulk material conveying systems are essential for the efficient and safe processing of wheat flour. The operation process, which involves loading, conveying, and discharge, is designed to handle the unique characteristics of wheat flour while maintaining product integrity. The working principle, based on fluidization and mechanical transport, ensures that the material is moved with minimal degradation and maximum efficiency. With proper design, maintenance, and control, these systems contribute significantly to the overall productivity and quality of wheat flour processing operations. As a leading provider in this field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing high-quality conveying systems tailored to the specific needs of the food processing industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top