Efficient material handling is a critical aspect of industrial operations, especially when dealing with bulk materials like coke powder. The dust removal coke powder pneumatic conveying system is a sophisticated solution designed to transport these materials safely and effectively. This system combines advanced engineering with robust design to ensure optimal performance in various industrial settings.
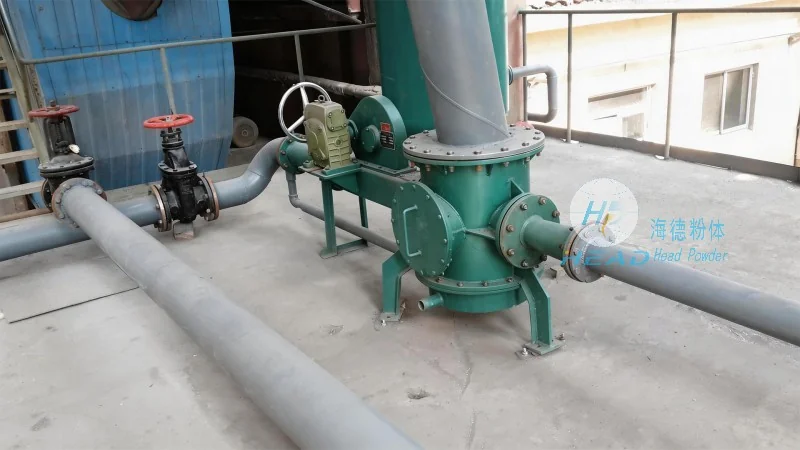
The dust removal coke powder pneumatic conveying system is engineered to handle coke powder, a material often associated with dust and potential health hazards. By integrating dust removal mechanisms, this system not only transports the material but also maintains a clean and safe working environment. The system is tailored to meet the specific needs of industrial applications, ensuring reliability and efficiency in material handling processes.
At the core of the dust removal coke powder pneumatic conveying system are several key components that work in harmony to achieve the desired results. These components include the hopper, which serves as the material storage and feeding unit; the air compressor, responsible for generating the necessary air pressure; the dust filter, which captures and removes airborne particles; and the conveying pipeline, which transports the material from the source to the destination. Each component plays a vital role in the overall operation of the system, contributing to its effectiveness and safety.
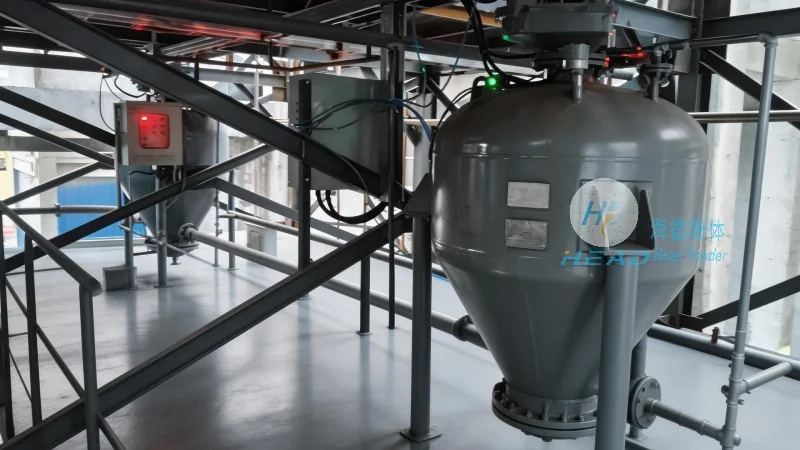
The operation of the dust removal coke powder pneumatic conveying system follows a systematic process that ensures smooth and continuous material transport. The process begins with the material being fed into the hopper from a storage silo or bulk container. The material then flows into the conveying pipeline through the hopper's outlet, where it is mixed with compressed air. The air, carrying the coke powder particles, is then directed through the pipeline to the receiving hopper or storage area. The dust filter is integrated into the system to capture any fine particles that may be released during the conveying process, ensuring that the air discharged is clean and free from contaminants. This process is typically automated, with sensors and controls monitoring the flow rate and pressure to maintain optimal performance.
The working principle of the dust removal coke powder pneumatic conveying system is based on the principles of fluid dynamics and air pressure. The system utilizes positive pressure or negative pressure (or a combination of both) to move the material through the pipeline. In positive pressure systems, the air compressor generates high-pressure air that forces the material through the pipeline. The air and material mixture is then separated at the receiving end, with the material being discharged and the air being filtered and recycled. In negative pressure systems, a vacuum is created at the receiving end, drawing the material and air through the pipeline. The dust filter is crucial in both systems as it removes the fine coke powder particles from the air, preventing contamination and ensuring compliance with environmental regulations. The system's design allows for flexible operation, adapting to different material characteristics and conveying distances.
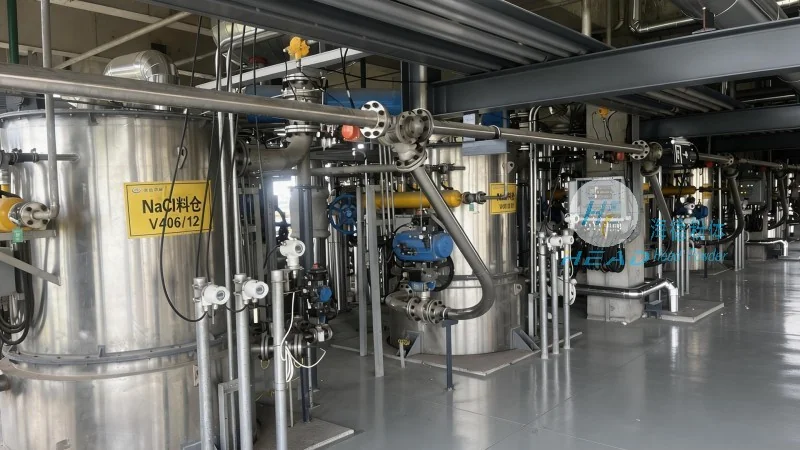
The dust removal coke powder pneumatic conveying system offers numerous benefits that make it an ideal choice for industrial applications. One of the primary advantages is the enhanced safety provided by the integrated dust removal mechanism, which reduces the risk of respiratory issues and other health hazards associated with coke powder dust. Additionally, the system minimizes material loss and waste, as the dust filter captures fine particles that would otherwise be lost during transport. The automated operation of the system also reduces labor costs and improves efficiency, allowing for continuous and reliable material handling. Furthermore, the system's compact design and modular components make it easy to install and maintain, reducing downtime and maintenance costs. The ability to handle varying material flow rates and conveying distances also adds to its versatility, making it suitable for a wide range of industrial processes.
HeadPowder, a leading manufacturer of industrial material handling systems, specializes in designing and manufacturing dust removal coke powder pneumatic conveying systems. With years of experience in the industry, the company has developed a reputation for quality, reliability, and innovation. The company's headquarters is located in Shandong, China, where it operates a state-of-the-art manufacturing facility equipped with advanced technology and skilled personnel. HeadPowder's team of engineers and technicians is dedicated to providing customized solutions that meet the specific needs of its clients, ensuring that each system is tailored to the unique requirements of the application. The company adheres to strict quality control standards and uses only the highest quality materials and components in its products, ensuring long-term performance and durability. HeadPowder's commitment to customer satisfaction and technical excellence has made it a trusted partner for industrial facilities worldwide.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top