High-pressure bin pump systems represent a sophisticated solution for material handling and transportation in various industrial applications. These systems are designed to efficiently transport bulk materials over long distances or across challenging terrains, leveraging pneumatic technology to achieve reliable and consistent performance. The technology behind high-pressure bin pumps is rooted in the principles of fluid dynamics and pressure differentials, enabling the movement of materials from storage bins or silos to processing units, storage facilities, or other destinations with minimal operational complexity.
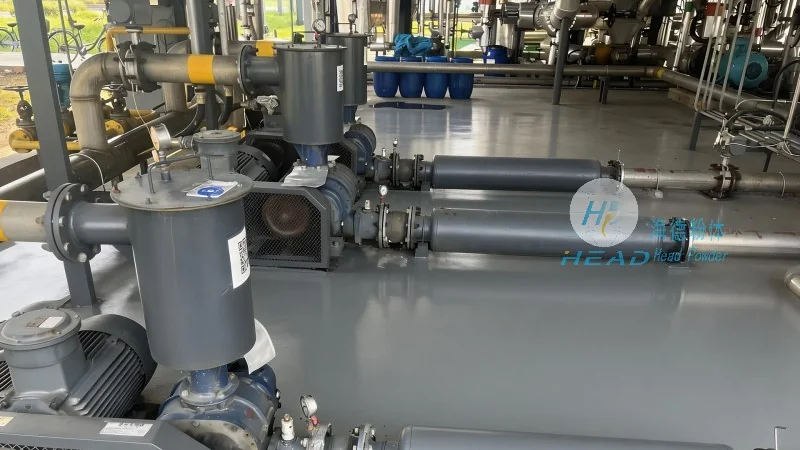
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer and supplier of advanced material handling equipment. With headquarters located in Shandong, China, the company specializes in the design, development, and production of high-quality pneumatic conveying systems tailored to meet the diverse needs of industrial sectors. HeadPowder's commitment to innovation, quality, and customer satisfaction has established it as a trusted partner in the material handling industry, providing reliable solutions for clients worldwide.
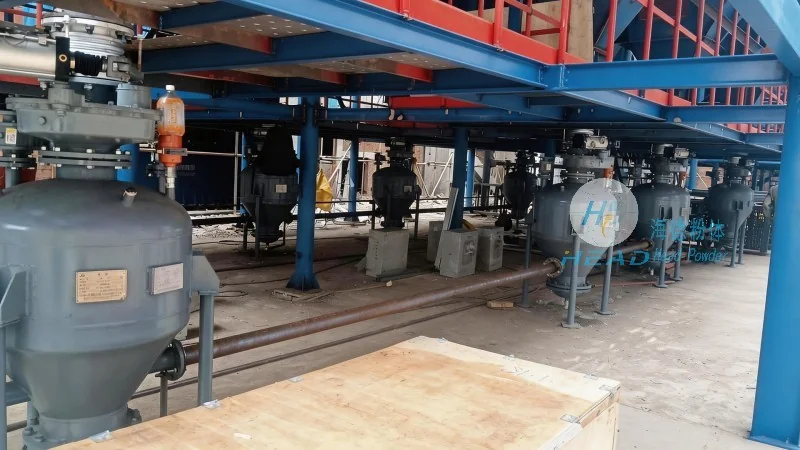
The core principle of high-pressure bin pump systems involves the use of compressed air or other gases to create a pressure differential that propels bulk materials through a pipeline network. In a typical setup, the material is first fed into a storage bin or hopper, where it is then pneumatically conveyed through a series of pipes to the destination point. The high-pressure pump, often a positive displacement type, generates the necessary pressure to overcome resistance in the pipeline and ensure the continuous flow of material. This process eliminates the need for mechanical components like conveyors or elevators, reducing maintenance requirements and enhancing operational efficiency.
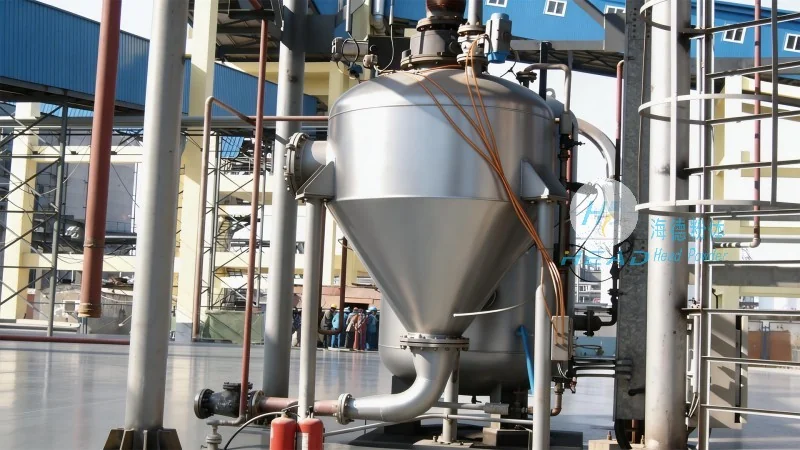
High-pressure bin pump systems are particularly well-suited for applications that demand high throughput, long-distance transport, or the handling of abrasive or corrosive materials. The equipment is designed to operate in a variety of industrial environments, including chemical processing plants, food and beverage facilities, mining operations, and construction sites. Key characteristics include: high material transport capacity, ability to handle diverse material types (from powders to granules), low maintenance requirements, and the capacity to operate over extended distances without significant pressure loss. Additionally, these systems offer flexibility in terms of layout and integration with existing infrastructure, making them a versatile choice for modern industrial operations.
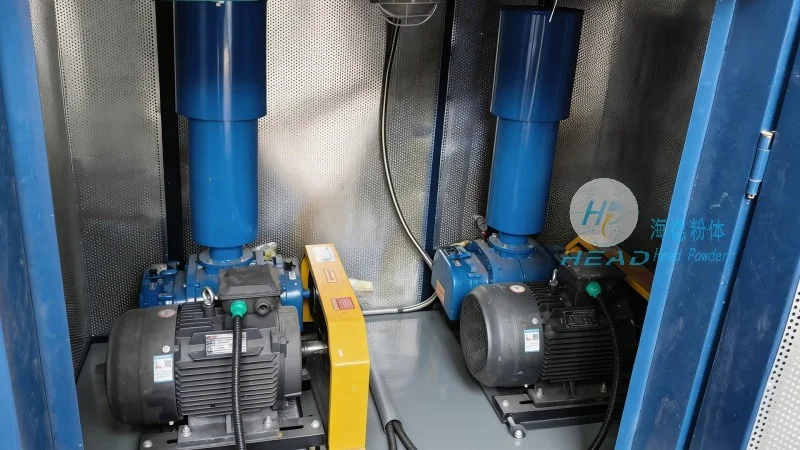
Implementing high-pressure bin pump technology offers several advantages over traditional material handling methods. The primary benefit is the reduction in labor costs and operational downtime, as the system operates automatically with minimal human intervention. Furthermore, the pneumatic conveying process minimizes material degradation, ensuring that the quality of the transported product is preserved. In industrial settings, these systems are commonly used for transporting raw materials to production lines, moving finished products to storage areas, or transferring waste materials for disposal. The adaptability of high-pressure bin pumps allows them to be integrated into existing workflows, enhancing overall productivity and efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top