HeadPowder Engineering, a leading provider in material handling solutions, specializes in the design and implementation of pneumatic conveying systems for various industrial applications. This article explores the fundamental principles behind the pneumatic conveying of potassium carbonate, a critical chemical widely used in industries such as pharmaceuticals, food processing, and chemical manufacturing. Understanding the mechanics and operational characteristics of this technology is essential for optimizing material transport efficiency and ensuring safe, reliable processing in industrial settings.
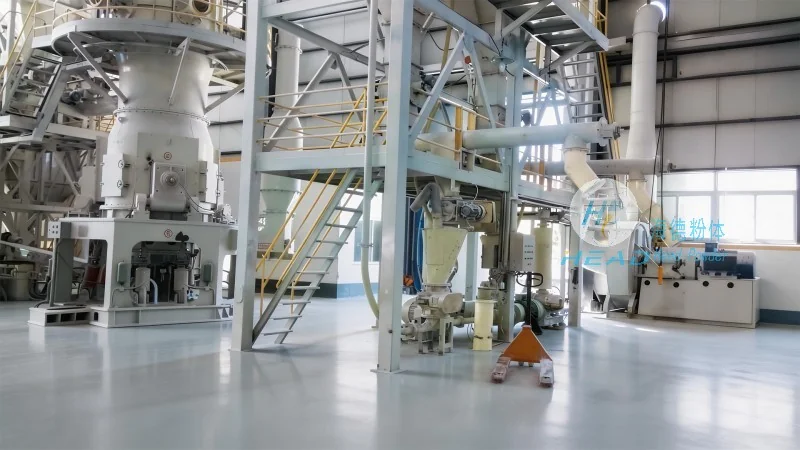
The pneumatic conveying of potassium carbonate relies on the movement of solid particles through a pipeline using a gas stream, typically air or a combination of air and other gases. Two primary modes of operation dominate in industrial applications: positive pressure and negative pressure systems. Positive pressure systems generate air pressure at the conveying source, pushing the material through the pipeline, while negative pressure systems create a vacuum at the receiving end, drawing material from the source. For potassium carbonate, which is often handled in bulk quantities, positive pressure systems are commonly preferred due to their ability to handle high material loads and maintain consistent flow rates. The system typically consists of a hopper, a rotary airlock valve, a conveying line, and a receiver. The hopper stores the potassium carbonate, and the rotary airlock valve controls the flow of material into the conveying line. The conveying line transports the material to the receiver, where it is collected. The air stream, often heated to prevent moisture absorption or caking, ensures that the material remains in a fluidized state, minimizing blockages and ensuring smooth transport. The design of the conveying line, including the diameter and length, is critical to maintaining the required air velocity to keep the particles suspended and prevent deposition. Proper air velocity, typically ranging from 20 to 30 meters per second for fine powders like potassium carbonate, is essential to achieve efficient and reliable transport. The system also incorporates filters and cyclones to separate the air from the material, ensuring that the air is clean and the material is free from contaminants. This separation process is crucial for maintaining product purity and preventing equipment damage from abrasive particles.
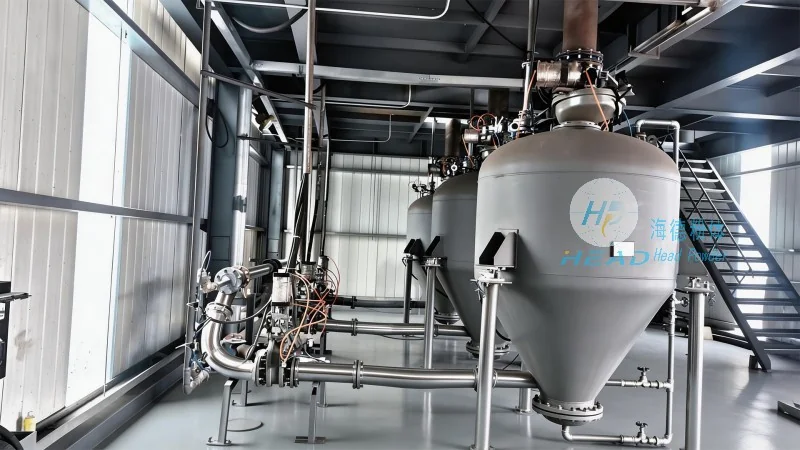
Potassium carbonate is widely used in diverse industrial sectors, and the pneumatic conveying system is tailored to meet the specific demands of each application. In pharmaceutical manufacturing, for instance, the system must adhere to stringent hygiene and contamination control standards. The use of positive pressure systems with enclosed hoppers and sealed conveying lines helps maintain a clean environment, preventing cross-contamination and ensuring product safety. The ability to handle fine powders without agglomeration is particularly important in this sector, as any clumping can affect the quality of the final product. In food processing, the system is designed to be fully sanitary, with materials such as stainless steel and food-grade components used throughout. The air stream is often filtered to remove any particles that could contaminate the food product, and the conveying process is monitored to prevent any temperature fluctuations that might affect the product's shelf life. The chemical industry also utilizes potassium carbonate in various processes, such as the production of fertilizers and detergents. Here, the system is designed to handle larger quantities of material and operate under higher pressures. The robust construction of the conveying line and the use of wear-resistant materials ensure that the system can withstand the abrasive nature of the material and the high operational pressures. Another key advantage of pneumatic conveying is its flexibility in handling different material characteristics. Potassium carbonate can vary in particle size, density, and moisture content, and the system can be adjusted to accommodate these variations. For example, if the material is more cohesive or has higher moisture content, the air velocity can be increased or the conveying line diameter adjusted to maintain optimal flow. The system's ability to handle changes in material properties without significant downtime or maintenance makes it a preferred choice for many industrial applications. Additionally, the system offers advantages in terms of space efficiency and integration with existing processes. Unlike traditional mechanical conveying systems, which require extensive space for hoppers, chutes, and conveyor belts, pneumatic conveying systems can be installed in compact areas, making them ideal for facilities with limited space. The integration of the system with existing production lines is also straightforward, as the conveying line can be connected directly to the source and receiver, minimizing the need for additional equipment or modifications to the existing infrastructure. This flexibility in installation and integration reduces the overall cost and time required for implementation, making it a cost-effective solution for many industrial operations.
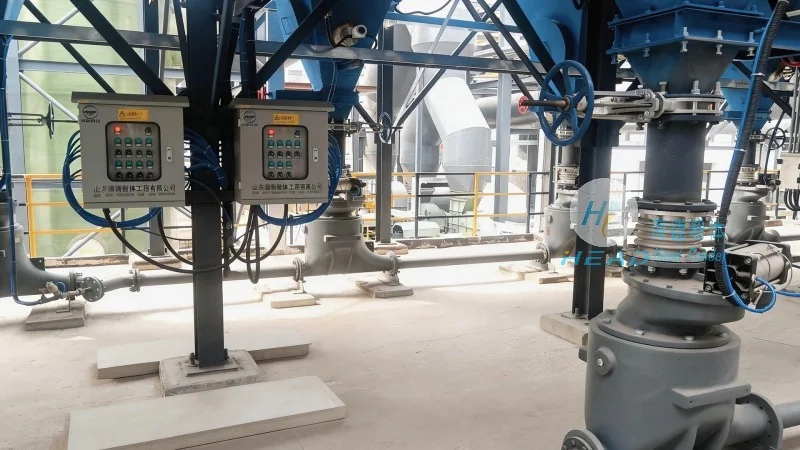
HeadPowder Engineering, with its headquarters in Shandong, China, has established itself as a trusted provider of advanced material handling solutions. The company specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored to the unique needs of clients in various industries. With a team of experienced engineers and technicians, HeadPowder Engineering leverages cutting-edge technology and rigorous testing protocols to ensure that each system meets the highest standards of performance and reliability. The company's expertise lies in understanding the specific challenges of handling materials like potassium carbonate, including their physical properties, handling requirements, and industry-specific regulations. By conducting thorough analyses of the material characteristics and operational requirements, the company develops customized solutions that optimize material transport efficiency, reduce downtime, and enhance overall process safety. HeadPowder Engineering's commitment to quality is evident in its use of high-quality materials and components, such as stainless steel for the conveying line and advanced control systems for monitoring and adjusting the conveying process. The company also provides comprehensive after-sales support, including maintenance, repair, and technical assistance, to ensure that the systems operate at peak performance throughout their lifecycle. This comprehensive approach to service and support has earned the company a reputation for reliability and customer satisfaction among its clients. In conclusion, the pneumatic conveying of potassium carbonate is a sophisticated technology that offers significant advantages in terms of efficiency, flexibility, and safety. By understanding the core principles and application scenarios of this technology, industrial facilities can optimize their material handling processes and improve overall operational performance. HeadPowder Engineering, with its expertise and commitment to quality, is well-positioned to provide the necessary solutions to meet the evolving needs of the industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top