Pneumatic conveying is a critical technology in the pharmaceutical industry for transporting bulk materials such as powders, granules, and other fine substances. This method leverages compressed air or other gases to move materials through a closed system, offering advantages like contamination control, energy efficiency, and scalability. Understanding the principles and application scenarios of this technology is essential for optimizing pharmaceutical manufacturing processes and ensuring compliance with industry standards.
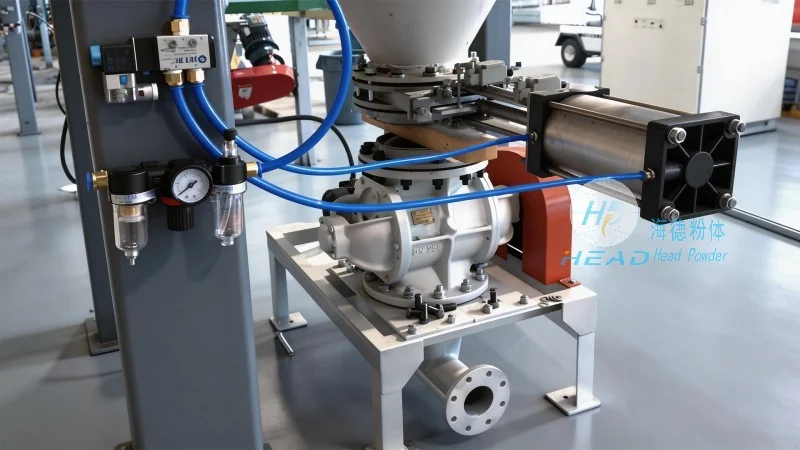
The core principle of pneumatic conveying involves creating a pressure differential between the inlet and outlet of the system. By introducing compressed air into the material hopper or feeder, the material is entrained and carried through the pipeline to the destination. There are primarily two types of pneumatic conveying systems: pressure and vacuum. Pressure systems operate by forcing air and material through the pipeline, while vacuum systems use a vacuum to draw material from the source. The choice between these systems depends on factors like material properties, distance, and system layout. For pharmaceutical applications, pressure systems are often preferred due to their ability to maintain positive pressure, which helps prevent contamination from external sources. The system typically includes components like a feeder, a conveying line, a separator, and a receiver. The feeder ensures a consistent flow of material, the conveying line transports it, the separator separates the material from the air, and the receiver collects the material. Each component plays a vital role in maintaining the efficiency and safety of the process.
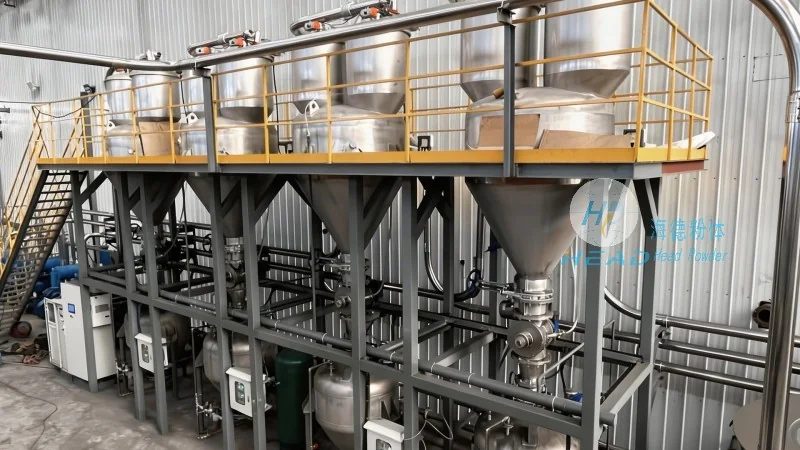
Pneumatic conveying is widely used in various stages of pharmaceutical manufacturing, from raw material handling to finished product packaging. In raw material handling, it is used to transport raw powders from storage silos to processing units, ensuring a clean and efficient transfer. During the manufacturing process, it can be employed to move intermediate products between different production lines, facilitating seamless workflow. In the final stages, it is used to transfer finished products from the production line to packaging areas, maintaining product integrity and preventing cross-contamination. The technology is particularly suitable for materials that are sensitive to moisture, temperature, or air exposure, as the closed system minimizes environmental impact. Additionally, pneumatic conveying can handle materials with varying particle sizes and densities, making it versatile for different pharmaceutical applications. For example, in the production of APIs (Active Pharmaceutical Ingredients), pneumatic conveying is used to transport raw materials to the reaction vessels, ensuring precise dosing and consistent quality. In the manufacturing of solid dosage forms, it helps in transferring granules or powders to the tablet press or capsule filling machines, enhancing production efficiency.
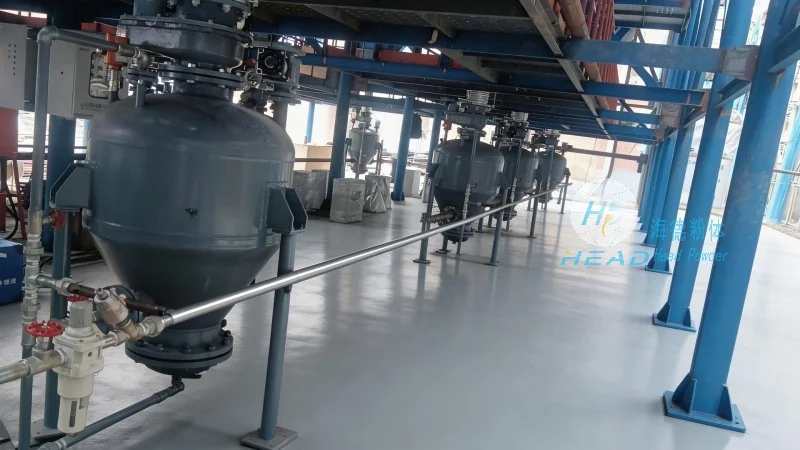
Implementing pneumatic conveying systems in pharmaceutical manufacturing offers several key advantages. Firstly, it provides excellent contamination control. The closed system prevents the entry of external contaminants, which is crucial for maintaining product purity and meeting regulatory requirements. Secondly, it enhances operational efficiency. By automating the material transfer process, it reduces manual handling, minimizes downtime, and increases overall productivity. Thirdly, it offers flexibility in system design. Pneumatic conveying systems can be customized to fit different plant layouts and material requirements, allowing for scalability as production needs change. Fourthly, it improves safety. The enclosed system reduces the risk of dust explosions and exposure to hazardous materials, creating a safer working environment. Lastly, it contributes to cost savings. By optimizing material handling and reducing waste, it helps lower operational costs over time. These advantages make pneumatic conveying a preferred choice for pharmaceutical manufacturers seeking to improve their production processes and ensure compliance with industry standards.
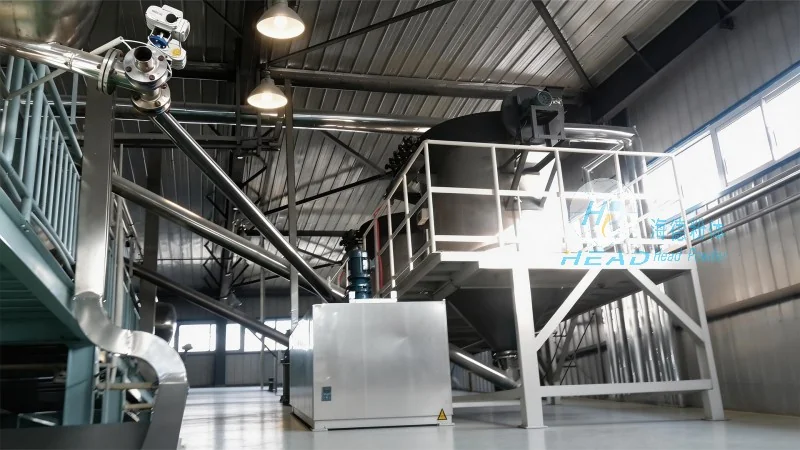
Shandong HeadPowder Engineering Co., Ltd., operating under the brand name headpowder, specializes in the design, manufacturing, and installation of pneumatic conveying systems tailored for the pharmaceutical industry. With a focus on precision engineering and adherence to GMP (Good Manufacturing Practice) standards, the company provides comprehensive solutions that meet the unique demands of pharmaceutical manufacturing. The company’s headquarters is located in Shandong, China, where it leverages advanced technology and experienced engineering teams to deliver high-quality products and services. By combining expertise in material handling and pharmaceutical industry knowledge, headpowder ensures that its pneumatic conveying systems are not only efficient but also compliant with regulatory requirements. The company’s commitment to quality and customer satisfaction has established it as a trusted partner in the pharmaceutical sector, helping manufacturers optimize their material handling processes and enhance overall production efficiency.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top