The pneumatic conveying of materials at dust extraction stations is a critical technology in modern industrial processes, enabling the efficient transport of bulk materials while maintaining air quality and operational safety. This article explores the fundamental principles behind this technology and highlights the key characteristics of its working scenarios, providing insights into how such systems are applied in real-world industrial settings.
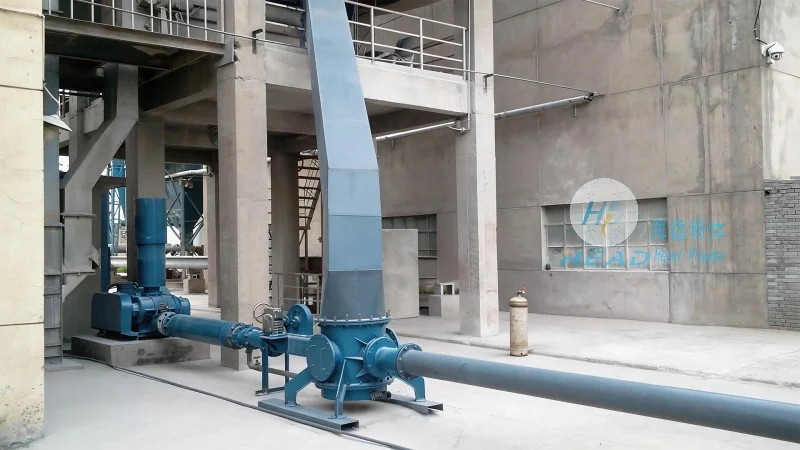
Pneumatic conveying operates by using a stream of air to transport solid particles through a pipeline. The process can be categorized into two main types: positive pressure and negative pressure systems. In positive pressure systems, air is forced through the pipeline, carrying the material forward. Conversely, negative pressure systems use suction to draw material into the pipeline. The choice between these systems depends on factors such as material properties, distance, and environmental requirements. The core principle involves creating a pressure differential that propels or pulls the material along the conveying line, ensuring consistent and reliable transport.
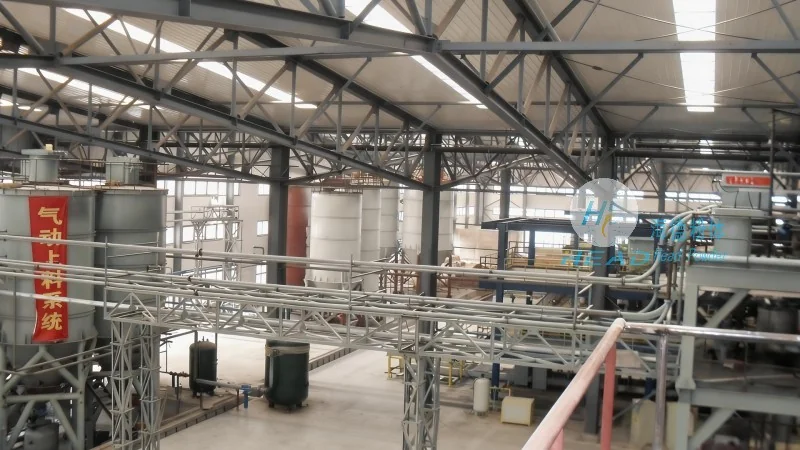
The working characteristics of pneumatic conveying systems vary significantly based on the specific application and operational conditions. For instance, in dust extraction stations, the system must handle fine particles and potentially abrasive materials, which can affect the design of the conveying line and the type of air flow. The velocity of the air stream is a critical parameter, as it must be sufficient to overcome the gravitational and frictional forces acting on the particles. Additionally, the system's ability to handle varying material loads and maintain consistent flow rates is essential for maintaining the efficiency of the dust extraction process.
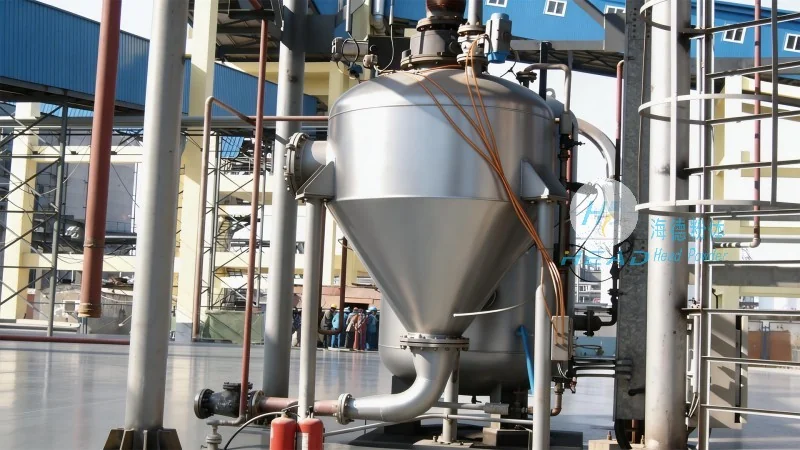
Pneumatic conveying is widely used in dust extraction stations for tasks such as transporting collected dust from filters to storage silos or for feeding raw materials into processing equipment. The benefits of this technology include reduced labor costs, minimized material loss, and improved safety by eliminating the need for manual handling of bulk materials. Furthermore, the system's ability to operate in a closed loop helps maintain air quality and prevents dust contamination in the surrounding environment. In industrial settings, these advantages translate into higher overall productivity and lower operational costs.
Modern pneumatic conveying systems for dust extraction stations are designed with advanced features that enhance operational efficiency. These include variable speed drives, which allow for precise control of air flow and material transport rates, and automated control systems that monitor and adjust the process in real-time. The use of high-quality materials for the conveying line, such as stainless steel or special alloys, ensures durability and resistance to corrosion from the materials being transported. Additionally, the integration of sensors and monitoring equipment enables proactive maintenance, reducing downtime and extending the lifespan of the system.
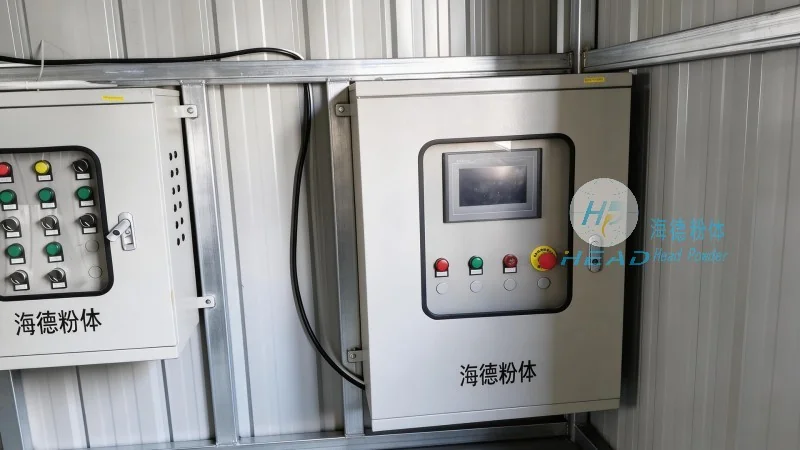
The principles and characteristics of pneumatic conveying at dust extraction stations are fundamental to the efficient operation of industrial processes. By understanding these aspects, industries can select and implement systems that best suit their specific needs, ensuring optimal performance and compliance with environmental regulations. As a leading provider in the field, Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing customized pneumatic conveying solutions tailored to the unique requirements of dust extraction applications.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top