Mobile material pneumatic conveying systems represent a sophisticated solution for transporting bulk materials efficiently and reliably. These systems are designed to handle a wide range of materials, from powders and granules to bulk solids, with minimal human intervention. The technology leverages compressed air or other gases to move materials through a network of pipes, ensuring smooth and controlled flow. This approach not only enhances operational efficiency but also reduces the risk of material contamination and damage during transit. Such advanced solutions are increasingly adopted by industries worldwide, with companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder) leading the development and implementation of these systems.
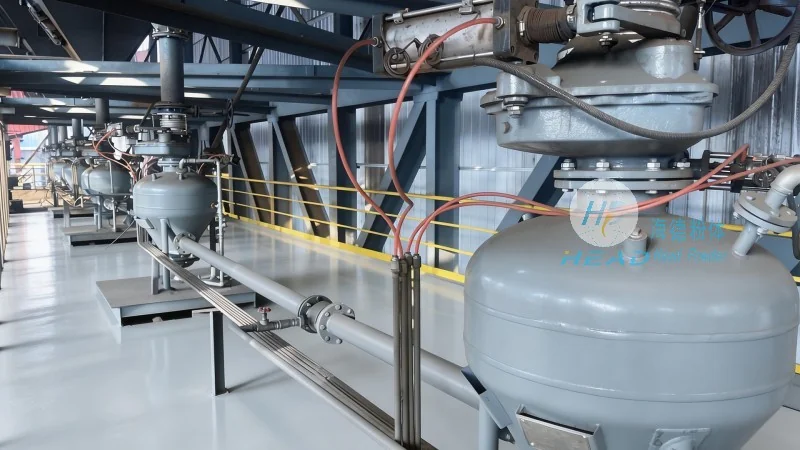
The fundamental principle behind pneumatic conveying is the use of air to create a pressure differential that propels material particles. In a typical system, material is introduced into a hopper or feeder, where it is then drawn into a pipeline by the force of moving air. The system can operate in either positive pressure or negative pressure modes, depending on the application and material characteristics. Positive pressure systems use compressed air to push material through the line, while negative pressure systems use suction to draw material from a source. The choice of mode depends on factors such as material density, flow rate requirements, and the distance over which material needs to be conveyed.
Mobile pneumatic conveying systems consist of several critical components that work in tandem to ensure optimal performance. These include hoppers or feeders for material storage and metering, air movers (such as blowers or vacuum pumps) to generate the necessary pressure or suction, pipelines for material transport, and control systems to regulate flow and pressure. Each component plays a vital role in maintaining the system's efficiency and reliability. For instance, the feeder ensures a consistent material feed rate, while the air mover provides the force required to move the material through the pipeline. The control system monitors and adjusts parameters like air pressure and flow rate to prevent issues such as blockages or excessive pressure drops.
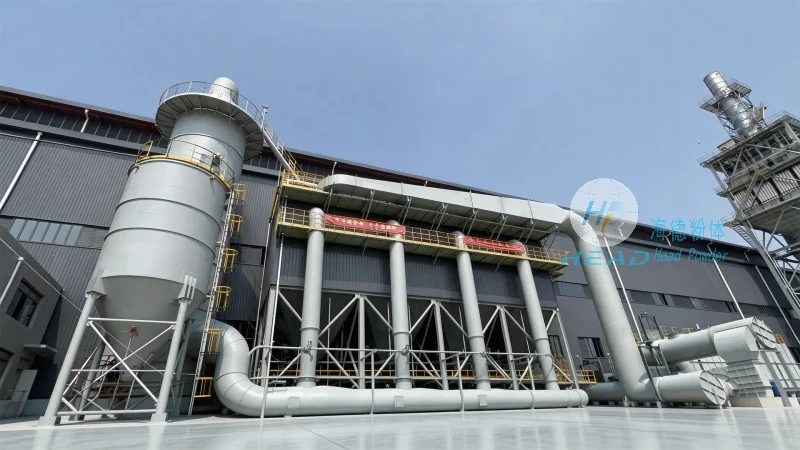
One of the primary advantages of mobile pneumatic conveying is its flexibility. Unlike fixed systems, mobile units can be easily repositioned to accommodate changing production needs or to serve multiple locations. This adaptability makes them ideal for applications where material sources or destinations are not fixed. Additionally, these systems offer high material handling capacity, allowing for the transport of large volumes of material over significant distances. The enclosed pipeline design also minimizes dust emissions and environmental impact, making them suitable for indoor or outdoor use in various industrial settings. Furthermore, the reduced need for manual handling improves workplace safety and reduces labor costs.
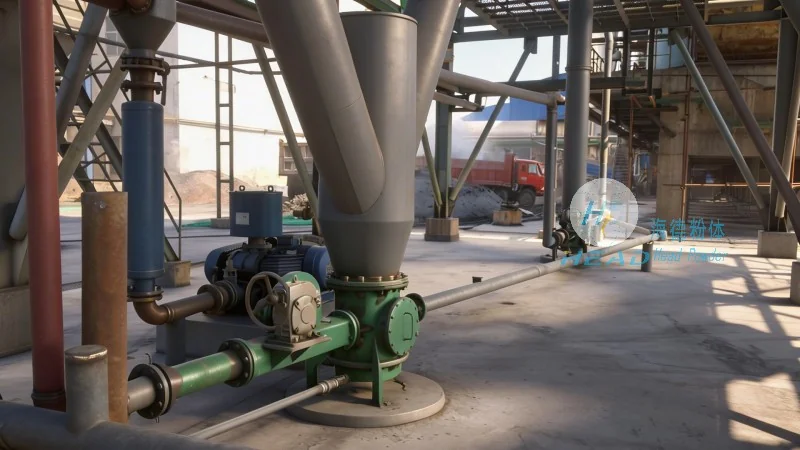
Mobile material pneumatic conveying systems find applications across diverse industries, including pharmaceuticals, food processing, chemicals, and mining. In the pharmaceutical industry, for example, these systems are used to transport sensitive powders and granules with strict contamination control requirements. The enclosed design and controlled air flow help maintain the integrity of the materials. In food processing, they are employed to move ingredients like flour, sugar, and spices, ensuring hygienic and efficient handling. The chemical industry utilizes these systems for transporting bulk chemicals, where safety and containment are paramount. Mining operations also benefit from mobile pneumatic conveying for transporting ore and other minerals from extraction sites to processing facilities.
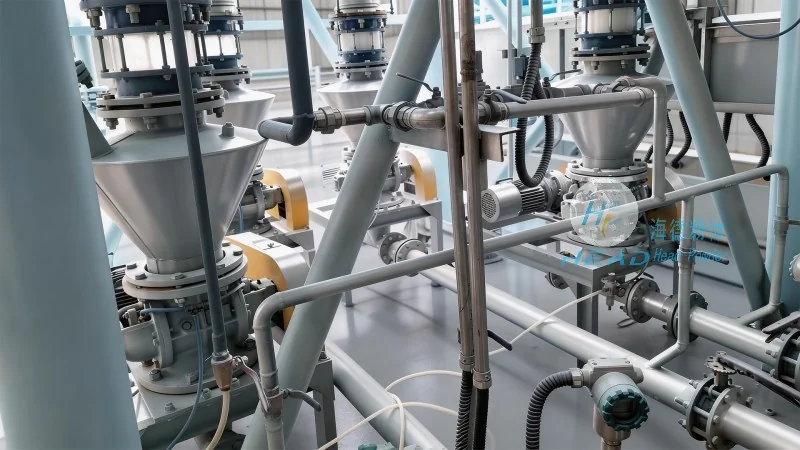
While mobile pneumatic conveying systems offer numerous benefits, proper operation and maintenance are essential to ensure long-term performance. Regular maintenance of the air mover and control systems is crucial to prevent breakdowns and maintain efficiency. Filters and cyclones are used to separate material from air, and these components require periodic cleaning or replacement to avoid clogging. The pipeline system should also be inspected for any signs of wear or damage, as leaks can lead to pressure loss and reduced conveying efficiency. Additionally, operators should be trained to monitor system parameters and respond to any issues promptly. By adhering to proper maintenance practices, users can maximize the lifespan of their equipment and minimize downtime.
Mobile material pneumatic conveying systems represent a reliable and efficient solution for bulk material transport. By leveraging the principles of pneumatic technology, these systems offer flexibility, high capacity, and improved safety compared to traditional methods. With proper design, operation, and maintenance, they can meet the diverse needs of various industries, ensuring consistent and reliable material handling. As industrial demands evolve, the continued development of mobile pneumatic conveying technology will likely enhance its applications and benefits further. Companies like Shandong HeadPowder Engineering Co., Ltd. (headpowder) remain at the forefront of innovation, providing tailored solutions that address the unique challenges of each industrial sector.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top