Phosphorus pentachloride (PCl₅) is a vital chemical reagent extensively utilized in the chemical industry, particularly in the synthesis of pesticides, pharmaceuticals, and other organic compounds. The safe and efficient handling of PCl₅ powder is crucial due to its high reactivity and potential hazards. Pneumatic conveying systems offer a reliable solution for transporting PCl₅ powder from storage to processing units, ensuring minimal exposure to personnel and preserving product integrity.
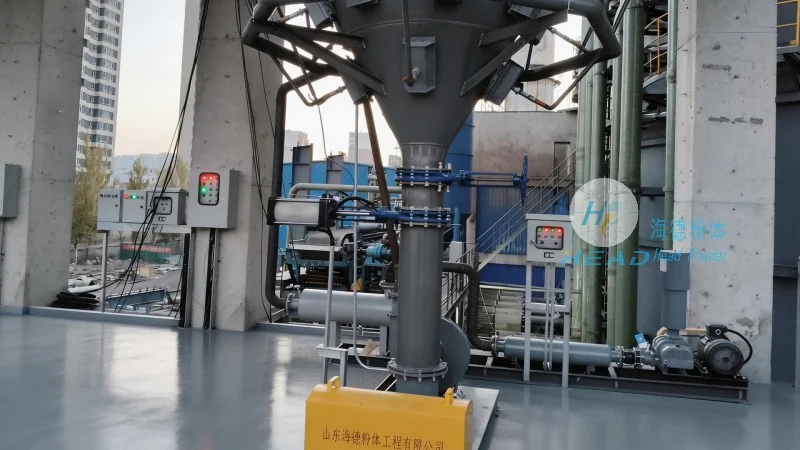
The fundamental principle of a PCl₅ powder pneumatic conveying line is the utilization of compressed air to transport dry bulk materials through a pipeline system. This method involves creating a pressure differential that propels the powder particles along the conveying line. The system typically comprises a hopper for material storage, a rotary valve for controlled discharge, a venturi or pressure vessel to accelerate the material-air mixture, and a receiver or processing unit at the destination. The air flow is regulated to maintain a consistent velocity, preventing particle segregation and ensuring smooth transport. For PCl₅, which is hygroscopic and reactive, the conveying system must be designed with corrosion-resistant materials and sealed components to avoid moisture ingress and chemical reactions.
Several key components collaborate to ensure the efficient operation of the PCl₅ powder pneumatic conveying line. The hopper serves as the primary storage vessel, equipped with a level indicator to monitor material levels. The rotary valve, often a star or slide valve, controls the flow rate of PCl₅ from the hopper into the conveying line, preventing backflow and maintaining a steady feed. The venturi or pressure vessel is critical for accelerating the material-air mixture, ensuring that the powder particles are entrained and transported at the required velocity. The receiver, typically a pressure vessel or a storage tank, collects the PCl₅ at the destination, with a discharge valve to release the material for processing. Additionally, filters and cyclones are integrated to separate the powder from the air stream, preventing dust contamination and ensuring compliance with environmental regulations.
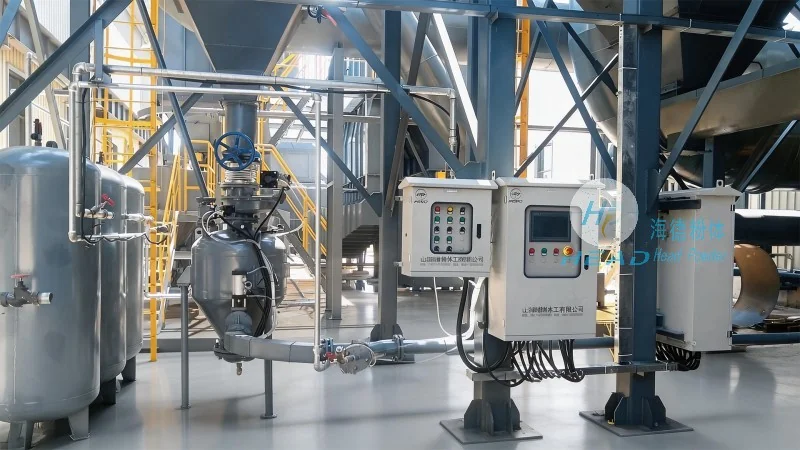
The working scene characteristics of PCl₅ powder pneumatic conveying lines are tailored to the specific demands of industrial processes. In chemical plants, these systems are commonly used to transport PCl₅ from bulk storage to reactors or reactors to downstream processing units. The design of the conveying line must consider the material's reactivity and potential for exothermic reactions, requiring temperature control and monitoring systems. For example, in the production of chlorinated organic compounds, the PCl₅ is often used as a chlorinating agent, and the conveying system must ensure that the material is delivered to the reactor at the precise temperature and concentration to avoid unwanted side reactions. The working scene also includes considerations for safety, such as explosion-proof designs and emergency shutdown systems, to protect personnel and equipment from the hazards associated with PCl₅ handling.
Implementing a PCl₅ powder pneumatic conveying line offers several advantages over traditional mechanical conveying methods. The primary benefit is the ability to handle PCl₅ in a closed system, minimizing exposure to personnel and reducing the risk of dust explosions. The system also provides better control over the material flow rate and velocity, ensuring consistent delivery to processing units. Additionally, pneumatic conveying systems are more flexible in terms of layout, allowing for horizontal, vertical, or inclined transport, which is particularly useful in complex plant layouts. The use of corrosion-resistant materials, such as stainless steel or special alloys, ensures the longevity of the system and reduces maintenance costs. For PCl₅, which is hygroscopic and reacts with moisture, the closed system prevents moisture ingress, maintaining the material's quality and reactivity.
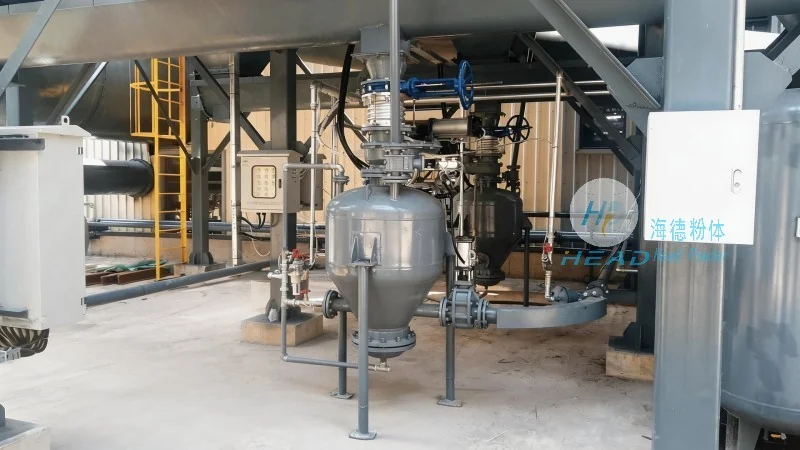
Operational considerations for PCl₅ powder pneumatic conveying lines include regular maintenance to ensure optimal performance. The rotary valve and venturi components require periodic cleaning to prevent clogging from PCl₅ particles, which can affect the system's efficiency. Filters and cyclones must be checked and replaced as needed to maintain air quality and prevent dust accumulation. Temperature and pressure monitoring systems are essential to detect any anomalies that could indicate a problem with the material or the system. Additionally, the system should be equipped with safety interlocks to prevent operation under abnormal conditions, such as low air pressure or high material levels. Regular inspections of the pipeline and components for signs of corrosion or wear are also necessary to ensure the system's reliability and safety.
Phosphorus pentachloride powder pneumatic conveying lines are a critical component in the safe and efficient handling of this hazardous chemical. By leveraging the principles of pneumatic conveying, these systems provide a reliable method for transporting PCl₅ from storage to processing units, while minimizing risks to personnel and maintaining product quality. The design and operation of such systems require careful consideration of the material's properties and the specific demands of the industrial application. With proper maintenance and operational controls, PCl₅ powder pneumatic conveying lines can significantly enhance productivity and safety in chemical manufacturing processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top