HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and installation of dust powder pneumatic conveying systems. This article delves into the fundamental principles behind these systems and highlights the key characteristics of their operational environments, providing a comprehensive overview for industry professionals and potential clients.
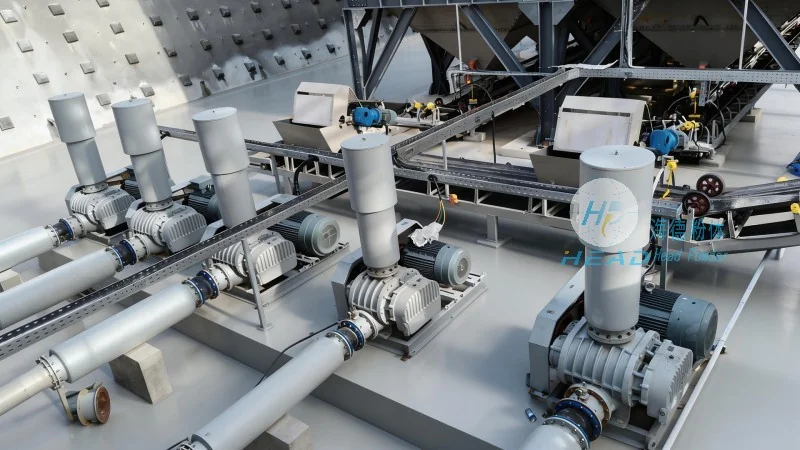
The fundamental principle of dust powder pneumatic conveying lines involves the use of air or gas to transport dry, powdery materials from one location to another. Unlike traditional mechanical conveying methods, which rely on belts, buckets, or screws, pneumatic systems utilize pressure or vacuum to move materials through a pipeline. This method is particularly effective for handling fine powders, such as those found in the chemical, food, and pharmaceutical industries, where maintaining material integrity and preventing contamination is critical.
At the heart of a pneumatic conveying system is the air compressor or vacuum pump, which generates the necessary pressure or vacuum to move the material. The system typically consists of a hopper for material storage, a feeder to control the flow rate, a pipeline for material transport, and a receiver to collect the material at the destination. The choice between pressure and vacuum systems depends on the specific application, with pressure systems generally used for short to medium distances and vacuum systems for longer distances or when the material needs to be drawn from a source.
The operational environment of dust powder pneumatic conveying lines is characterized by several distinct features that impact system performance and efficiency. One of the primary characteristics is the need for precise control over material flow and air pressure. This is crucial to prevent issues such as blockages, which can occur if the material is too fine or if the air flow is insufficient. Advanced control systems, often integrated with sensors and automation, are employed to monitor and adjust these parameters in real-time, ensuring smooth and consistent operation.
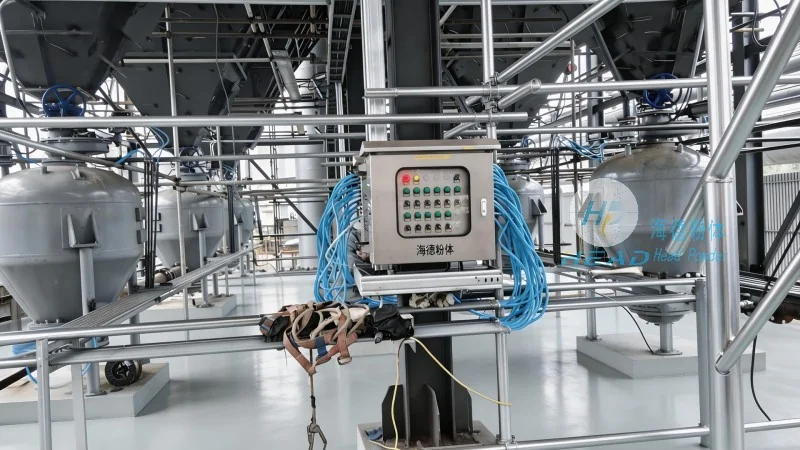
Another important characteristic is the system's ability to handle a wide range of materials, from fine powders to bulkier granules. This versatility makes pneumatic conveying suitable for diverse applications, including the transportation of chemicals, food additives, and pharmaceutical powders. The system's design allows for easy integration with existing production lines, minimizing downtime and facilitating seamless material transfer.
Environmental considerations also play a significant role in the working scene. Pneumatic conveying systems are designed to minimize dust emissions and ensure compliance with environmental regulations. Features such as dust collection systems and sealed pipelines help maintain a clean and safe working environment, reducing the risk of respiratory issues for operators and preventing contamination of the surrounding area.
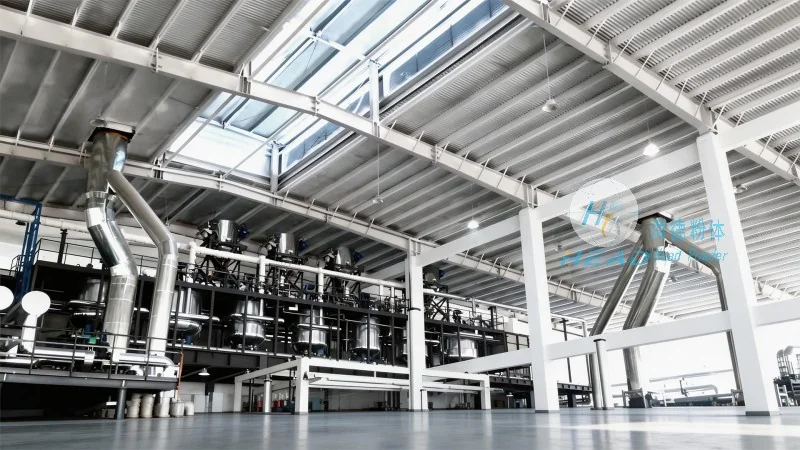
Dust powder pneumatic conveying lines are widely used in various industrial settings, each with unique requirements that influence system design and operation. For example, in the chemical industry, these systems are used to transport reactive powders, where maintaining a controlled environment is essential to prevent accidental reactions. In the food industry, the systems are designed to meet stringent hygiene standards, with stainless steel components and sealed pipelines to prevent contamination from external sources.
In the pharmaceutical industry, the focus is on maintaining product purity and sterility. Pneumatic conveying systems are often integrated with cleanroom technology, ensuring that the material is handled in a controlled environment free from contaminants. This is critical for pharmaceutical products, where even minor impurities can have significant health implications.
Furthermore, the scalability of pneumatic conveying systems allows them to be adapted to different production volumes and operational needs. Whether for small-scale laboratory applications or large-scale industrial production, these systems can be customized to meet specific requirements, making them a versatile solution for material handling challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top