HeadPowder, a leading provider in the field of material handling solutions, specializes in the design and manufacturing of advanced pneumatic conveying systems tailored for handling magnesium hydroxide powders. This article delves into the fundamental principles behind such equipment and highlights the key characteristics of its application across various industrial scenarios.
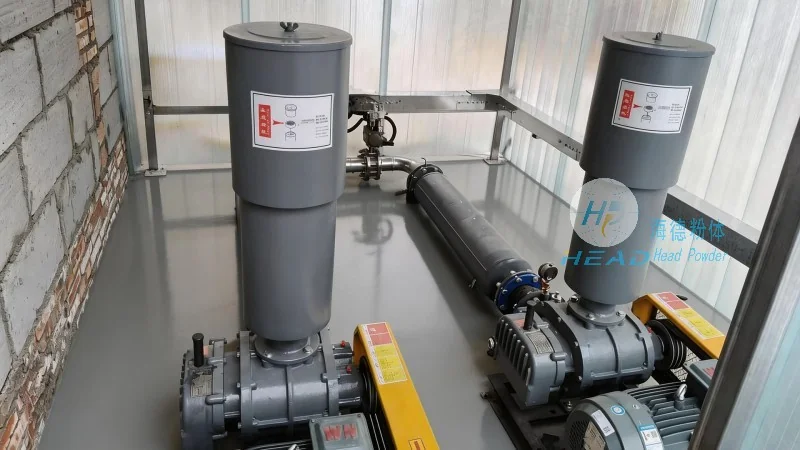
Magnesium hydroxide (Mg(OH)₂) is a widely used chemical compound in industries such as pharmaceuticals, food processing, and chemical manufacturing. Its powder form often requires efficient and reliable transportation from storage to processing units. Pneumatic conveying equipment offers a solution by utilizing air as the conveying medium to transport the powder, eliminating the need for mechanical components like belts or screws that may cause contamination or degradation of the product.
The core principle of pneumatic conveying involves creating a flow of air through a pipeline, which then carries the magnesium hydroxide powder particles. There are two primary types of pneumatic conveying systems: pressure and vacuum. In pressure systems, compressed air is introduced at the discharge end, pushing the powder forward. In vacuum systems, a vacuum is created at the receiving end, drawing the powder into the pipeline. The choice between these systems depends on factors like the distance to be covered, the volume of material to be conveyed, and the characteristics of the powder, including particle size, density, and moisture content.
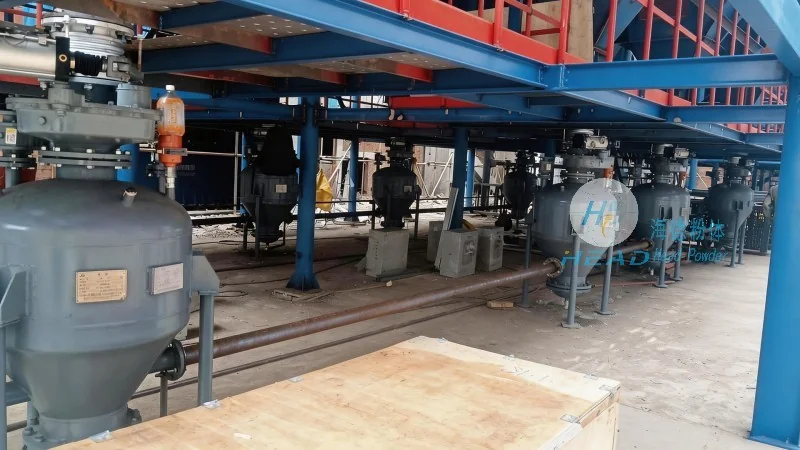
The pneumatic conveying equipment for magnesium hydroxide powders is engineered with several technical features to ensure optimal performance. These include:
The application of magnesium hydroxide powder pneumatic conveying equipment varies across different industrial settings, each with unique requirements and benefits:
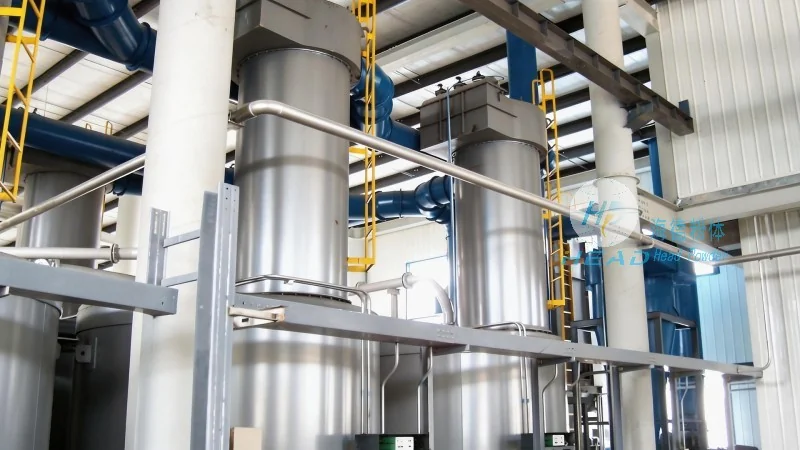
In pharmaceutical manufacturing, the purity and sterility of magnesium hydroxide are critical. The pneumatic conveying system is used to transport the powder from bulk storage to mixing and compounding units without direct human contact, reducing the risk of contamination. The system's ability to maintain a controlled environment ensures that the final product meets stringent quality standards.
For food-grade magnesium hydroxide applications, such as in food supplements or additives, the equipment is designed to be hygienic and easy to clean. The use of stainless steel components and sealed pipelines prevents cross-contamination with other materials, ensuring compliance with food safety regulations. The system's efficiency in handling fine powders also contributes to maintaining product quality and consistency.
In chemical plants, the handling of magnesium hydroxide powders may involve higher volumes and more aggressive conditions. The pneumatic conveying equipment is capable of handling large quantities of material over long distances, with the ability to integrate with other processing equipment such as reactors and reactors. The system's robust design ensures it can withstand the demands of continuous operation in a chemical manufacturing environment.
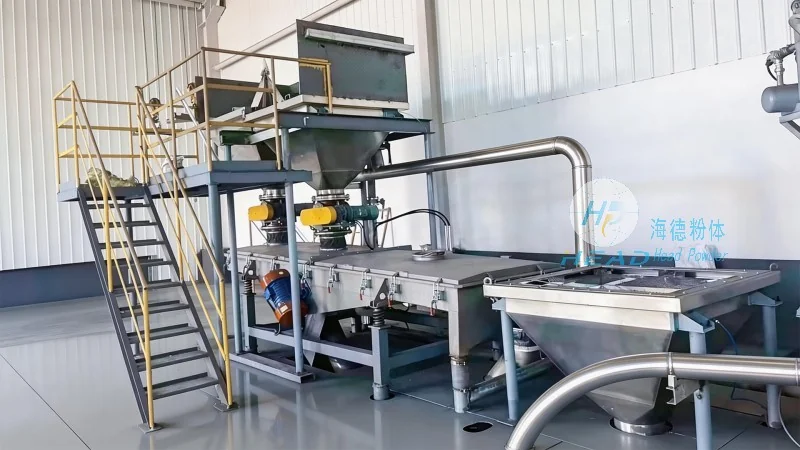
When operating in industrial settings, the safety and environmental impact of the pneumatic conveying system are paramount. The equipment is designed with features such as dust collection systems and explosion-proof components to mitigate risks associated with powder handling. Additionally, the system's energy efficiency helps reduce operational costs while minimizing the carbon footprint of the facility.
HeadPowder's magnesium hydroxide powder pneumatic conveying equipment combines advanced technology with practical design to meet the diverse needs of industrial applications. By understanding the principles of pneumatic conveying and the specific characteristics of magnesium hydroxide powders, the equipment ensures efficient, safe, and reliable transportation, contributing to improved productivity and product quality across various industries.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top