HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced pneumatic conveying systems tailored for dry pebble powder applications. This article explores the fundamental principles behind these systems and highlights key working scene characteristics that make them indispensable in various industrial settings.
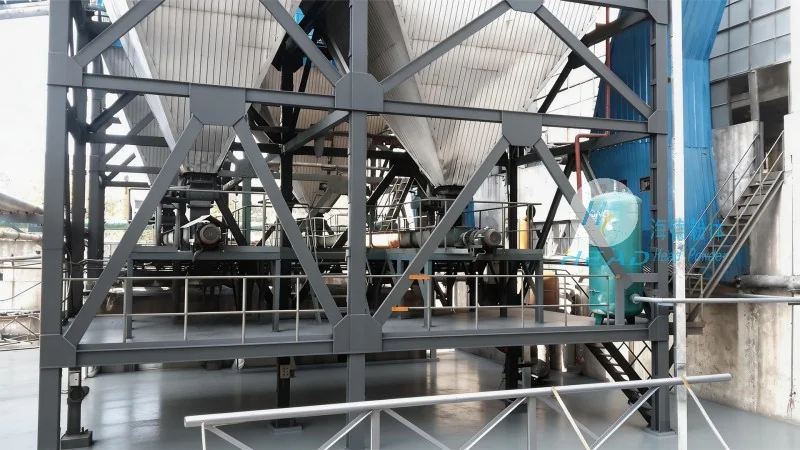
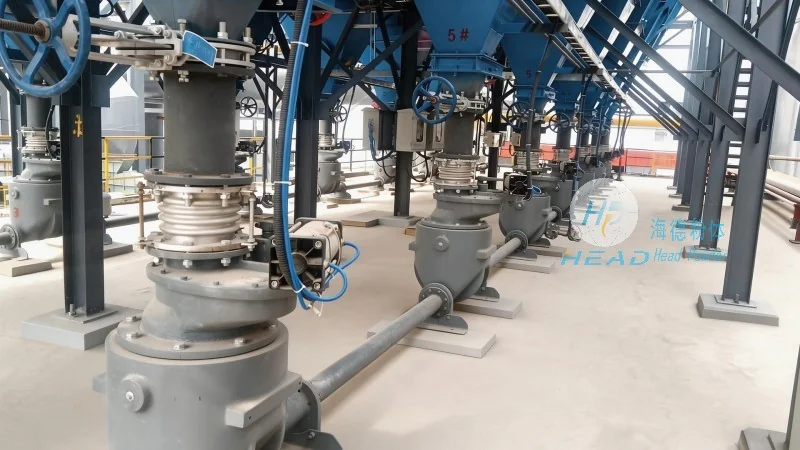
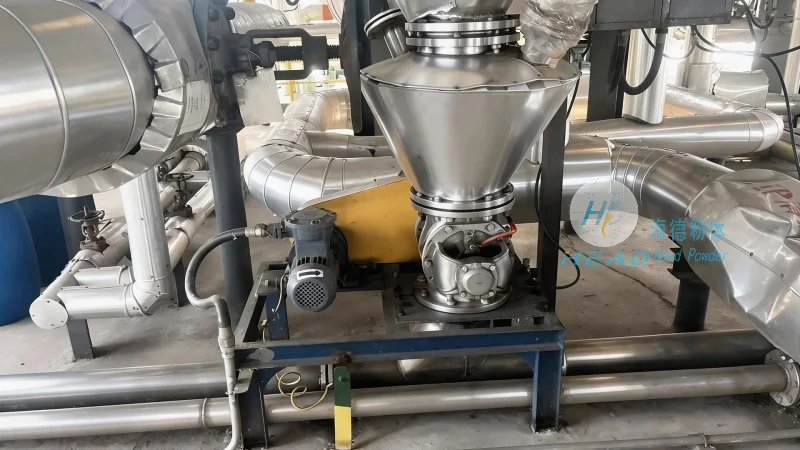
The pneumatic conveying of dry pebble powders relies on the fundamental principle of transporting bulk materials through a pressurized or vacuum air stream. Unlike traditional mechanical conveying methods, which often involve high maintenance and potential material degradation, pneumatic systems utilize air as the primary medium to move powders efficiently. The process typically involves a hopper where the pebble powder is stored, a conveying line where the material is propelled by air, and a discharge point where the powder is released. The key to effective operation lies in maintaining the right air pressure and flow rate to ensure consistent and reliable material transport. HeadPowder's systems are engineered to optimize these parameters, ensuring minimal particle breakage and maximum efficiency. The company's expertise in material science and fluid dynamics allows them to design systems that can handle a wide range of pebble powder characteristics, from fine to coarse particles, while maintaining high throughput rates. For example, in mining operations, where pebble powders are often coarse and abrasive, HeadPowder's systems are equipped with wear-resistant components to extend their service life. The use of high-quality materials and precision engineering ensures that the conveying lines can withstand the harsh conditions of industrial environments, reducing the risk of system failures and downtime. Additionally, the company's systems incorporate advanced control technologies, such as variable frequency drives (VFDs), which allow for precise regulation of air flow and pressure, further enhancing operational efficiency and energy savings.
One of the most significant advantages of pneumatic conveying systems for dry pebble powders is their ability to operate in diverse industrial environments. These systems are particularly suited for applications where traditional conveying methods are impractical or inefficient. For instance, in mining and quarry operations, where large volumes of pebble powders need to be transported over long distances, pneumatic systems offer a cost-effective solution. The flexibility of these systems allows them to be integrated into existing production lines, reducing the need for extensive infrastructure modifications. Additionally, the enclosed nature of pneumatic conveying minimizes dust emissions, making it a more environmentally friendly option compared to open-air methods. HeadPowder's systems are designed to meet stringent environmental regulations, ensuring that they can be used in industries where dust control is critical. Another key characteristic is the system's adaptability to different operating conditions. Whether in a high-temperature or high-humidity environment, HeadPowder's equipment is engineered to maintain optimal performance. The robust construction and advanced materials used in the manufacturing process ensure durability and longevity, reducing downtime and maintenance costs for industrial users. In food processing industries, where hygiene and cleanliness are paramount, HeadPowder's systems are constructed with stainless steel components and sealed designs to prevent contamination. This makes them suitable for transporting pebble powders used in food products, such as calcium supplements or mineral additives. The system's ability to maintain a clean and dust-free environment also enhances product quality and safety, which is crucial for meeting regulatory standards. Furthermore, in chemical processing plants, where pebble powders may be reactive or corrosive, HeadPowder's systems are equipped with specialized materials and coatings to protect against chemical exposure. These features ensure that the conveying equipment remains functional and safe, even in harsh chemical environments.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top