Ammonia fertilizer, a vital nutrient for crop growth, plays a crucial role in modern agricultural systems. The efficient and safe transportation of this fine powder is essential to ensure its optimal distribution and application. Powder pneumatic conveying has emerged as a sophisticated and effective method for handling ammonia fertilizer, offering advantages such as reduced dust generation, improved operational safety, and enhanced material flow control. This article explores the fundamental principles of ammonia fertilizer powder pneumatic conveying, detailing its working mechanisms and the specific characteristics of various application scenarios to provide a comprehensive understanding of the technology.
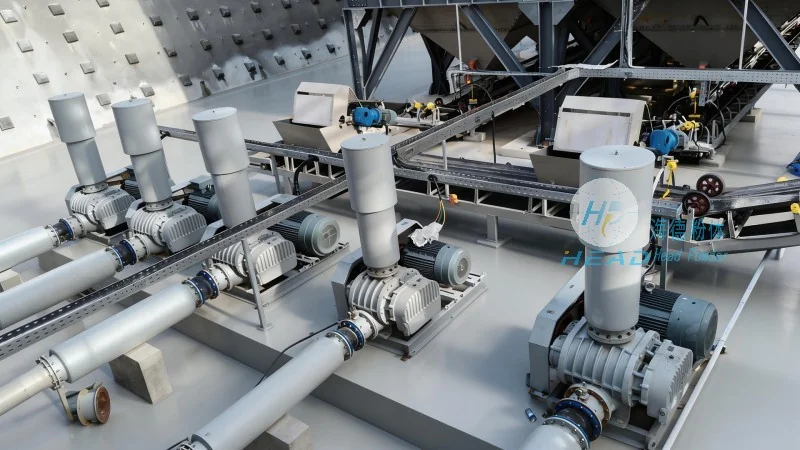
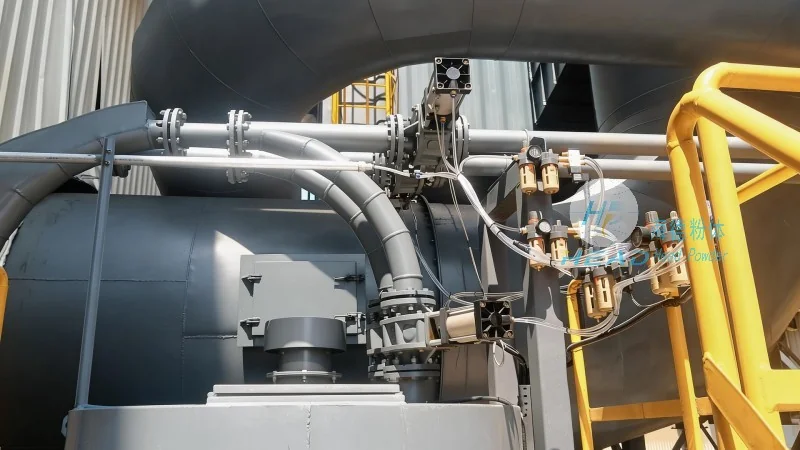
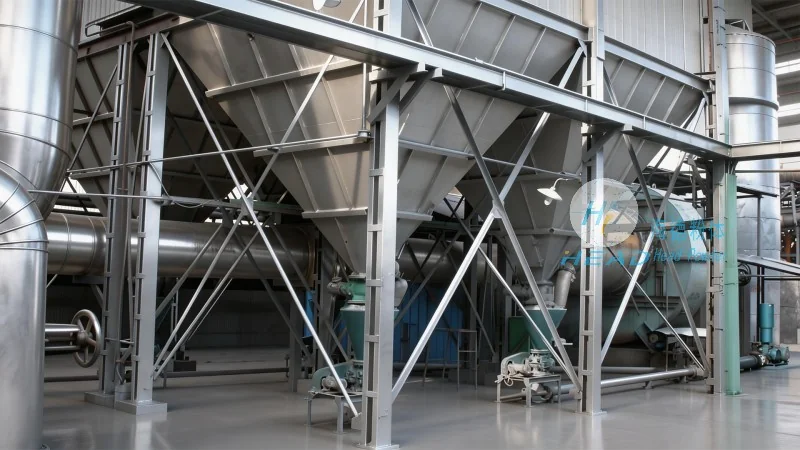
Pneumatic conveying involves the transport of solid particles, including ammonia fertilizer, using a gas stream, typically air or a mixture of air and other gases. The process relies on the creation of a pressure differential or a vacuum to move the material through a pipeline system. For ammonia fertilizer, this method is particularly advantageous due to the material's fine particle size, which can cause clogging in traditional mechanical systems, and its sensitivity to moisture and contamination. The core principles of pneumatic conveying include selecting the appropriate air velocity, pressure, and pipeline design to achieve efficient and consistent material transport. Key factors influencing the conveying process include the particle size distribution, bulk density, and moisture content of the fertilizer, all of which affect the required air flow rate and pressure levels. The two primary types of pneumatic conveying systems are pressure and vacuum systems. Pressure systems use a blower to generate positive pressure, pushing the material through the pipeline from the feed point to the discharge point. This method is ideal for short to medium distances and high material flow rates. Vacuum systems, on the other hand, use a vacuum pump to create a negative pressure, drawing the material from the feed point into the pipeline. Vacuum conveying is more suitable for longer distances or when the material needs to be transported from multiple sources, as it can effectively handle the material over greater distances without significant pressure loss.
The application of ammonia fertilizer powder pneumatic conveying varies across different industrial and agricultural settings, each with distinct characteristics that influence the system design and operational parameters. In large-scale fertilizer production facilities, the system may need to handle high volumes of material over long distances, requiring robust pipeline networks and high-capacity blowers. The pipeline design may include multiple branches and elevation changes to accommodate the layout of the production plant. In contrast, smaller agricultural operations might utilize compact, portable systems suitable for on-site fertilizer distribution, such as in field application or small-scale farms. The working scene characteristics also include considerations for environmental conditions, such as temperature and humidity, which can impact the material's flow properties and the system's performance. For example, in hot climates, the system may need to incorporate cooling mechanisms to prevent the material from clumping or caking due to moisture absorption. Additionally, safety protocols are paramount due to the potential hazards associated with ammonia, including its corrosive nature and the risk of leaks, making the design of sealed and leak-proof systems essential. The system may also need to comply with local environmental regulations regarding dust emissions and air quality, which can influence the choice of filtration and exhaust systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top