Shandong HeadPowder Engineering Co., Ltd. is a professional manufacturer specializing in the design, development, and production of fertilizer granular material conveying equipment. The company is located in Shandong, China, and has established a strong reputation in the industry for its innovative solutions tailored to the needs of fertilizer processing and handling.
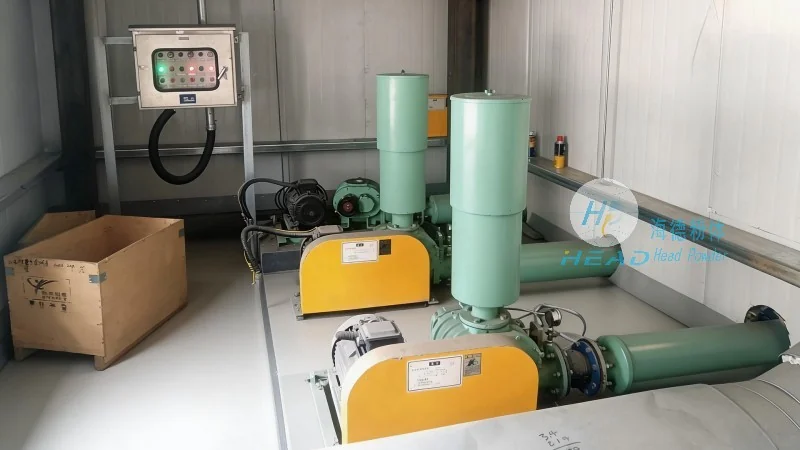
The fertilizer granular material conveying system equipment operates on the principle of mechanical transport, utilizing advanced technologies such as screw conveyors, belt conveyors, and pneumatic systems. These systems are engineered to handle the specific characteristics of fertilizer granules, including their size, density, and flowability. The core components include feeders, conveyors, and control units that work in tandem to ensure efficient and reliable material transport. The screw conveyor, for instance, uses rotating screws to move granular materials through a closed tube, providing a continuous and controlled flow. This mechanism minimizes material degradation and ensures consistent delivery to the next processing stage.
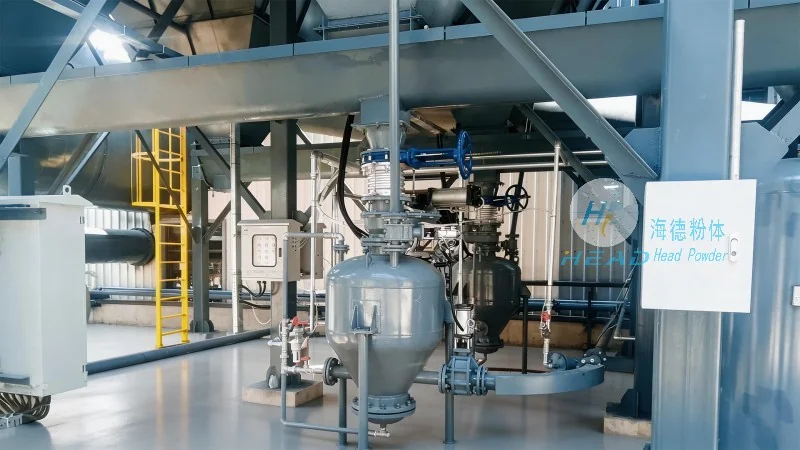
The working scene characteristics of these conveying systems are tailored to various industrial applications within the fertilizer industry. In large-scale fertilizer production facilities, the equipment is designed to handle high volumes of granular materials, supporting continuous production lines. The systems are also adapted for different operational environments, from indoor processing plants to outdoor storage and transfer operations. Key features include durability, as the equipment is constructed from corrosion-resistant materials to withstand the chemical properties of fertilizers. Additionally, the systems are equipped with safety mechanisms and monitoring systems to ensure operational safety and compliance with industry standards. The adaptability of the conveying systems allows them to integrate seamlessly with existing production infrastructure, enhancing overall operational efficiency.
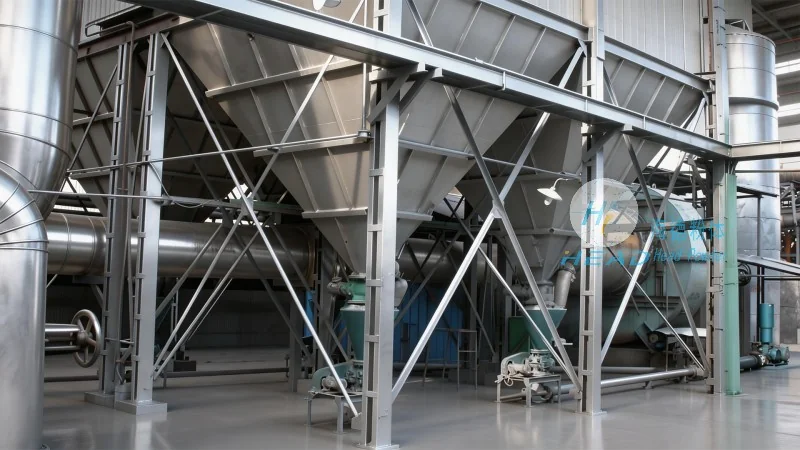
The advantages of using fertilizer granular material conveying systems extend beyond basic transport. These systems contribute to improved production efficiency by reducing downtime and ensuring a steady supply of materials to downstream processes. The precise control over material flow helps maintain consistent product quality, which is critical in fertilizer manufacturing. Furthermore, the energy-efficient design of modern conveying systems minimizes operational costs, making them a cost-effective solution for businesses in the fertilizer sector. The systems also support environmental compliance by reducing dust emissions and improving material handling safety, aligning with industry regulations and sustainability goals.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top