HeadPowder, a leading manufacturer based in Shandong, China, specializes in providing advanced material handling solutions tailored for the efficient processing of magnesium sulfate. This article delves into the core principles underlying magnesium sulfate material handling systems and highlights the key characteristics of their operational scenarios, offering insights into how these systems enhance productivity and safety in industrial applications.
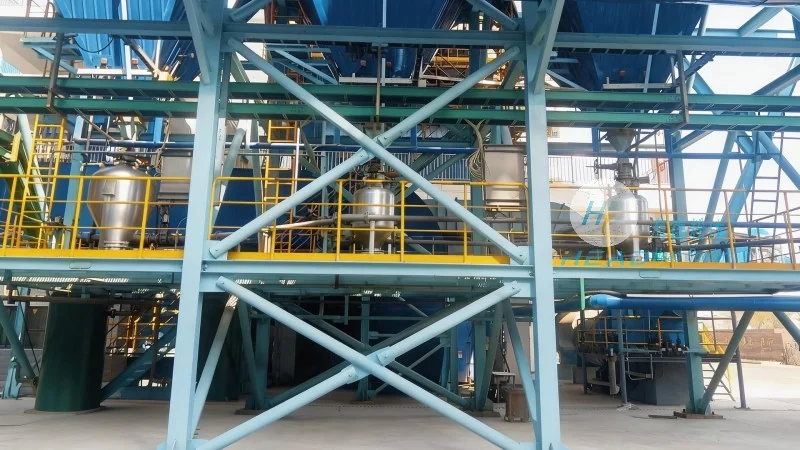
The fundamental principle of magnesium sulfate material handling systems revolves around the efficient transport, storage, and transfer of this chemical compound. Magnesium sulfate, commonly known as Epsom salt, is widely used in various industries including pharmaceuticals, agriculture, and food processing. The systems are designed to handle the unique physical properties of magnesium sulfate, such as its granular or crystalline form, varying moisture content, and potential for dust generation. Key components typically include conveyors, feeders, storage silos, and control systems that work in tandem to ensure smooth material flow. The design emphasizes durability, as the equipment must withstand the corrosive and abrasive nature of the material over extended periods of operation. Advanced materials and coatings are often employed to protect against wear and chemical degradation, ensuring long-term reliability.
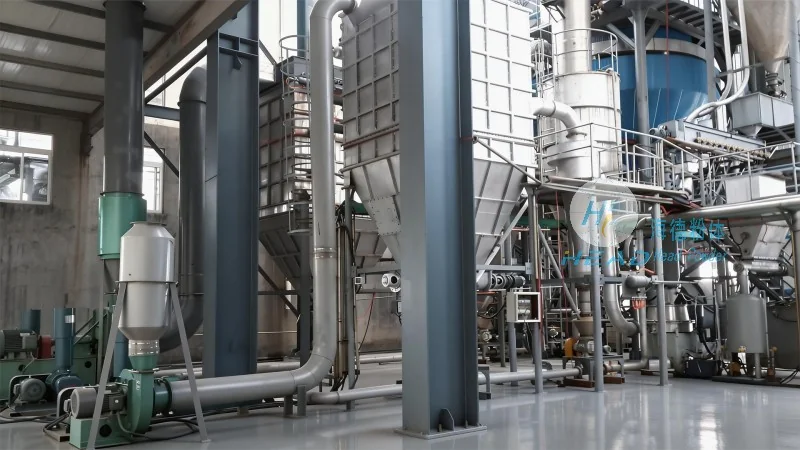
The operational scenarios for magnesium sulfate material handling systems vary significantly based on the end-use application and the scale of production. In pharmaceutical manufacturing, for instance, the systems are required to maintain stringent hygiene standards and precise control over material handling to prevent contamination. This often involves enclosed conveyor systems with HEPA filtration and stainless steel construction. In agricultural settings, the systems may need to handle bulk quantities of magnesium sulfate for fertilizer production, requiring robust, high-capacity equipment capable of withstanding outdoor conditions and heavy usage. The characteristics of these working scenes include considerations for dust control, as magnesium sulfate can generate fine particles that pose health risks and environmental concerns. Additionally, the systems must be adaptable to different particle sizes and moisture levels, which can fluctuate based on the source of the material or the processing stage. The integration of sensors and automation technologies is crucial in modern systems to monitor flow rates, detect blockages, and adjust operational parameters in real-time, enhancing efficiency and reducing downtime.
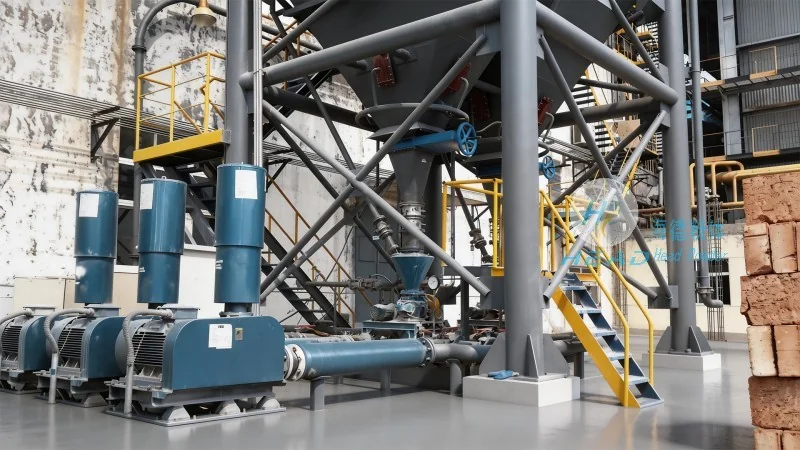
HeadPowder's magnesium sulfate material handling systems are engineered with application-specific features that address the unique challenges of each operational scenario. For example, in food processing industries, the systems incorporate sanitary design elements, such as easy-to-clean surfaces and hygienic sealing mechanisms, to meet regulatory requirements. In contrast, industrial applications may prioritize cost-effectiveness and durability, utilizing heavy-duty components that can handle high volumes of material with minimal maintenance. The advantages of these systems extend beyond mere material transport; they also contribute to overall operational efficiency by reducing manual handling, minimizing material loss, and improving safety through automated processes. The modular design of many systems allows for flexibility in scaling up or modifying the setup to accommodate changing production needs, providing a long-term solution for businesses. Furthermore, the integration of energy-efficient technologies helps reduce operational costs while maintaining performance standards.
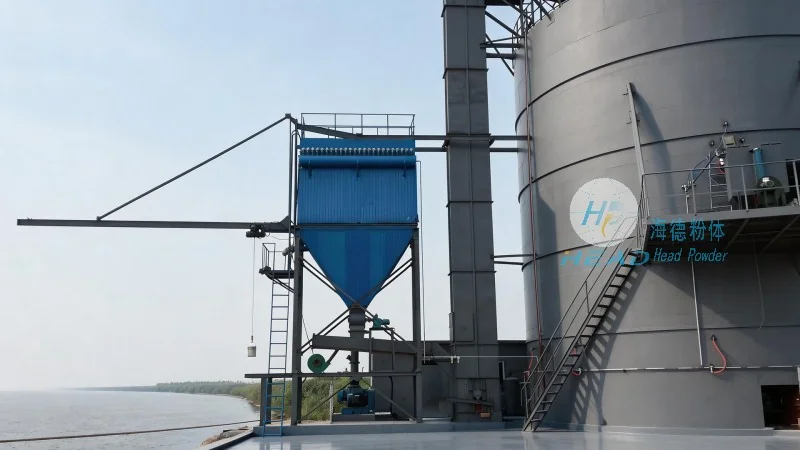
HeadPowder Engineering Co., Ltd., with its headquarters in Shandong, China, continues to innovate in the development of magnesium sulfate material handling systems, focusing on the principles of efficiency, safety, and adaptability. By understanding the specific requirements of different working scenarios, these systems provide tailored solutions that optimize material flow and reduce operational risks. The combination of robust engineering, advanced materials, and intelligent control systems ensures that magnesium sulfate can be handled safely and effectively, supporting the diverse needs of various industries. As industries evolve, the importance of reliable material handling systems becomes increasingly critical, and companies like HeadPowder are at the forefront of delivering solutions that meet these demands.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top