For industrial facilities dealing with bulk material handling, the tonne bag unpacking and material conveying system represents a critical piece of equipment designed to streamline the process of converting large, packaged materials into manageable quantities for further processing or distribution. This system integrates multiple components to efficiently handle the entire workflow from bag opening to material transport, ensuring high throughput and operational reliability.
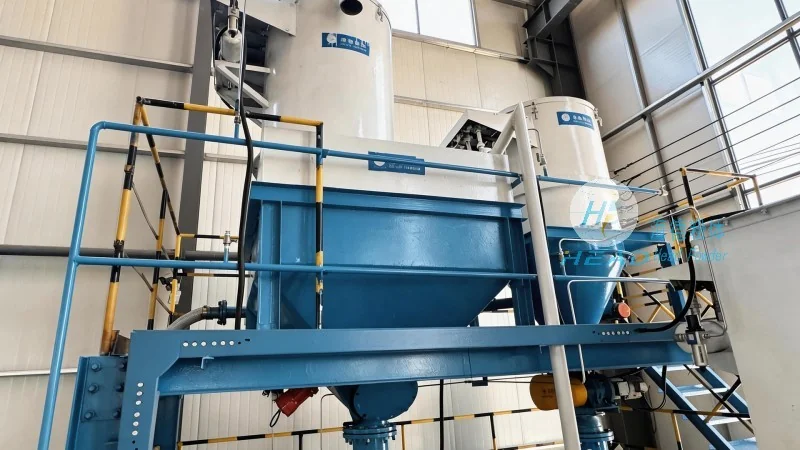
The tonne bag unpacking material conveying system typically comprises several key components, each playing a vital role in the overall operation. The primary stages include bag opening mechanisms, material discharge systems, and conveying units. The bag opening component may utilize hydraulic or mechanical force to rupture the bag, allowing the contained material to flow out. This is often followed by a discharge hopper or chute that directs the material into a conveyor system. The conveying system, which can be belt, screw, or pneumatic, then transports the material to the next processing stage or storage location.
During operation, the system operates in a sequential manner. The bag is positioned on a loading platform, and the opening mechanism activates to break the bag's seal. The material then falls into the discharge hopper, where it is collected and transferred by the conveyor. This design minimizes manual intervention, reducing labor costs and improving safety by eliminating the need for workers to handle heavy or potentially hazardous bags. The system's efficiency is further enhanced by its ability to handle various material types, including powders, granules, and bulk solids, making it versatile for different industrial applications.
The working scene characteristics of the tonne bag unpacking material conveying system are tailored to meet the demands of diverse industrial settings. These systems are commonly found in industries such as mining, construction, agriculture, and chemical processing, where bulk materials are frequently transported in tonne bags. The equipment is designed to operate in both indoor and outdoor environments, with some models featuring weather-resistant components to ensure continuous operation in varying conditions.
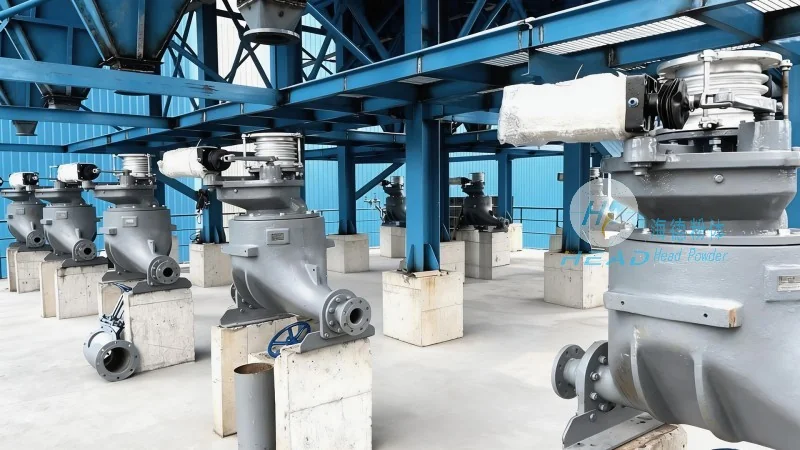
In mining operations, for example, the system is used to process ore or rock that has been packaged in tonne bags after initial crushing or screening. The system efficiently unloads the material and conveys it to a conveyor belt or storage silo, facilitating the next stage of processing. In construction sites, the system may handle bulk materials like cement or sand, improving material handling efficiency and reducing the time required for manual unloading. The system's adaptability also makes it suitable for agricultural applications, where it can process fertilizers or seeds packaged in tonne bags, supporting efficient farm operations.
The working scene characteristics also include considerations for space and layout. The system is designed to fit into existing industrial layouts, with modular components that can be customized to fit specific facility dimensions. This flexibility allows for integration into both new and existing production lines, minimizing disruption to ongoing operations. Additionally, the system's noise and dust control features are important in many industrial environments, as they help maintain a safe and comfortable working environment for personnel.
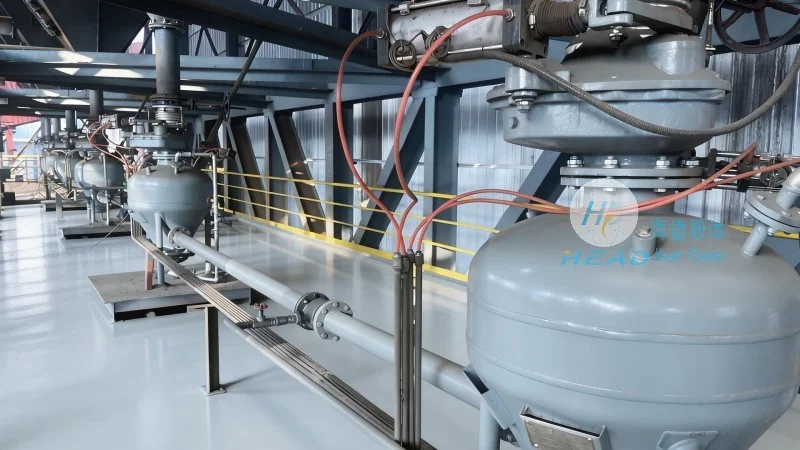
HeadPowder, a leading manufacturer of material handling equipment, specializes in the design, development, and production of advanced tonne bag unpacking and conveying systems. With a strong focus on innovation and customer satisfaction, the company has established itself as a trusted provider in the industry. HeadPowder's headquarters is located in Shandong, China, where the company's research and development team continuously works to improve product performance and reliability.
The company's commitment to quality is evident in its manufacturing processes, which adhere to international standards and undergo rigorous testing to ensure each system meets the highest performance criteria. HeadPowder's products are known for their durability, efficiency, and ease of maintenance, making them a preferred choice for industrial clients worldwide. The company also provides comprehensive after-sales support, including installation, training, and technical assistance, to ensure customers maximize the value of their investment.
With a presence in China and a growing international market, HeadPowder continues to expand its product portfolio and service capabilities. The company's dedication to customer needs and technological advancement positions it as a key player in the material handling equipment industry, delivering solutions that enhance operational efficiency and safety for its clients.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top