Positive pressure dilute phase material handling systems represent a sophisticated approach to transporting bulk materials over long distances with efficiency and reliability. This technology is designed to handle a wide range of powders and granular materials, ensuring minimal product degradation while maintaining high throughput rates. The core principle revolves around creating a positive pressure environment within the pipeline, which forces the material to move through the system under pressure, eliminating the need for vacuum or external power sources beyond the initial feeding mechanism.
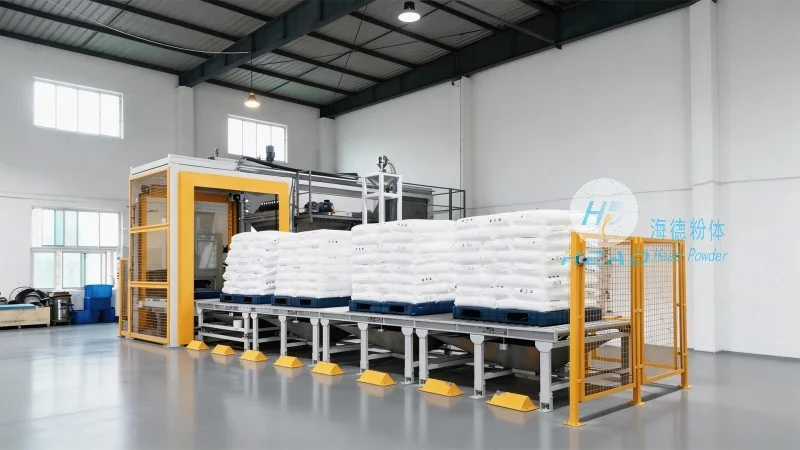
The system operates on the principle of positive pressure, where air or gas is introduced into the material stream to create a slurry-like mixture. This mixture, known as a dilute phase, allows the material to be transported at high velocities through the pipeline. The key components include a feeder, a positive pressure blower or compressor, and a pipeline network. The feeder ensures a consistent feed rate, while the blower maintains the necessary pressure to propel the material. The pipeline is typically made of corrosion-resistant materials like stainless steel or special alloys to handle various materials, such as cement, coal, or agricultural products. The system is designed with pressure regulators and flow control valves to minimize pressure drops and maintain a stable flow, which is crucial for consistent performance and preventing material blockages.
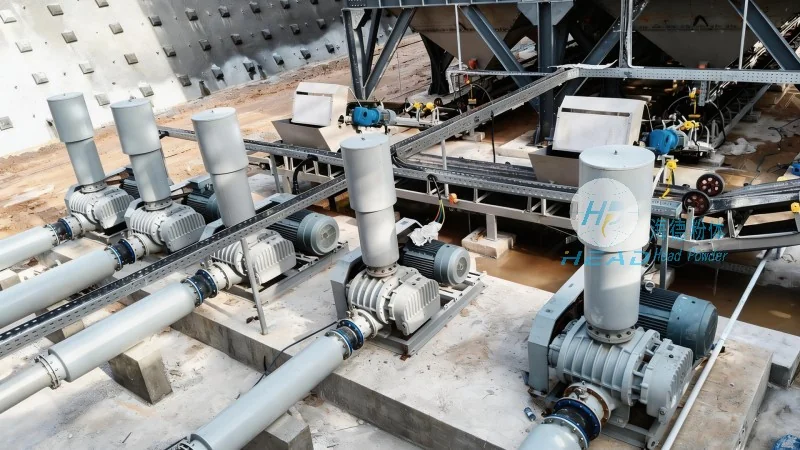
These systems are widely used in various industrial sectors, including cement production, coal handling, and food processing. In cement plants, they are used to transport raw materials and finished products from storage silos to production lines, ensuring a continuous supply of materials for cement manufacturing. In coal handling facilities, they efficiently move coal from stockpiles to boilers, supporting power generation and industrial processes. Agricultural applications include the transport of grain and other bulk agricultural products from farms to processing facilities, facilitating efficient post-harvest handling. The versatility of the system allows it to adapt to different material characteristics and operational requirements, making it a preferred choice for industries requiring reliable bulk material transport over long distances.
Compared to other material handling methods, such as vacuum systems or mechanical conveyors, positive pressure dilute phase systems offer several advantages. They are more energy-efficient, as they require less power to maintain pressure and can operate with lower energy consumption. The positive pressure environment also reduces the risk of product contamination and degradation, which is critical for sensitive materials like pharmaceuticals or food products. Additionally, the system is capable of handling a wide range of material sizes and densities, from fine powders to coarse granules, without the need for pre-processing or material modification. The ability to operate over long distances without intermediate storage or transfer points further enhances operational efficiency and reduces downtime, leading to improved productivity and cost savings for industrial operations.
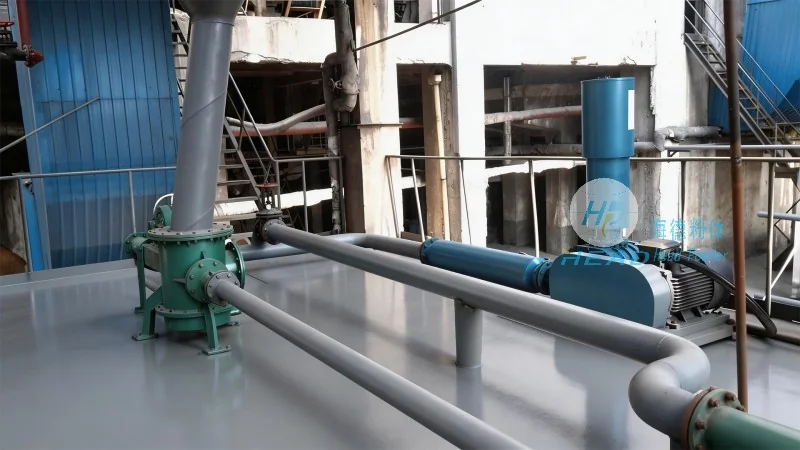
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer and supplier of material handling equipment, specializing in positive pressure dilute phase systems. With a strong commitment to innovation and quality, the company has developed advanced solutions tailored to the needs of various industries. HeadPowder's products are designed to meet international standards and are backed by comprehensive technical support and after-sales service. The company's headquarters is located in Shandong, China, where it leverages local expertise and resources to deliver high-quality equipment to global markets, serving clients in sectors such as cement, coal, agriculture, and more. HeadPowder's dedication to customer satisfaction and technological advancement has established it as a trusted partner in the material handling industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top