Principles and Application Scenarios of Pharmaceutical Material Handling Equipment
Release time:2026-09-19 11:01:31
name of the company:Shandong Headpowder Engineering Co., Ltd.
telephone:156-6277-7102
contacts:Manager Zhang
Pharmaceutical material handling equipment is essential for the efficient and compliant transfer of materials throughout pharmaceutical manufacturing processes. These systems are designed to ensure product integrity, safety, and regulatory adherence while optimizing operational efficiency. Understanding the core principles and diverse application scenarios of such equipment is crucial for pharmaceutical facilities aiming to enhance productivity and maintain industry standards.
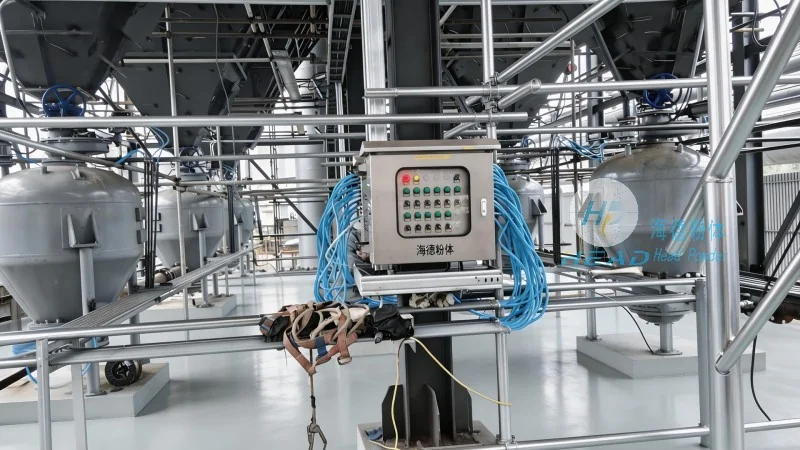
Company Overview
HeadPowder, a prominent manufacturer based in Shandong, China, specializes in developing high-quality pharmaceutical material handling solutions. As Shandong HeadPowder Engineering Co., Ltd., the company leverages advanced engineering and industry expertise to deliver tailored equipment that meets the stringent requirements of pharmaceutical production. HeadPowder's commitment to innovation and compliance ensures that their systems enhance operational performance while adhering to global regulatory standards.
Core Principles of Pharmaceutical Material Handling Systems
The fundamental principles guiding pharmaceutical material handling equipment revolve around precision, hygiene, and safety. These systems are engineered to handle sensitive materials with minimal risk of contamination, ensuring each step of the material transfer process aligns with regulatory expectations. Key principles include:
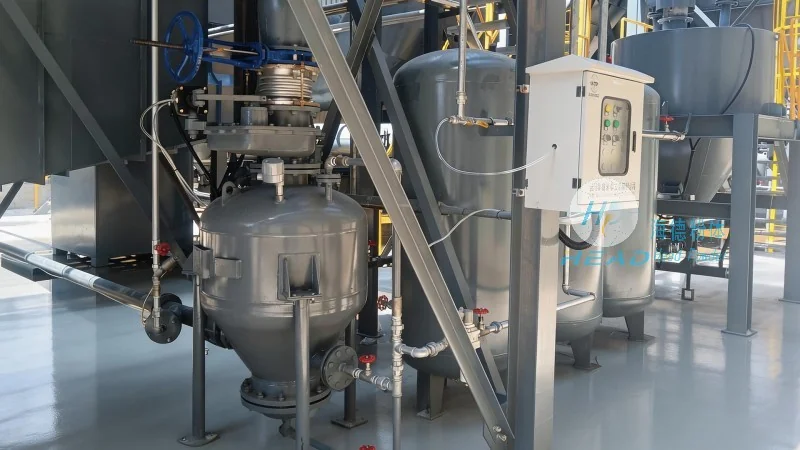
- Hygienic Design: Equipment features smooth, non-porous surfaces and easy-to-clean components to prevent product contamination and facilitate thorough sanitation.
- Material Compatibility: Components are constructed from materials like stainless steel, PTFE, or specialized plastics that are compatible with pharmaceutical substances, avoiding chemical reactions or degradation.
- Controlled Environment Integration: Systems often operate within cleanroom environments, utilizing air filtration and positive pressure to maintain sterile conditions during material transfer.
- Automation and Integration: Advanced control systems enable seamless integration with production lines, allowing real-time monitoring and adjustment of material flow to optimize efficiency.
Key Components and Their Functions
Pharmaceutical material handling equipment comprises interconnected components, each serving a specific role to ensure smooth operation. Common components include:
- Pneumatic Conveying Systems: Use air pressure to transport powders and granules through a network of pipes, offering flexibility and low maintenance.
- Vacuum Lifters: Employ vacuum technology to lift and move bulk materials, providing gentle handling suitable for delicate pharmaceutical products.
- Belt Conveyors: Utilize continuous belts to transport materials over longer distances, ideal for moving larger quantities with consistent speed and direction.
- Pneumatic Dosing Systems: Precisely measure and dispense materials into containers or processing equipment, ensuring accurate dosing and minimizing waste.
- Material Handling Robots: Automated robotic systems for handling and transferring items, enhancing precision and reducing human error in repetitive tasks.
Application Scenarios in Pharmaceutical Manufacturing
The versatility of pharmaceutical material handling equipment makes it applicable across various manufacturing stages. Key application scenarios include:
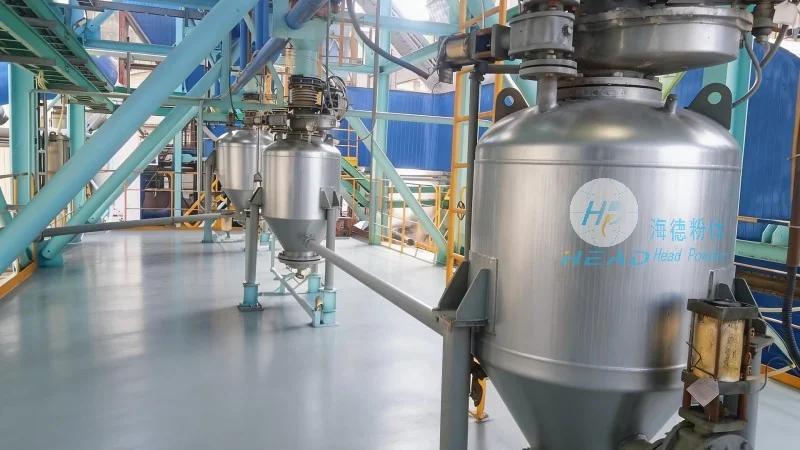
- Raw Material Handling: Efficiently transporting raw ingredients from storage to production lines, ensuring timely availability and minimizing material waste.
- Intermediate Product Transfer: Moving partially processed materials between production stages, maintaining product integrity and preventing cross-contamination.
- Finished Product Packaging: Transferring finished pharmaceutical products from production lines to packaging machines, ensuring consistent and accurate packaging.
- Quality Control Sampling: Handling samples for testing and analysis, enabling rapid and reliable quality checks throughout the production cycle.
- Waste Management: Transporting waste materials from production areas to disposal or recycling facilities, maintaining a clean and organized manufacturing environment.
Advantages of Advanced Pharmaceutical Material Handling Solutions
Implementing modern pharmaceutical material handling equipment offers significant benefits to manufacturers. These include:
- Increased Efficiency: Automated systems reduce manual labor, leading to faster material transfer and shorter production cycles.
- Enhanced Product Quality: Precise control over material handling minimizes product damage, ensuring consistent quality and reducing defects.
- Improved Safety: Automated and enclosed systems reduce human exposure to hazardous materials, lowering workplace accident risks.
- Regulatory Compliance: Hygienic and controlled designs help manufacturers meet stringent regulatory requirements, avoiding penalties and maintaining market access.
- Scalability: Modular systems can be easily expanded or reconfigured to accommodate changes in production volume or product lines.
Conclusion
Pharmaceutical material handling equipment is a critical component of modern pharmaceutical manufacturing, enabling efficient, safe, and compliant material transfer. Companies like Shandong HeadPowder Engineering Co., Ltd. in Shandong, China, are leading the development of innovative solutions that address the unique challenges of the pharmaceutical industry. By understanding the principles and application scenarios of these systems, manufacturers can optimize operations, enhance product quality, and remain competitive in a highly regulated market.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China
