HeadPowder, a leading engineering company based in Shandong, China, specializes in the design and manufacturing of advanced conveying systems for dry coffee materials. This article explores the fundamental principles behind these systems and highlights key application scenarios where they are utilized effectively.
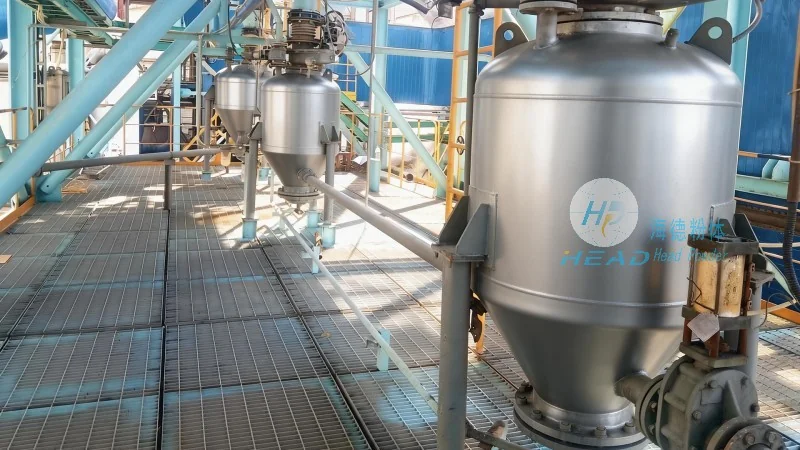
The core principle of dry coffee material conveying systems is to transport coffee beans, ground coffee, or other dry coffee-related products efficiently and safely from one processing stage to another. These systems typically operate on the basis of mechanical force, such as gravity, vacuum, or positive pressure, to move materials through a network of pipes, hoppers, and other components. The design of these systems is tailored to handle the unique properties of coffee materials, including their varying sizes, moisture content, and susceptibility to dust generation. Advanced systems may incorporate features like air filtration, temperature control, and material separation to ensure optimal performance and product quality.
At the heart of a dry coffee material conveying system are several critical components that work in concert to achieve reliable material transport. The primary components include feed hoppers, which are used to store and feed the coffee material into the system; conveying mechanisms, such as screw conveyors, pneumatic conveyors, or bucket elevators, which move the material through the system; and discharge units, which deliver the material to the next processing stage. Each component is engineered to handle the specific characteristics of coffee materials, ensuring minimal product degradation and maximum efficiency. For example, screw conveyors are commonly used for horizontal or slight incline transport, while pneumatic conveyors are ideal for vertical or long-distance transport due to their ability to handle fine powders and prevent material buildup.
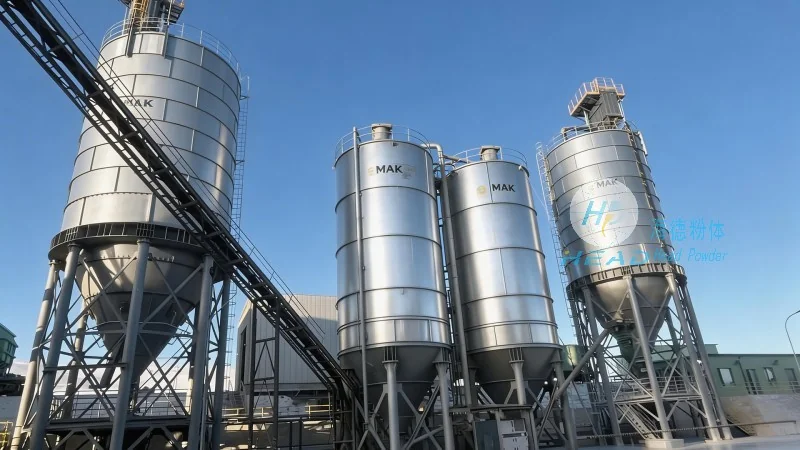
Dry coffee material conveying systems are widely employed across various stages of coffee processing and distribution. In coffee roasting facilities, these systems are used to transport raw coffee beans from storage to the roasting machines and then to cooling and packaging areas. The systems help maintain consistent material flow, reducing downtime and improving overall production efficiency. During the grinding process, conveying systems transport ground coffee from the grinder to storage silos or packaging lines, ensuring that the product is handled gently to preserve its flavor and aroma. Additionally, in coffee blending operations, conveying systems facilitate the mixing of different coffee varieties or additives, allowing for precise control over the final product composition. The versatility of these systems also makes them suitable for use in coffee distribution centers, where they help move bulk coffee products from receiving areas to shipping and storage zones.
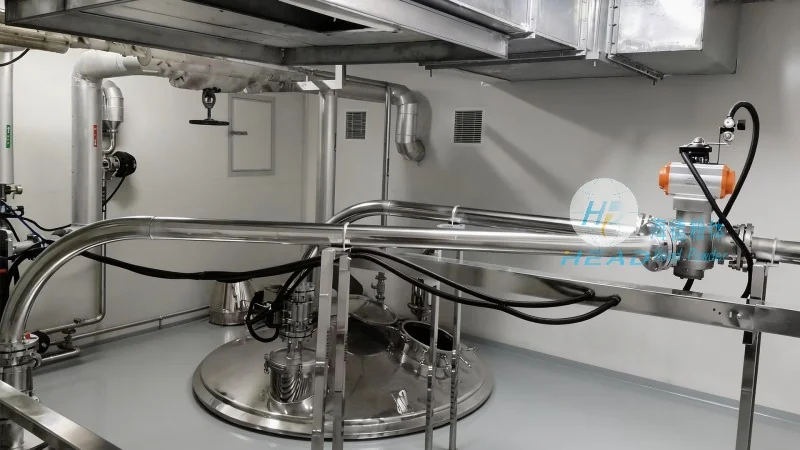
Implementing dry coffee material conveying systems offers numerous advantages for coffee processing businesses. One of the most significant benefits is the improvement in operational efficiency, as these systems can handle large volumes of material with minimal manual intervention. This reduces labor costs and increases production throughput. Additionally, the use of enclosed systems helps minimize dust and contamination, which is crucial for maintaining product quality and compliance with food safety regulations. The systems also contribute to better product consistency by ensuring uniform material handling and reducing the risk of human error. Furthermore, modern conveying systems are designed to be energy-efficient, which helps lower operational costs and reduce the environmental impact of coffee processing operations.
HeadPowder's dry coffee material conveying systems represent a sophisticated solution for the efficient and reliable transport of coffee materials. By understanding the principles and application scenarios outlined in this article, coffee processing companies can make informed decisions about implementing these systems to enhance their operations. With a focus on quality, efficiency, and innovation, HeadPowder continues to provide tailored solutions that meet the unique needs of the coffee industry.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top