In the pharmaceutical manufacturing sector, efficient and reliable material handling systems are crucial for ensuring product quality, compliance with regulatory standards, and overall operational efficiency. These systems are designed to manage the movement of raw materials, intermediate products, and finished goods throughout the production process, from receiving to packaging. The design and implementation of such systems require careful consideration of factors like sterility, contamination control, and adherence to Good Manufacturing Practices (GMP).
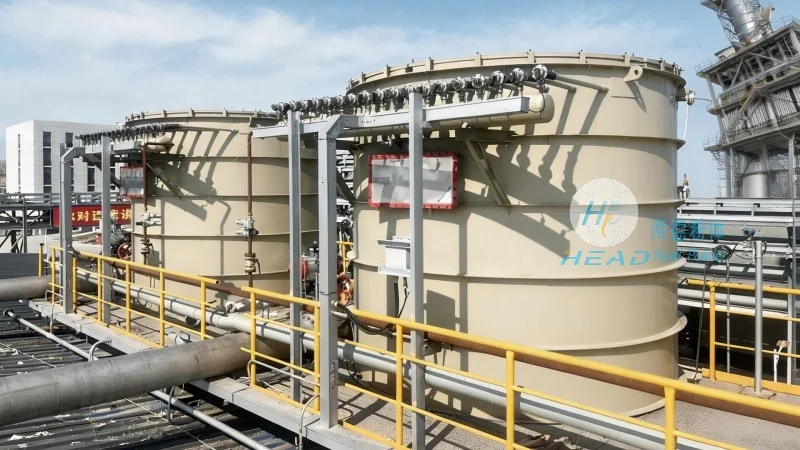
The fundamental principles of pharmaceutical material handling systems revolve around precision, safety, and compliance. One of the primary principles is the maintenance of a sterile environment, which is achieved through the use of cleanroom technology, air filtration systems, and sealed conveyor mechanisms. Another critical principle is the prevention of cross-contamination, which is ensured by implementing segregation of materials, use of dedicated transport routes, and regular cleaning protocols. Additionally, these systems must adhere to GMP guidelines, which dictate the design, construction, and operation of equipment to minimize the risk of product adulteration.
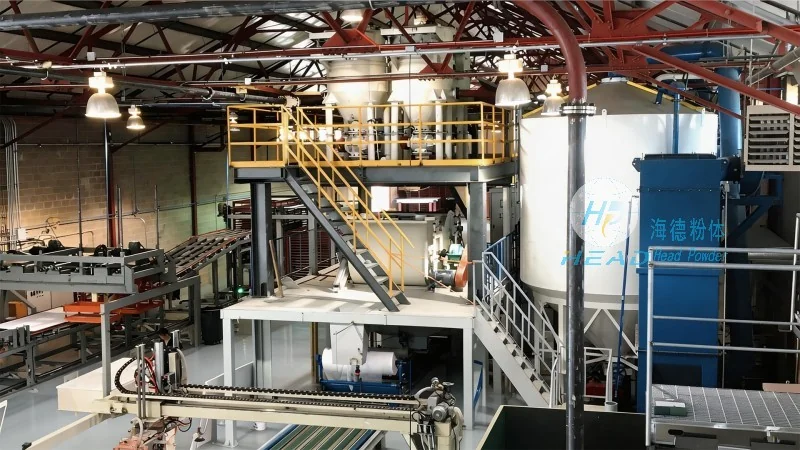
Pharmaceutical material handling systems operate in diverse scenarios tailored to specific manufacturing processes. For instance, in solid dosage form production, systems may include automated conveying of raw powders, blending equipment, and packaging lines. In liquid or semi-solid product manufacturing, systems might involve tank transport, filling machines, and capping units. Another common scenario is in the handling of sterile products, where systems are equipped with aseptic transfer mechanisms, such as sterile transfer hoods and closed-loop transport systems. These scenarios highlight the adaptability of material handling solutions to meet the unique demands of different pharmaceutical products and production stages.
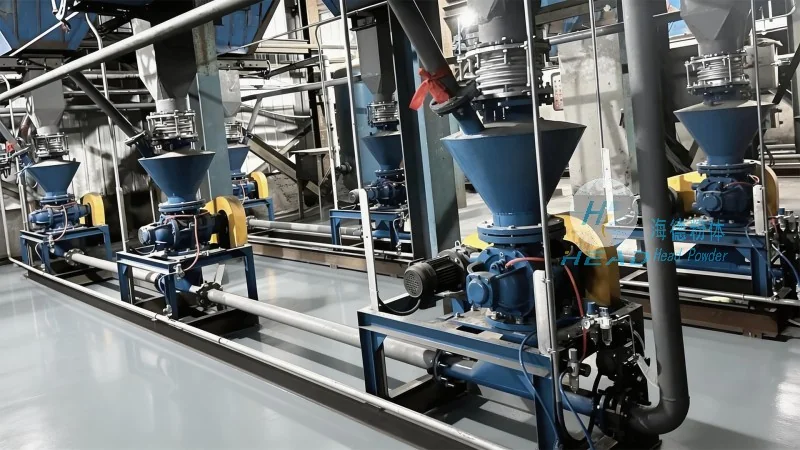
Headpowder, a leading provider in the pharmaceutical engineering sector, specializes in the design, manufacturing, and integration of advanced material handling systems. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for pharmaceutical manufacturers worldwide. Headpowder's expertise lies in developing customized solutions that align with clients' specific needs, ensuring optimal performance and compliance with industry standards.
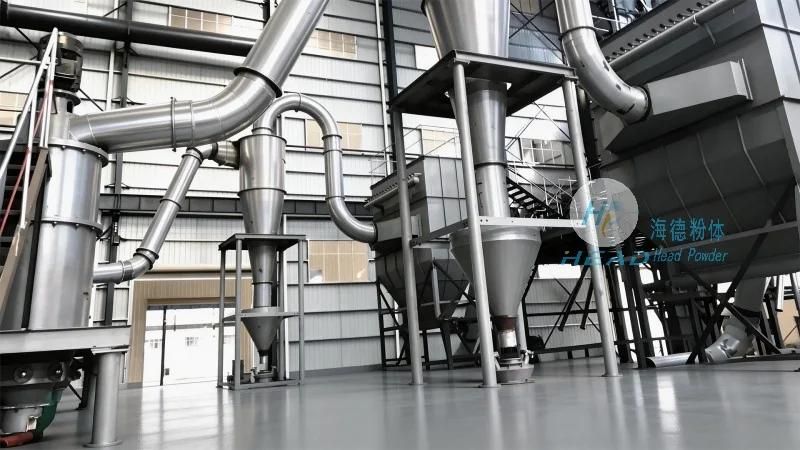
Headpowder is headquartered in Shandong, China, with a dedicated team of engineers and technicians focused on delivering high-quality material handling solutions. The company's location in China provides access to a robust supply chain and skilled workforce, enabling efficient project execution and timely delivery of systems.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top