Heptahydrate magnesium sulfate, commonly known as Epsom salt, is a widely used chemical compound in various industrial applications. The efficient and reliable transportation of this powder is crucial for maintaining production efficiency and product quality. This article introduces the principle and working characteristics of the heptahydrate magnesium sulfate powder conveying system equipment, highlighting its design and application in industrial settings.
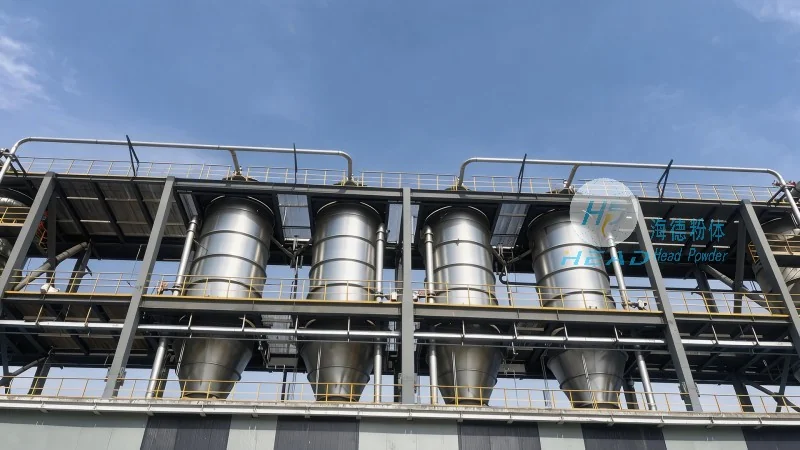
HeadPowder, a leading manufacturer in the field of powder handling and conveying systems, specializes in providing customized solutions for various industrial needs. With a strong commitment to quality and innovation, the company has established itself as a trusted partner for businesses requiring advanced powder processing equipment. HeadPowder's expertise lies in designing and manufacturing systems that ensure safe, efficient, and cost-effective powder transportation, particularly for sensitive materials like heptahydrate magnesium sulfate.
The heptahydrate magnesium sulfate powder conveying system operates based on principles of pneumatic or mechanical conveying, depending on the specific requirements of the application. Pneumatic conveying systems utilize air or other gases to transport the powder through a network of pipes, while mechanical systems rely on screw conveyors, belt conveyors, or other mechanical components to move the material. The choice of system depends on factors such as the particle size, moisture content, and the distance over which the powder needs to be transported. For heptahydrate magnesium sulfate, which is a fine powder with moderate flowability, a combination of pneumatic and mechanical components is often employed to achieve optimal conveying performance.
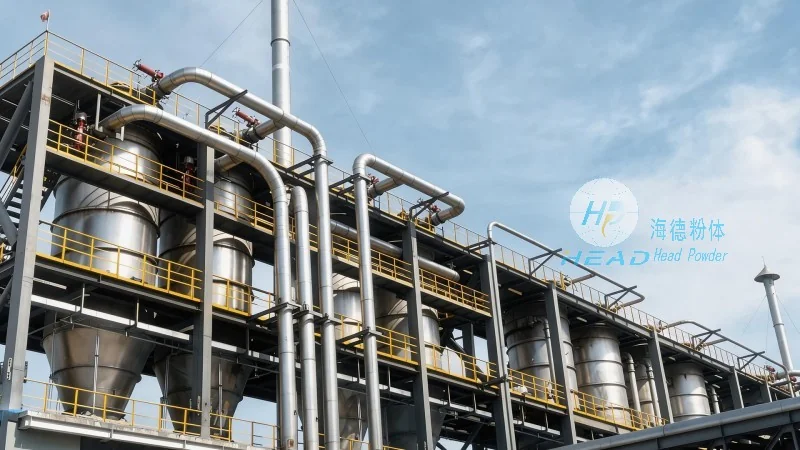
The working scene characteristics of the heptahydrate magnesium sulfate powder conveying system are tailored to meet the demands of industrial environments. These systems are designed to handle the specific properties of the powder, including its hygroscopic nature and potential for dust generation. The equipment is constructed with materials that are resistant to corrosion and wear, ensuring long-term durability and reliability. In industrial settings, such as chemical plants, pharmaceutical facilities, or food processing plants, the conveying system integrates seamlessly with other processing equipment, allowing for smooth material flow from storage to processing units. The system's design also considers safety aspects, including dust suppression measures and explosion-proof features, to comply with industrial safety regulations. The working scene typically involves continuous operation, with the system capable of handling varying production volumes and maintaining consistent material quality throughout the process.
The heptahydrate magnesium sulfate powder conveying system offered by HeadPowder features several key advantages that enhance its performance and usability. These include high conveying efficiency, low maintenance requirements, and the ability to handle a wide range of particle sizes and moisture levels. The system is equipped with advanced control mechanisms that allow for precise regulation of the conveying process, ensuring consistent material flow and preventing issues such as blockages or overloading. Additionally, the system is designed for easy integration with existing production lines, minimizing downtime during installation and operation. The use of high-quality components and rigorous quality control processes ensures that the system meets or exceeds industry standards, providing reliable performance in demanding industrial environments.
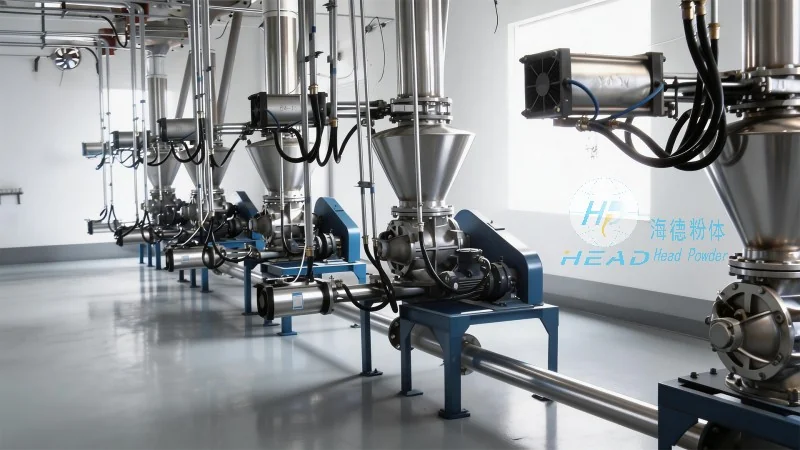
The heptahydrate magnesium sulfate powder conveying system is applicable in various industries where the compound is used as a raw material or intermediate. In the chemical industry, it is used in the production of other magnesium compounds, fertilizers, and pharmaceuticals. In the food industry, it serves as a food additive and dietary supplement. The system's versatility allows it to be adapted to different production scales, from small-scale laboratory applications to large-scale industrial production. The working scene characteristics, such as the ability to handle fine powders and maintain product purity, make it suitable for applications where product quality is critical. The system's design also supports easy cleaning and maintenance, which is essential for industries with strict hygiene requirements.
In conclusion, the heptahydrate magnesium sulfate powder conveying system is a critical component in the efficient processing of this important chemical compound. The system's design, based on advanced principles of powder handling, ensures reliable and safe transportation of the material. HeadPowder's expertise in manufacturing such systems has enabled the company to provide customized solutions that meet the specific needs of various industries. As industrial demands continue to evolve, the company remains committed to innovation and quality, ensuring that its conveying systems continue to deliver superior performance and reliability in the future.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top