HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of advanced powder conveying systems tailored for coal and sand applications. Our company, Shandong HeadPowder Engineering Co., Ltd., has established itself as a trusted provider of efficient and reliable equipment for handling fine particulate materials in industrial settings.
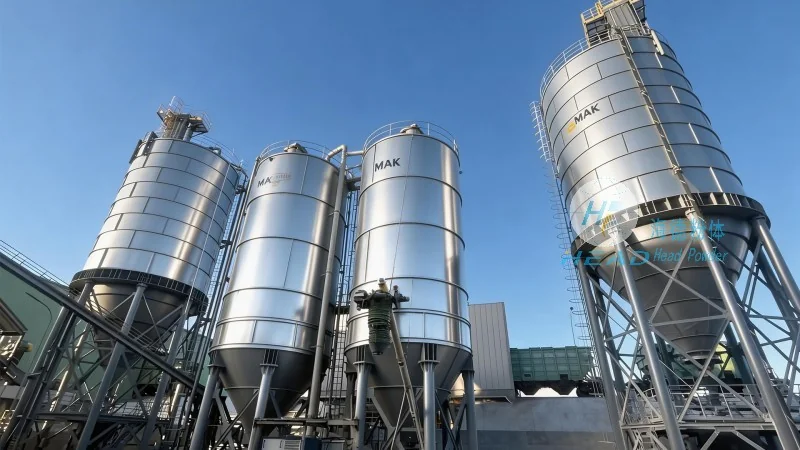
Coal sand powder conveying systems are critical components in various industrial processes where the transportation of fine powders like coal dust, sand, and other granular materials is required. These systems are engineered to ensure safe, efficient, and consistent material transfer from source to destination, minimizing dust generation and operational risks. The core of such systems lies in their ability to handle abrasive and potentially hazardous materials while maintaining high throughput and low maintenance costs.
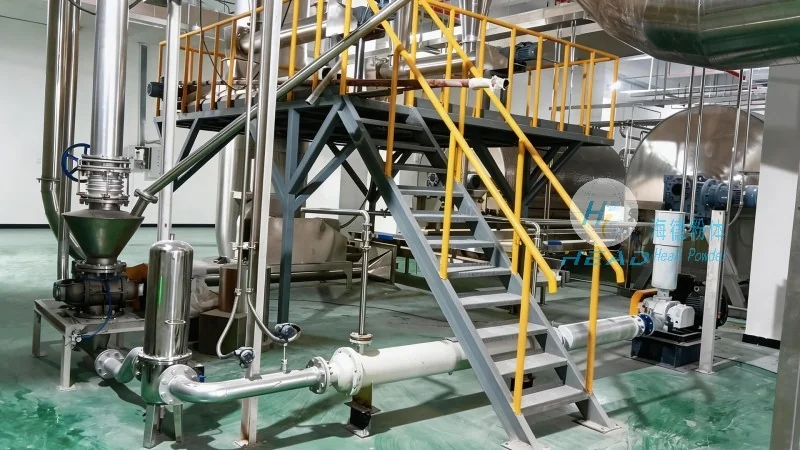
The fundamental principle behind coal sand powder conveying systems involves the use of air or mechanical forces to move particulate materials through a pipeline. In pneumatic conveying systems, for example, a blower or compressor generates a flow of air that propels the powder particles forward. The system typically includes a hopper for material storage, a feeding mechanism to control the flow rate, a conveying line, and a receiver to deposit the material at the destination. Mechanical conveying systems, on the other hand, utilize rotating components like screws or belts to transport the material. Both approaches are designed to optimize the movement of fine powders, ensuring minimal degradation of the material and efficient energy utilization.
The working scene characteristics of coal sand powder conveying systems are tailored to meet the specific demands of industrial environments. These systems are often deployed in scenarios where material handling efficiency is paramount, such as in mining operations, power plants, and construction sites. The equipment is designed to operate under varying conditions, including different particle sizes, moisture levels, and ambient temperatures. For instance, in coal processing facilities, the conveying system must handle high volumes of coal dust while maintaining air quality standards. Similarly, in sand processing plants, the system ensures the smooth transfer of sand for concrete production or other construction applications. The adaptability of these systems to diverse operational conditions makes them indispensable in modern industrial workflows.
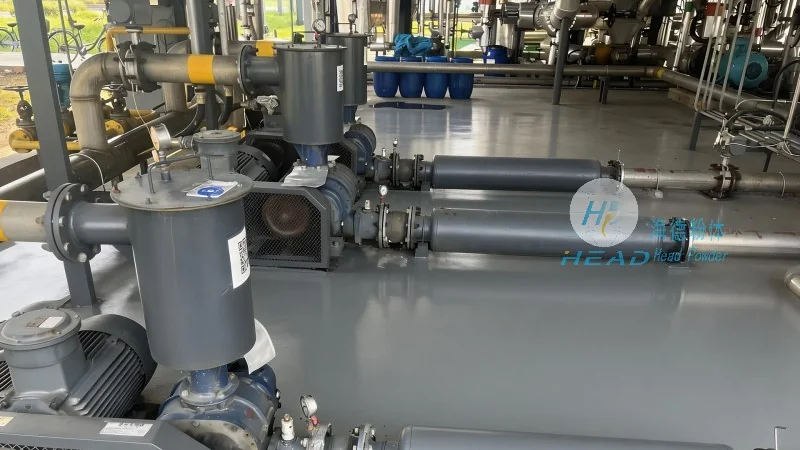
Coal sand powder conveying systems offer several advantages that make them suitable for a wide range of applications. Firstly, they provide a dust-free environment, which is crucial for maintaining workplace safety and compliance with environmental regulations. Secondly, these systems can handle high material throughput, reducing the need for manual labor and increasing overall productivity. Thirdly, the equipment is designed for low maintenance, with components that are resistant to wear and corrosion from abrasive materials. In practical applications, these systems are used in coal handling, sand processing, and other industries where fine particulate materials need to be transported over long distances or within complex layouts. The reliability and efficiency of HeadPowder's conveying systems have made them a preferred choice for companies seeking to optimize their material handling processes.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top