HeadPowder, a leading provider in the field of material handling solutions, specializes in the design, manufacturing, and implementation of advanced pneumatic conveying systems tailored for the handling of rare earth powders. This article delves into the fundamental principles underlying these systems and highlights the key working scene characteristics that define their effectiveness and reliability in industrial applications.
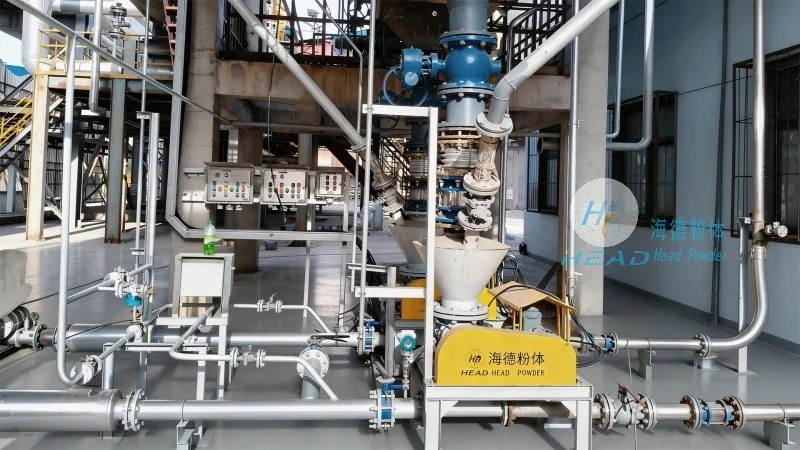
Pneumatic conveying systems operate by transporting bulk materials, such as rare earth powders, through a pipeline using a gas stream, typically air or other gases. The primary principle involves creating a pressure differential or using vacuum to move the material from the source to the destination. In the context of rare earth powders, which are often fine, abrasive, and potentially sensitive to moisture or contamination, the system design must address several critical factors to ensure efficient and safe operation. Key principles include the selection of appropriate air velocities, pipeline configurations, and material handling components that minimize particle degradation, prevent blockages, and maintain product integrity throughout the conveying process.
The working scene characteristics of these systems are shaped by the unique properties of rare earth powders and the specific requirements of industrial environments. These characteristics include:
1. **Material Handling Efficiency**: The systems are engineered to handle rare earth powders with high efficiency, ensuring consistent flow rates and minimal downtime. This is achieved through optimized air flow management and robust pipeline designs that accommodate the fine particle size and potential for agglomeration.
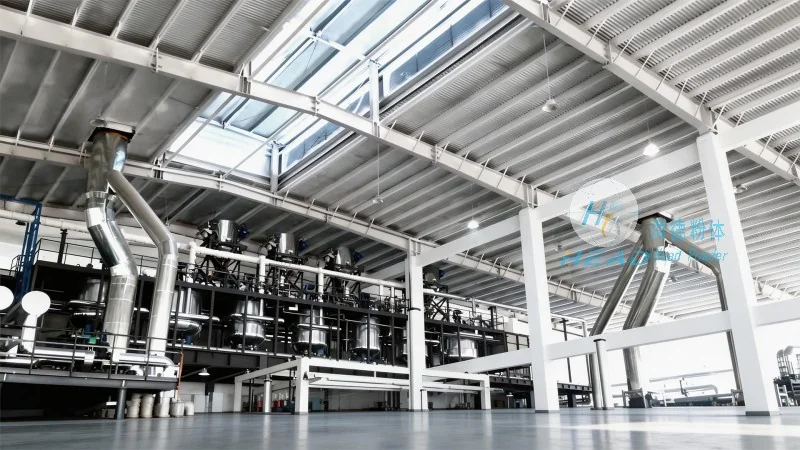
2. **Process Integration and Flexibility**: Rare earth powder pneumatic conveying systems are designed for seamless integration into existing production lines. They offer flexibility in conveying distances, from short-distance transfers to long-distance applications, and can be adapted to various production scenarios, including batch processing or continuous operation.
3. **Safety and Environmental Compliance**: Given the potential hazards associated with handling rare earth powders, such as dust explosions or contamination risks, the systems incorporate safety features like explosion-proof designs, dust collection systems, and enclosed conveying paths to ensure compliance with industrial safety standards and environmental regulations.
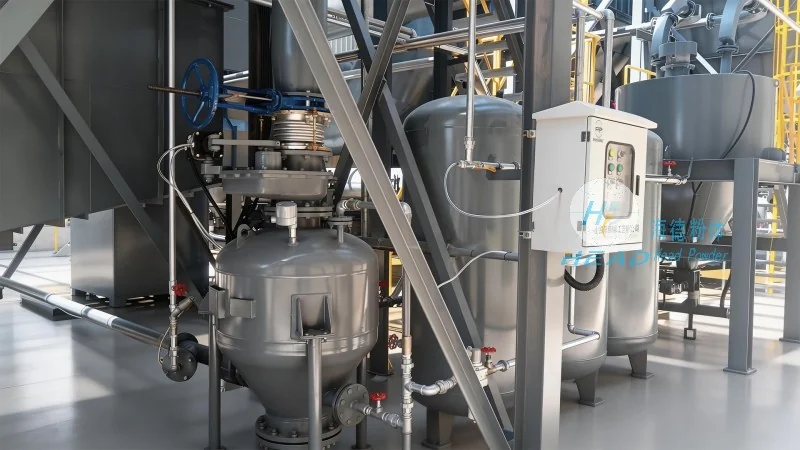
4. **Maintenance and Durability**: The equipment is constructed with durable materials, such as stainless steel or specialized alloys, to withstand the abrasive nature of rare earth powders and the operational stresses of continuous use. This ensures long-term reliability and reduces maintenance costs over the system's lifecycle.
Shandong HeadPowder Engineering Co., Ltd., based in Shandong, China, leverages decades of experience in material handling technology to deliver customized pneumatic conveying solutions for rare earth powder applications. The company's approach involves a thorough understanding of the client's specific operational needs, followed by the design and implementation of systems that meet both functional and safety requirements. By focusing on the unique characteristics of rare earth powders and the demands of industrial environments, HeadPowder ensures that its systems provide reliable, efficient, and cost-effective material transport solutions.
In summary, rare earth powder pneumatic conveying systems represent a sophisticated solution for the efficient and safe handling of rare earth materials. The principles of pneumatic transport, combined with specialized design considerations for rare earth powders, result in systems that enhance productivity, ensure product quality, and comply with industrial standards. HeadPowder, with its expertise and commitment to quality, continues to provide innovative solutions that meet the evolving needs of industries relying on rare earth powders.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top