For industrial applications requiring precise material handling, metering bin pump pneumatic conveying lines offer a reliable and efficient solution. This article explores the fundamental principles behind these systems and highlights key characteristics of their operational scenarios, providing insights into how they enhance material transport processes in various industrial settings.
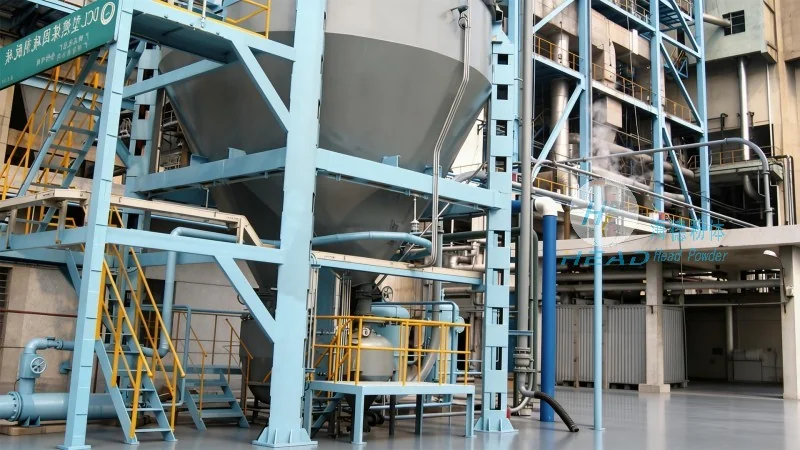
The metering bin pump, as a critical component of pneumatic conveying systems, operates on the principle of creating a controlled pressure differential to move bulk materials through a pipeline. By utilizing a hopper or bin to store the material and a pump to generate the necessary air flow, the system ensures consistent and accurate material discharge. The pump typically works by drawing air from the system, mixing it with the material, and then propelling the mixture through the conveying line under pressure. This method allows for the transport of dry powders and granules over long distances with minimal product degradation, making it suitable for a wide range of industrial applications.
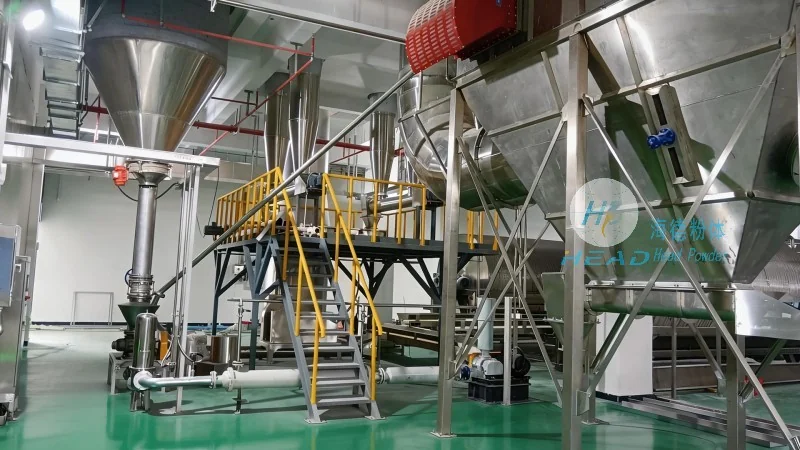
The operational characteristics of metering bin pump pneumatic conveying lines are defined by several factors that influence their performance and suitability for specific applications. These include the type of material being conveyed, the distance and elevation changes required, and the desired flow rate and accuracy. For example, in industries such as cement, chemical, and food processing, where precise dosage and contamination control are paramount, these systems excel. The ability to maintain a consistent pressure and flow rate ensures that the material is transported without segregation or clumping, which is crucial for maintaining product quality. Additionally, the system's flexibility allows for integration with other processing equipment, such as mixers, classifiers, and storage silos, enabling seamless material handling workflows.
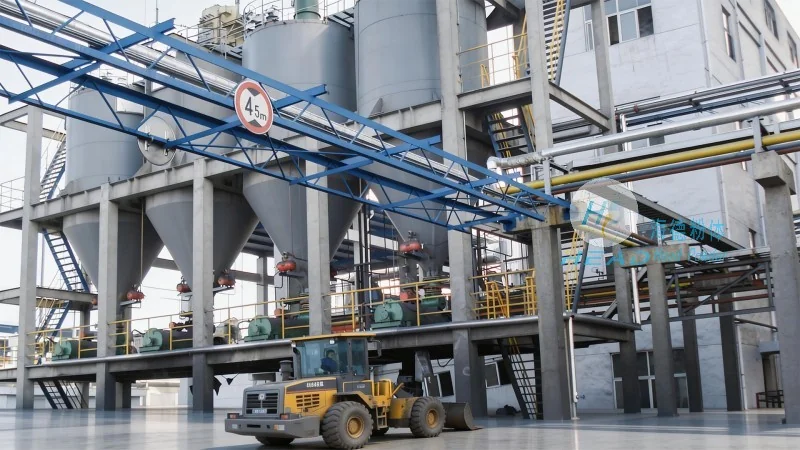
Real-world applications of metering bin pump pneumatic conveying lines vary across different industries, each leveraging the system's unique advantages. In the cement industry, for instance, these systems are used to transport raw materials and finished products from storage silos to production lines, ensuring a steady supply of materials for cement manufacturing. The chemical industry benefits from the system's ability to handle abrasive and corrosive materials without damaging the equipment, as the pump and pipeline are designed to withstand the harsh conditions. Similarly, in the food processing sector, where hygiene and product purity are critical, the system's enclosed design prevents contamination and maintains the integrity of the product. The consistent flow rate and precise metering capabilities also contribute to improved production efficiency and reduced waste, as materials are delivered exactly as needed without over or under-dosing.
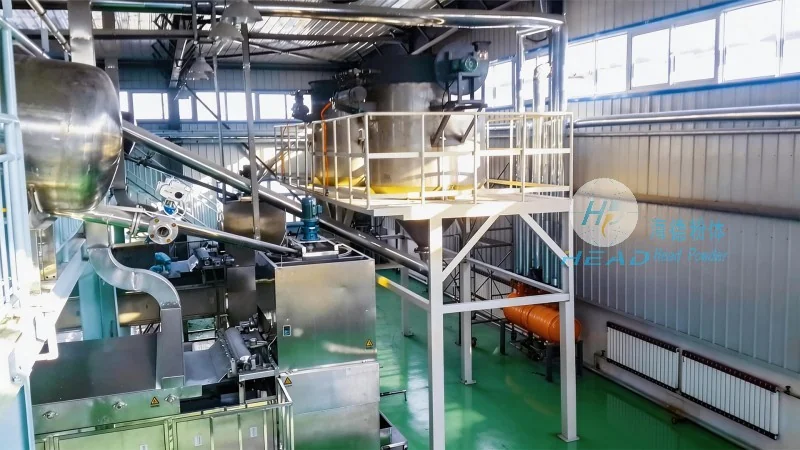
HeadPowder, a leading manufacturer of industrial material handling equipment, specializes in the design, development, and production of metering bin pump pneumatic conveying systems. With a strong presence in China, particularly in Shandong province, the company has built a reputation for delivering high-quality, reliable solutions tailored to the diverse needs of industrial clients. The company's commitment to innovation and customer satisfaction is reflected in its state-of-the-art manufacturing facilities and rigorous quality control processes. By leveraging advanced engineering and manufacturing technologies, HeadPowder ensures that its products meet the highest industry standards, providing customers with durable and efficient solutions for their material handling challenges.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top