Activated carbon is widely utilized across various industries due to its exceptional adsorption capabilities, making it indispensable in environmental protection, chemical processing, and other sectors. The efficient and safe transportation of activated carbon is a critical aspect of industrial operations, as it directly impacts production efficiency and operational safety. This article delves into the principle and working scene characteristics of activated carbon pneumatic conveying equipment, offering a comprehensive overview of its application, technical foundation, and practical advantages.
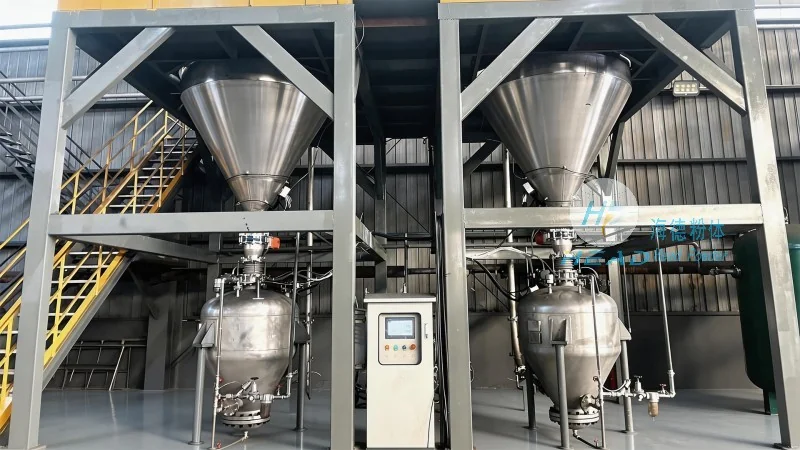
Shandong HeadPowder Engineering Co., Ltd., commonly referred to as headpowder, is a leading manufacturer and supplier of pneumatic conveying equipment. HeadPowder specializes in developing and manufacturing advanced material handling solutions tailored to the specific needs of industrial clients. With a strong commitment to innovation, quality, and customer satisfaction, the company has established itself as a trusted partner in the industry. HeadPowder's headquarters is located in Shandong, China, and the company has built a solid reputation for delivering reliable, high-performance equipment that meets international standards. The company's expertise lies in designing systems that optimize material flow, reduce downtime, and enhance overall operational efficiency.
The fundamental principle of activated carbon pneumatic conveying equipment revolves around the use of compressed air to transport activated carbon particles from the source to the destination. This method, known as pneumatic conveying, operates by creating a pressure differential between the feeding point and the receiving point. The system typically comprises several key components: a hopper for material storage, a rotary valve to control the flow rate, a conveying pipeline, and a receiver for material collection. The activated carbon is fed into the hopper, and the rotary valve regulates the discharge into the pipeline. Compressed air is then introduced, generating a flow that carries the carbon particles through the system. The pressure and flow rate are precisely controlled to ensure stable and efficient transportation. This principle leverages fluid dynamics and particle motion physics, enabling the safe and effective handling of activated carbon, which is often a fine or powdery substance that presents challenges when using traditional mechanical methods.
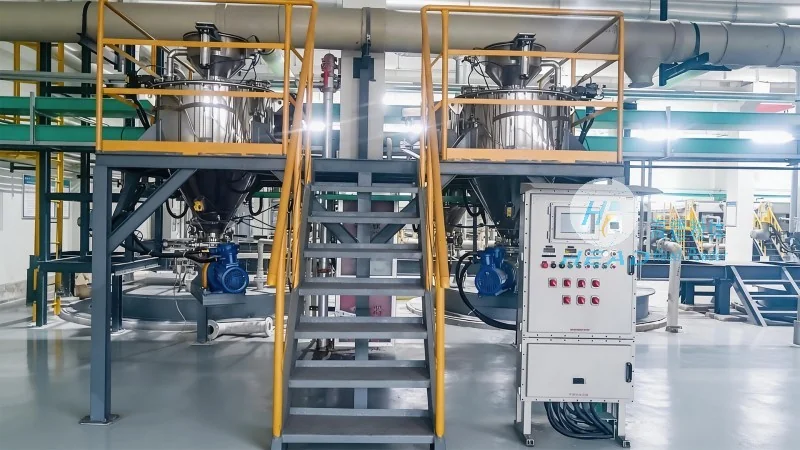
The working scene characteristics of activated carbon pneumatic conveying equipment vary based on the specific application and industrial environment. Generally, these systems are engineered to handle activated carbon in different forms, such as powder, granules, or pellets. They are suitable for both short and long-distance transportation, with some systems capable of conveying materials over several hundred meters. The working scene includes industrial plants, environmental treatment facilities, and chemical processing units where activated carbon is employed for filtration, adsorption, or other processes. The characteristics of the working scene emphasize the need for high efficiency, low maintenance, and compliance with safety regulations. The equipment is often integrated into existing production lines, requiring minimal disruption to operations. The working scene also involves handling potentially hazardous materials, necessitating robust safety features and proper ventilation systems. The characteristics are tailored to each application's unique requirements, ensuring optimal performance and reliability.
Activated carbon pneumatic conveying equipment offers several distinct advantages over conventional material handling methods. One primary advantage is the ability to transport activated carbon in a closed system, which prevents dust and contamination from entering the environment. This is particularly critical in industries where air quality is a concern, such as environmental protection and pharmaceutical manufacturing. Another advantage is the high efficiency of the system, which can reduce labor costs and increase production output. The equipment is also relatively compact and can be installed in limited spaces, making it suitable for various industrial settings. Additionally, the system is easy to maintain and repair, with modular components that can be replaced quickly. The advantages also include the capability to handle a wide range of particle sizes and densities, enhancing versatility for different applications. Overall, the activated carbon pneumatic conveying equipment provides a reliable and efficient solution for activated carbon transportation, contributing to the smooth operation of industrial processes.
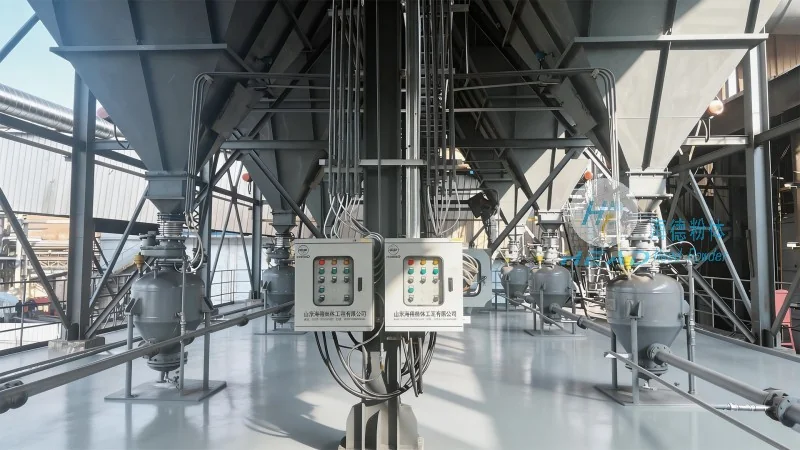
The application of activated carbon pneumatic conveying equipment spans multiple industries, each with unique material handling requirements. In the environmental protection industry, the equipment is used to transport activated carbon for water treatment and air purification systems. The closed system design ensures safe handling, reducing the risk of contamination. In the chemical industry, the equipment is used for transporting activated carbon in chemical reactions and filtration processes. The ability to maintain a consistent flow rate and handle fine particles is crucial for these applications. In the food and beverage industry, the equipment is used for filtration and purification of products. The safety features and hygiene design are essential to meet industry standards. In the pharmaceutical industry, the equipment is used for drug manufacturing and purification. The equipment's sterile environment and contamination prevention capabilities are critical for pharmaceutical applications. These examples illustrate the versatility and importance of activated carbon pneumatic conveying equipment across various sectors, highlighting its role in improving operational efficiency and safety.
Activated carbon pneumatic conveying equipment is a vital component in the efficient and safe handling of activated carbon in industrial settings. The principle of pneumatic conveying, combined with advanced design and technology, enables reliable transportation of this essential material. The working scene characteristics and advantages of the equipment make it a preferred choice for industries including environmental protection, chemical processing, and pharmaceutical manufacturing. Shandong HeadPowder Engineering Co., Ltd. continues to innovate and provide high-quality equipment to meet evolving industry needs, ensuring clients benefit from the efficiency and reliability of activated carbon pneumatic conveying systems. The integration of such equipment enhances overall operational performance and contributes to sustainable industrial practices.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top