When it comes to transporting dolomite, selecting the right method is crucial for efficiency and cost-effectiveness in industrial operations. Dolomite, a sedimentary rock composed primarily of calcium magnesium carbonate, is widely used in various industries such as construction, steel production, and chemical manufacturing. The choice of conveying method depends on factors like material characteristics, distance, volume, and the specific requirements of the application. This article explores several common dolomite conveying methods, highlighting their advantages and typical applications. HeadPowder, a leading provider of material handling solutions, specializes in designing and manufacturing equipment tailored to the unique needs of dolomite processing. With decades of experience in the industry, HeadPowder offers a range of conveying systems that ensure reliable and efficient transport of dolomite from extraction to processing.
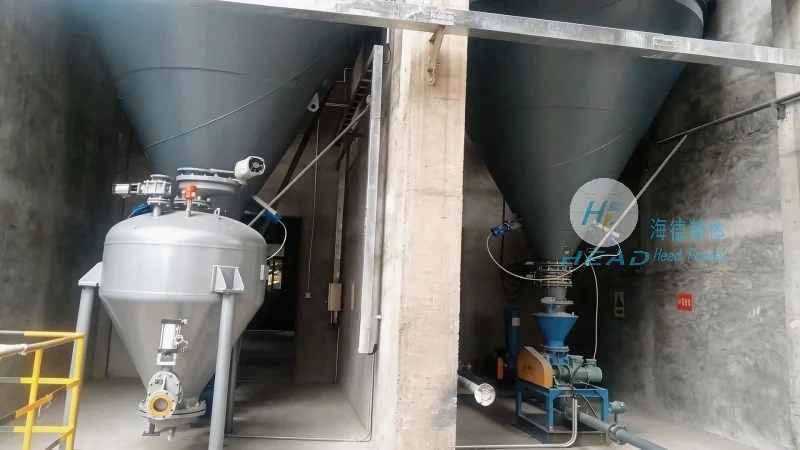
Belt conveyors are one of the most widely used methods for dolomite transportation due to their versatility and reliability. These systems consist of a continuous loop of belt that moves material from the loading point to the discharge point. The belt is supported by rollers and driven by a motor, allowing for smooth and consistent movement of dolomite particles. For dolomite, which can range from fine powders to larger lumps, belt conveyors can be equipped with special materials like rubber or PVC to prevent wear and ensure durability. The design of the belt conveyor can be customized to handle different particle sizes and moisture content, making it suitable for both bulk and fine dolomite. One of the key advantages of belt conveyors is their ability to operate continuously over long distances with minimal maintenance. They are particularly effective in open-pit mining and quarry operations where dolomite is extracted and then transported to processing facilities. The system can be integrated with other equipment, such as crushers and screens, to form a complete material handling line. Belt conveyors also offer a cost-effective solution for transporting large volumes of dolomite, as they require less energy compared to other methods like pneumatic systems. However, they may not be suitable for very fine powders, as the belt can cause dust issues and require additional dust control measures.
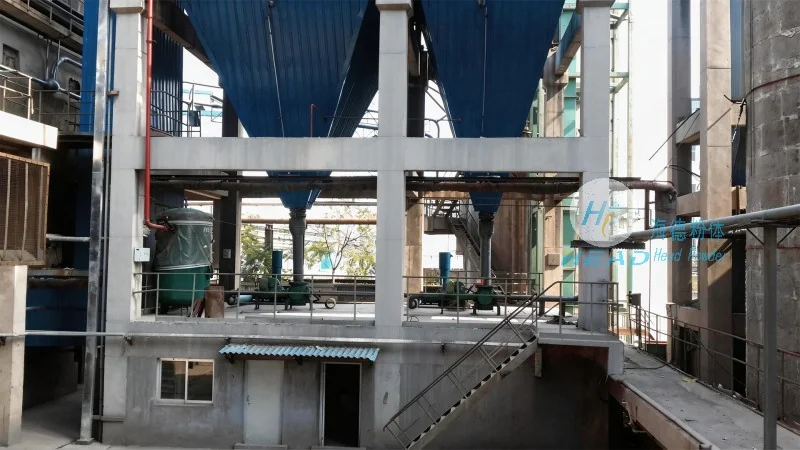
For vertical or inclined transport of dolomite, bucket elevators are an excellent choice. These systems use a series of buckets attached to a belt or chain that moves vertically or at an angle. The buckets scoop up dolomite from a hopper at the bottom and carry it to the top, where the material is discharged. Bucket elevators are particularly effective for transporting dolomite in vertical shafts or over long vertical distances, such as in processing plants where the material needs to be lifted from a storage silo to a higher level for further processing. The design of the bucket elevator can be adjusted to handle different particle sizes, with larger buckets for coarser dolomite and smaller buckets for finer powders. The speed and capacity of the elevator can be controlled to match the production requirements of the plant. One of the main advantages of bucket elevators is their ability to transport material vertically without the need for additional space, making them ideal for facilities with limited horizontal space. They are also relatively low maintenance, as the moving parts are enclosed and protected from dust and debris. However, bucket elevators may have higher initial costs compared to belt conveyors and can be more complex to install. They also require regular inspection to ensure the buckets are in good condition and the chain or belt is properly tensioned to prevent breakdowns.
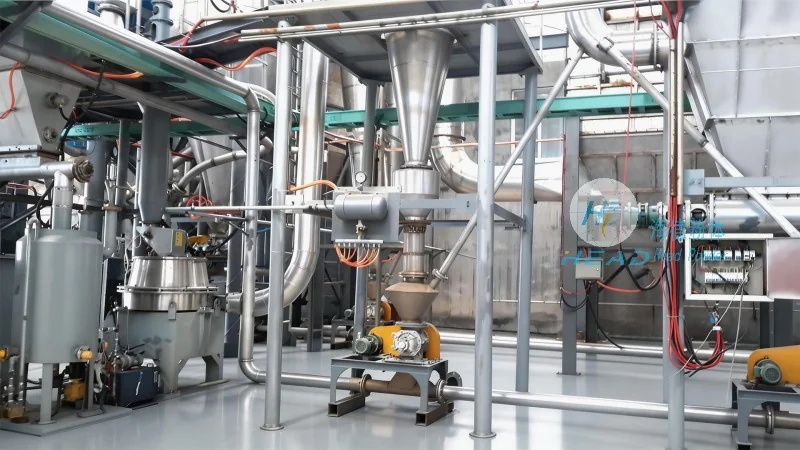
Pneumatic conveying systems use air or other gases to transport dolomite particles through a pipeline. This method is particularly suitable for fine dolomite powders or dust, as it can move material over long distances without the need for mechanical components at the end points. The system typically consists of a blower or compressor that generates air pressure, a hopper to feed the dolomite, and a pipeline network that carries the material to the discharge point. The dolomite is suspended in the air stream and carried through the pipeline, where it is then collected in a receiver at the end. Pneumatic conveying systems can be either positive pressure or negative pressure, depending on the application. Positive pressure systems blow air into the pipeline, pushing the material forward, while negative pressure systems create a vacuum to draw the material into the pipeline. For dolomite, which can be abrasive, the pipeline material is often made of stainless steel or other corrosion-resistant materials to prevent wear and ensure longevity. One of the key advantages of pneumatic conveying is its ability to transport material in a closed system, which helps to control dust and maintain a clean environment. This is particularly important in industries where dust control is a regulatory requirement. Pneumatic systems can also handle varying particle sizes and moisture content, making them versatile for different dolomite applications. However, they may require higher energy consumption compared to other methods, especially for long-distance or high-volume transport. The system also needs to be properly designed to prevent blockages and ensure consistent flow, as dolomite particles can be sticky or clump together, leading to system inefficiencies.
Screw conveyors, also known as auger conveyors, are another common method for dolomite transportation. These systems use a rotating screw or auger to move material along a trough. The screw is typically made of metal and is designed to handle different particle sizes and moisture content. The material is fed into the trough at one end and is pushed forward by the rotating screw to the discharge point at the other end. Screw conveyors are particularly effective for transporting dolomite in horizontal or slightly inclined directions, such as from a storage bin to a processing machine. They are often used in applications where the material needs to be mixed or blended, as the screw can provide gentle agitation. One of the main advantages of screw conveyors is their simplicity and low maintenance. The system consists of a single rotating part, which reduces the number of components that can fail, making it reliable for continuous operation. Screw conveyors are also relatively inexpensive compared to other methods like belt or pneumatic systems. However, they may not be suitable for very large or heavy dolomite lumps, as the screw can cause wear and tear on the trough and the screw itself. They are also less effective for long-distance transport, as the material may experience friction and wear over time. Screw conveyors are commonly used in small to medium-scale operations where the volume of dolomite is moderate and the distance is short.
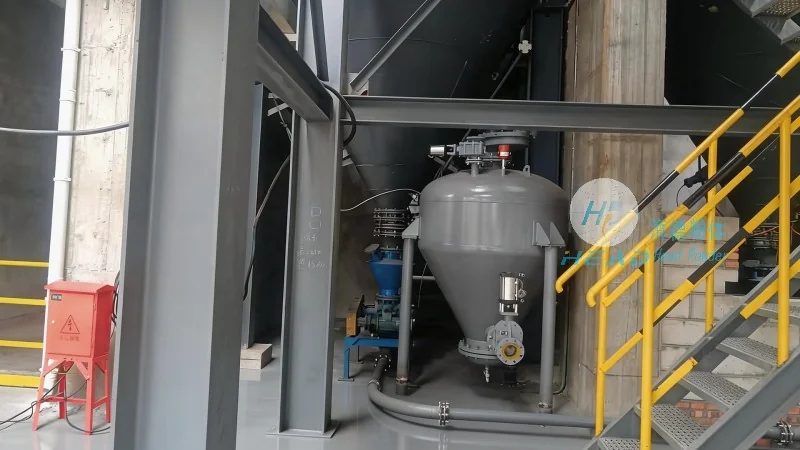
Vibrating conveyors use vibration to move dolomite along a trough. The system consists of a conveyor bed that is supported by springs and driven by an electric motor, which causes the bed to vibrate at a specific frequency. The vibration helps to move the dolomite particles forward, even when the material is dry or has a low angle of repose. Vibrating conveyors are particularly effective for transporting dolomite in horizontal or slightly inclined directions, and they can handle a wide range of particle sizes and moisture content. The design of the conveyor can be adjusted to control the speed and direction of the material flow, making it suitable for different applications. One of the key advantages of vibrating conveyors is their ability to handle sticky or cohesive dolomite without the need for additional equipment like feeders or crushers. The vibration helps to break up clumps and ensure consistent movement of the material. They are also relatively low maintenance, as there are no moving parts that come into direct contact with the material, reducing wear and tear. Vibrating conveyors are commonly used in industries where the material needs to be transported at a controlled speed, such as in food processing or pharmaceutical manufacturing. However, they may not be suitable for very fine powders, as the vibration can cause dust to become airborne and require additional dust control measures. The system also needs to be properly balanced to prevent excessive vibration and noise, which can affect the surrounding environment.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top