HeadPowder, a leading provider in the field, specializes in the design and implementation of pneumatic conveying systems tailored for the food additive industry. These systems are engineered to meet stringent safety and hygiene standards, ensuring the integrity of sensitive ingredients while optimizing operational efficiency. By leveraging advanced technology and industry expertise, HeadPowder delivers solutions that enhance productivity and maintain product quality throughout the material handling process.
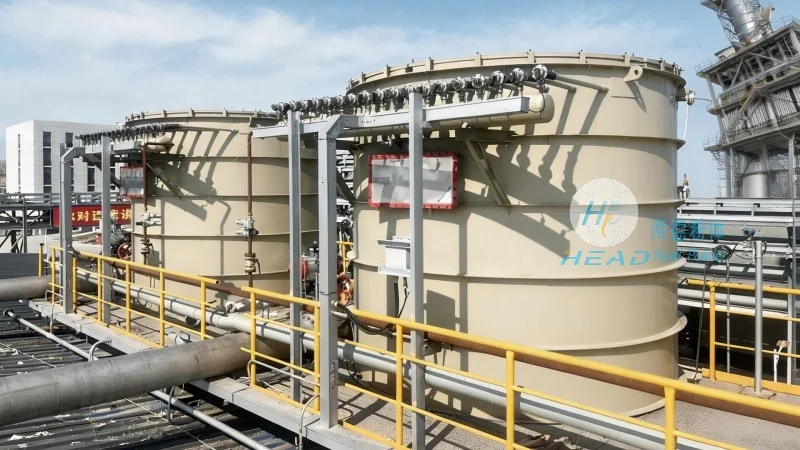
Pneumatic conveying systems operate by transporting bulk materials through a pipeline using a stream of air or other gas. The process involves creating a pressure differential between the inlet and outlet of the system, which propels the material forward. There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems utilize compressed air to push material, while vacuum systems employ a vacuum to pull material. For food additives, vacuum systems are often preferred due to their gentler handling, which minimizes product degradation and maintains quality. This is critical for ingredients that are sensitive to mechanical stress or temperature changes, ensuring that their functional properties remain intact.
The pneumatic conveying systems offered by Shandong HeadPowder Engineering Co., Ltd. are designed with several distinct advantages that make them ideal for various food additive handling scenarios. One of the most significant benefits is the ability to transport materials in a closed system, which prevents contamination from external sources and maintains product purity. This is particularly crucial for food additives, where cross-contamination can lead to regulatory issues and product recalls. The closed-loop design also reduces dust emissions, improving workplace safety and environmental compliance.
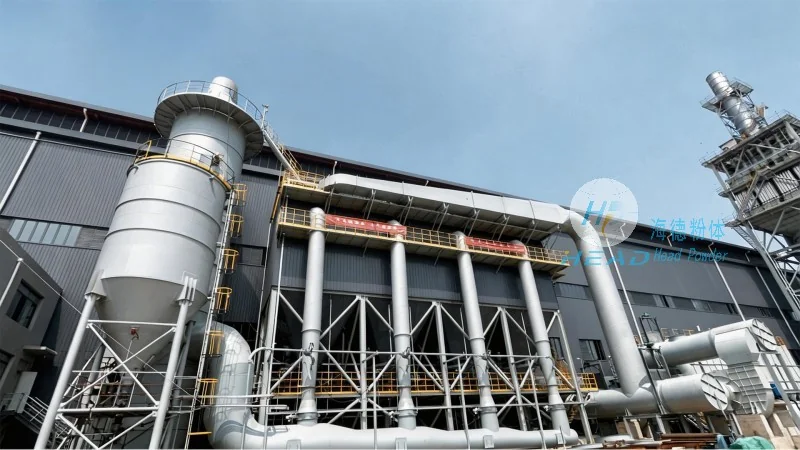
Another key feature is the system's flexibility in handling different material types. Whether dealing with powders, granules, or fine particles, the equipment can be customized to accommodate varying particle sizes and flow characteristics. This adaptability allows for seamless integration into existing production lines, reducing downtime and increasing overall productivity. For instance, in a manufacturing facility producing food colorings or flavor enhancers, the system can efficiently convey raw materials from storage silos to processing equipment without manual intervention.
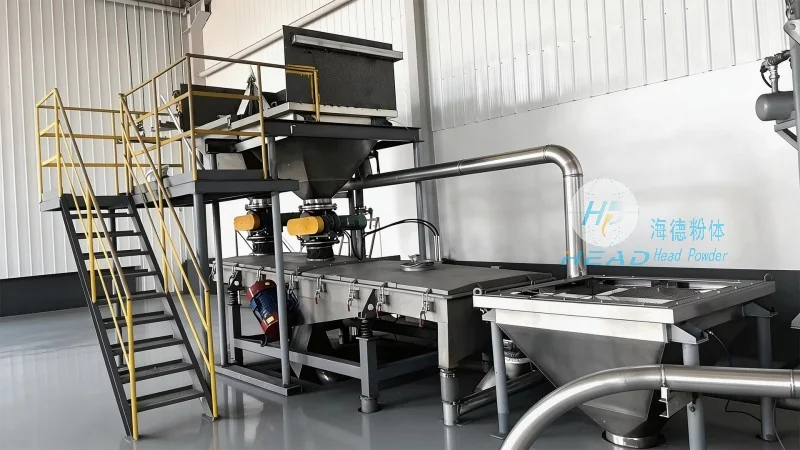
Furthermore, the systems are engineered for low maintenance and high reliability. Advanced materials and robust construction ensure long service life, minimizing operational disruptions and maintenance costs. The use of stainless steel components and hygienic design principles aligns with industry standards, such as FDA and GMP, ensuring compliance with regulatory requirements. This not only enhances product safety but also streamlines quality control processes, giving manufacturers confidence in their output.
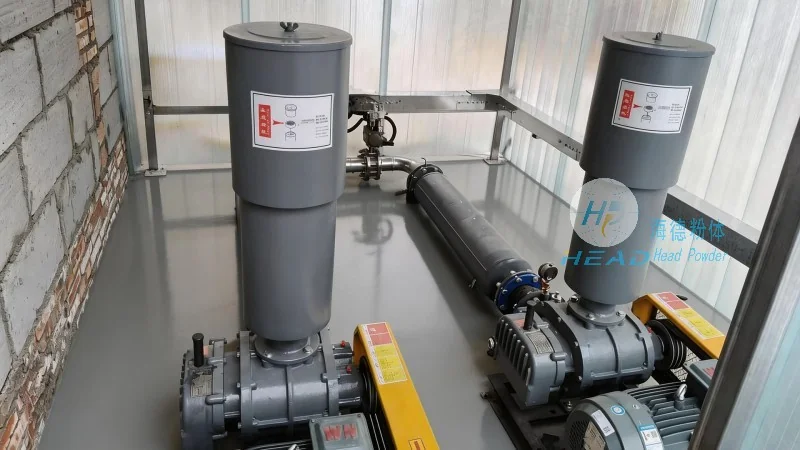
Implementing a pneumatic conveying system from HeadPowder brings numerous benefits to food additive manufacturers. Firstly, it enhances operational efficiency by automating material transport, reducing labor costs and increasing throughput. Secondly, it improves product quality by minimizing exposure to contaminants and handling stress. Thirdly, it ensures regulatory compliance, which is essential for maintaining market access and customer trust. These advantages collectively contribute to a competitive edge in the industry, allowing companies to meet growing demand while upholding the highest standards of safety and quality.
HeadPowder, based in Shandong, China, is dedicated to providing innovative solutions for material handling in the food and pharmaceutical sectors. With years of experience in the industry, the company has developed a deep understanding of the unique challenges faced by food additive manufacturers. By combining technical expertise with customer-centric approaches, HeadPowder delivers systems that not only meet but exceed industry expectations. The company's commitment to research and development ensures that its products remain at the forefront of technological advancements, offering sustainable and efficient solutions for the future of food additive processing.

 Shandong Headpowder Engineering Co., Ltd.
 156-6277-7102(Manager Zhang)
 0531-83386006
 Jinan, Shandong Province, China

telephone
WeChatconsult
top